کلینیک فوق تخصصی دانش آموخته  لوله کشی صنعتی  ۸۳-۸۴ ( نفت و گاز ) -  مایترکاری

کلینیک فوق تخصصی دانش آموخته لوله کشی صنعتی ۸۳-۸۴ ( نفت و گاز ) - مایترکاری

سایتی نو و نخست برای ارائه راهنمای ساخت انواع شابلون پایپینگ به Fabricator ها و بالا بردن دانش ریاضی ایشان
کلینیک فوق تخصصی دانش آموخته  لوله کشی صنعتی  ۸۳-۸۴ ( نفت و گاز ) -  مایترکاری

کلینیک فوق تخصصی دانش آموخته لوله کشی صنعتی ۸۳-۸۴ ( نفت و گاز ) - مایترکاری

سایتی نو و نخست برای ارائه راهنمای ساخت انواع شابلون پایپینگ به Fabricator ها و بالا بردن دانش ریاضی ایشان

روش آزمون و حد پذیرش برای خال جوش جوشکار ... برداشت از AWS D1.1 2020


6.24 Method of Testing and Acceptance Criteria for Tack Welder Qualification

A force shall be applied to the specimen as shown in Figure fi.23 until rupture occurs. The force may be applied by any convenient means. The surface of the weld and of the fracture shall be examined visually for defects.

6.24.1 Visual Acceptance Criteria. The tack weld shall present a reasonably uniform appearance and shall be free of overlap, cracks, and undercut exceeding 1/32 in [1 mm]. There shall be no porosity visible on the surface of the tack weld.

6.24.2 Destructive Testing Acceptance Criteria. The fractured surface of the tack weld shall show fusion to the root, but not necessarily beyond, and shall exhibit no incomplete fusion to the base metals or any inclusion or porosity larger than 3/32 in [2.5 mm] in greatest dimension.


روش های آزمون و حد پذیرش برای صلاحیت WPS ... برداشت از AWS D1.1 2020


6.10 Methods of Testing and Acceptance Criteria for WPS Qualification

The welded test assemblies shall have test specimens prepared by cutting the test plate , whichever is applicable. The test specimens shall be prepared for testing

Visual Inspection of Welds. The visual acceptance criteria for qualification of groove and fillet welds (excluding weld tabs) shall conform to the following requirements, as applicable:

6.10.1.1 Visual Inspection of Groove Welds. Groove welds shall meet the following requirements:

(1) Any crack shall be unacceptable, regardless of size.

(2) All craters shall be filled to the full cross section of the weld.

(3) Weld reinforcement shall not exceed 1/8 in [3 mm]. The weld profile shall conform to Figure 1.4 and shall have complete fusion.

(4) Undercut shall not exceed 1/32 in [1 mm].

(5) The weld root for CJP grooves shall be inspected, and shall not have any cracks, incomplete fusion, or inadequate joint penetration.

(6) For CJP grooves welded from one side without backing, root concavity or melt-through shall conform to the following:

(a) The maximum root concavity shall be 1/16 in [2 mm], provided the total weld thickness is equal to or greater than that of the base metal.

(b) The maximum melt-through shall be 1/8 in [3 mm].

6.10.1.2 Visual Inspection of Fillet Welds. Fillet welds shall meet the following requirements: (1) Any crack shall be unacceptable, regardless of size.

(2) All craters shall be filled to the full cross section of the weld.

(3) The fillet weld leg sizes shall not be less than the required leg sizes.

(4) The weld profile shall meet the requirements of Figure 1.4.

(5) Base metal undercut shall not exceed 1/32 in [1 mm].

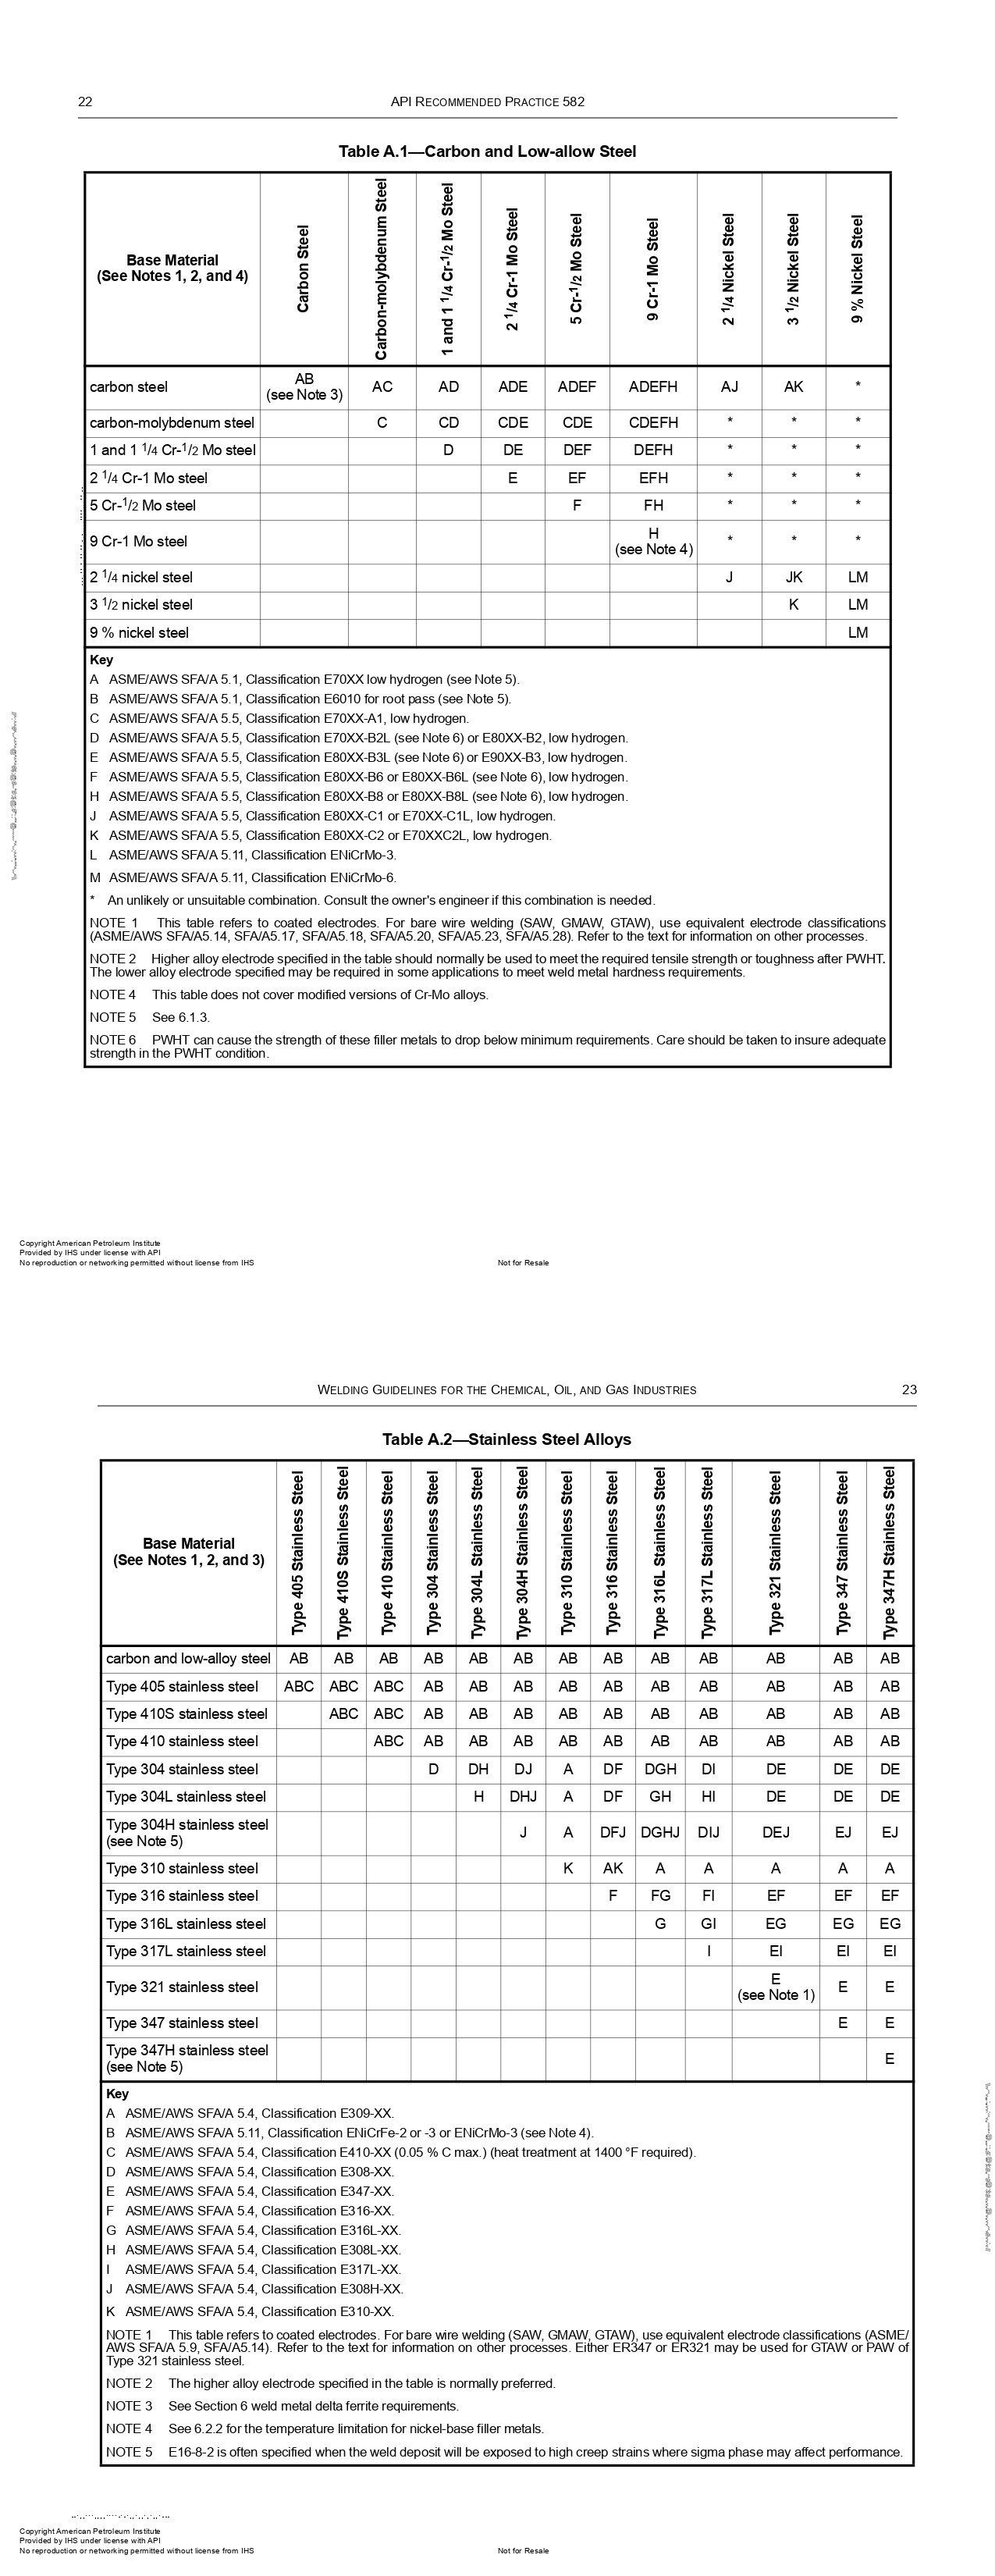
Welding A106-B To A335-P22


For welding A106-B to A335-P22, a filler metal like E8018-B2 is recommended. This electrode is suitable for similar Cr-Mo alloyed steels and is often used in steam plant, boiler plant, and pipe production applications. Alternatively, filler wires like ER80S-B2 or ER90S-B3 can be used for TIG or MIG welding. 

Elaboration:

E8018-B2:

This is a basic shielded metal arc welding (SMAW) electrode designed for welding Cr-Mo alloyed steels. It's known for producing a weld deposit with similar properties to the base metal, making it suitable for applications where strength and ductility are crucial. 

ER80S-B2 and ER90S-B3:

These are filler wires used for gas metal arc welding (GMAW) and gas tungsten arc welding (GTAW). They offer good weld properties and are compatible with A335 P22 material. 

A106-B and A335-P22:

These are both steel grades commonly used in piping and pressure vessel applications. A106-B is a carbon steel, while A335-P22 is a low-alloy steel. The welding process must consider the differences in their properties and ensure a strong, durable weld.


حد پذیرش تعمیر ترک در API 1104


جوش دارای عیب ترک باید تعمیر شود یا سرجوش کلا بریده شود ، عیب ترک یا ترک ستاره ای موجود در گرده جوش خارجی یا داخلی می تواند با سنگ زنی و بدون روش صلاحیت جوشکاری تعمیر گردد. اگر سنگ زنی باعث از بین رفتن گرده جوش شود باید با یک روش تاییدیه جوشکاری جایگزین گردد ، نیاز به برش سرجوش در حالات زیر اتفاق می افتد: 

-


  تعمیر دوباره ترک ممنوع است.


10.2.3 Crack Repiars


A weld containing a crack defect(s) shall either be repaired or cut out. Crater or star crack defect(s) found and contained completely in internal or external weld reinforcement may be repaired by grinding (i.e., abrasive methods) without a qualified repair procedure. If grinding to remove a crater or star crack defect(s) exceeds the internal or external reinforcement, the reinforcement shall be replaced using a qualified welding procedure. A cut-out is required when either of the following conditions exist.

a) A weld with a crack defect, as defined by 9.3.10, shall be cut out when the length of a single crack or the aggregate length of more than one crack is greater than 8 % of the weld length. The length of a crack is the longest dimension regardless of orientation.

b) A double repair of a crack is not permitted. Additional cracking in the weld area after repair shall require a cut-out.


جوشکاری تعمیری


E 200 Repair welding procedures

201.Repair welding shall be qualified by a separate weld repair qualification test.

202.Preheat for repair welding should be minimum 50°C above minimum specified preheat for production welding.

203.When a heat treated pipe or component is repaired by welding, a new heat treatment may have to be included in the qualification of the weld repair procedure, depending on the effect of the weld repair on the properties and microstructure of the existing weld and base material.

204.Qualification of repair welding procedures shall be made by excavating a groove in an original weld welded in accordance with a qualified welding procedure.

شیار حفر شده باید طول کافی برای بدست آوردن تعداد مورد نیاز نمونه‌های آزمایشی + 50 میلی‌متر در هر انتها را داشته باشد.

205.The excavated groove shall be of sufficient length to obtain the required number of test specimens + 50 mm at each end.

Repeated repairs

206.If repeated weld repairs are permitted or agreed, these shall be qualified separately.

207.In case of repeated repairs, the test piece shall contain a repair weld of a qualified repaired original weld. For repeated in-process root repair, single pass cap repair and/or single pass root sealing repairs the repair weld shall be removed prior to re-repair.

Qualification welding

208 .The qualification test shall be made in a manner realistically simulating the repair situation to be qualified. 

209.Qualification welding shall be performed in accordance with E101 through E108.

210.For pipeline girth welds the repair qualification welding shall be performed in the overhead through vertical positions.

211.For roll welding the length of the repair weld may be centred at the 12 o’clock location for external repairs and at the 6 o’clock location for internal repairs, in which case repair welding is qualified for repair welding in these locations only.


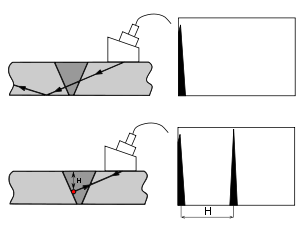
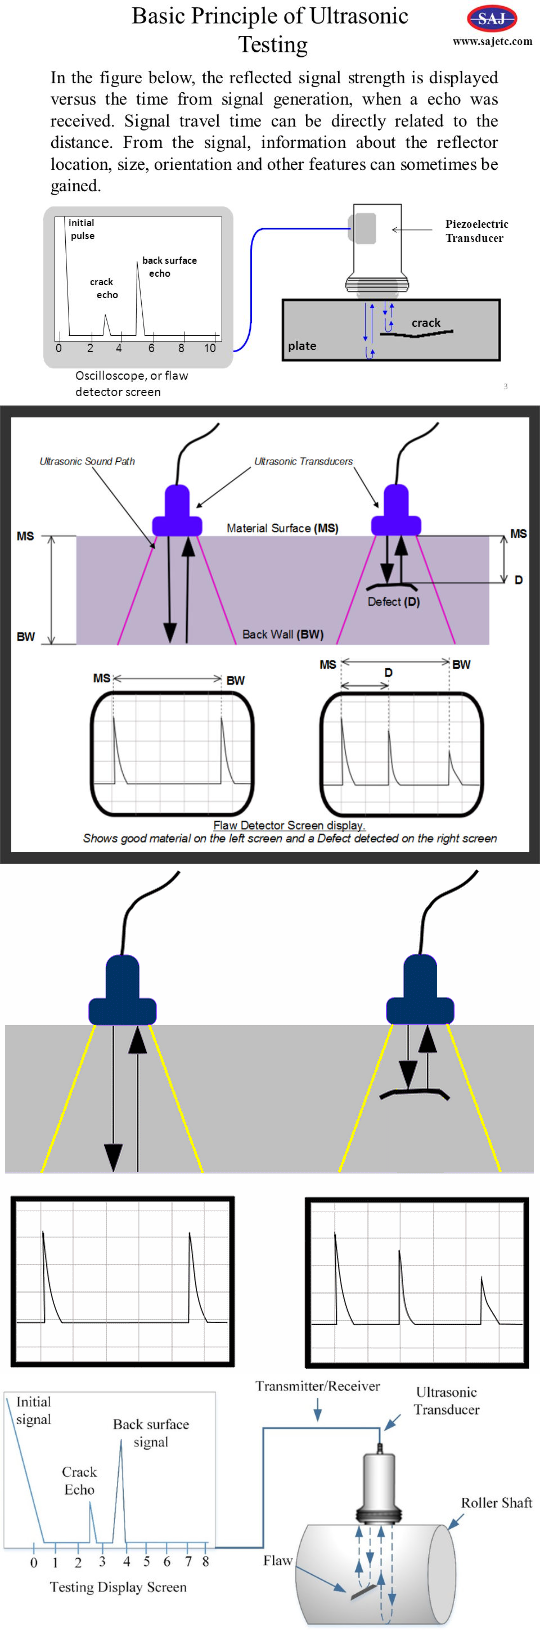
Sizing 6dB or 20dB Drop


زمانیکه اندازه ناپیوستگی بزرگتر از قطر ترانسدیوسر باشد، طول ناپیوستگی با قانون ۶  دسی بل قابل اندازه گیری است. اسکن می کنیم تا ماکزیمم ارتفاع را از عیب بگیریم و دامنه را به ۸۰ درصد میرسانیم و به سمت راست اسکن می کنیم و هر موقع که ارتفاع سیگنال به ۴۰ درصد رسید پروب را برداشته و محل مرکز پروب را بر روی قطعه کار مارک میکنیم و دوباره حالت قبلی را تکرار می کنیم اما این بار به سمت چب اسکن می کنیم و ارتفاع به ۸۰ درصد میرسد و با اسکن کردن به سمت متضاد ارتفاع اکو به ۴۰ درصد خواهد رسید باز این محل را در مرکز پروب مارک میکنیم و دو نقطه بدست آمده را به هم  میکنیم و طول عیب بدست خواهد آمد.


DNV-OS-F101

Contact surface

325 For ultrasonic testing the contact surface shall be clean and smooth, i.e. free from dirt, scale, rust, welding spatter, etc. which may influence the result of the testing. Correction for differences in surface conditions and attenuation between the reference block and the actual work piece shall be performed and the maximum correction allowed on flat surfaces is 6 dB.


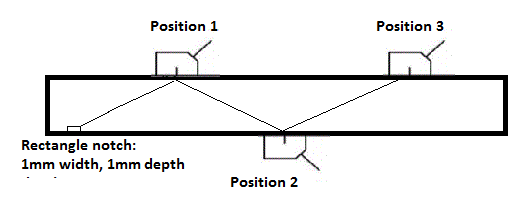
The Reference notch shall be 1mm wide, rectangular with depth of 1mm . This technique applies only for thickness range 8mm  u t<15mm and fr beam angles W 70°.


E8018-B2, the "B" indicates that the electrode contains certain alloying elements such as chromium (Cr), molybdenum (Mo), and boron (B). These elements contribute to the low-alloy steel's strength and toughness, making it suitable for applications requiring high strength and impact resistance.


8018-C1 is a low alloy, low hydrogen, iron powder electrode designed to weld 2% nickel steels in the 70-80,000 psi range and where low temperature, impact properties must be good. This electrode provides a stable arc in flat and horizontal fillet welding positions, producing weld deposits with fine bead appearance, free from undercuts and with excellent mechanical properties. 8018-C1 may be used with AC or DC (reverse polarity).


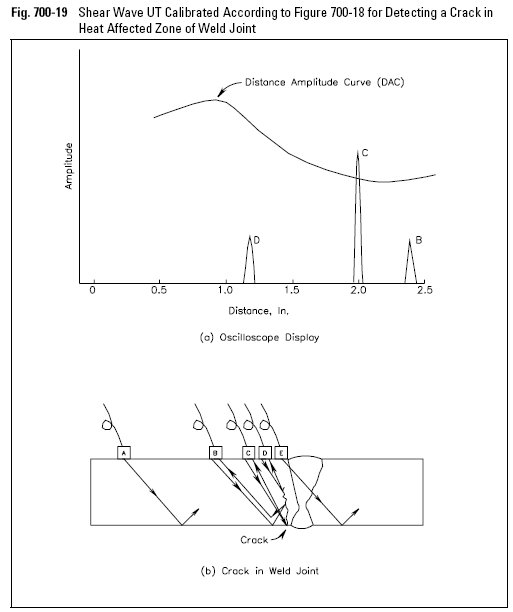
بازرسی جوش به روش UT و حد پذیرش


یک استاد دانشگاه درباره اقدام اخیر متروی تهران نوشت: برگزاری مسابقه نامه خودمونی به خدا از سوی مترو کار خوبی است اما بهتر است در کنار این اقدامات که مسجد محل هم می تواند انجام دهد، بخش اجتماعی مترو به کارهای اصلی خود بپردازد. ایجاد نارضایتی و ناراحتی هنر نیست.


بکارگیری اتباع خارجی بدون پروانه کار در مشاغل حوزه سلامت از قبیل مواد غذایی و بهداشت و درمان (رستوران، آشپزخانه، درمانگاه، داروخانه و ...) ممنوع است.


معاونت اجتماعی و پیشگیری از وقوع جرم دادگستری استان تهران 


شروط غیرقانونی در قرارداد کار چه هستند؟

شروط غیرقانونی در قرارداد کار، به توافقاتی گفته می‌شود که برخلاف قوانین آمره کار تنظیم شده‌اند و حتی در صورت رضایت کارگر، فاقد اعتبار قانونی هستند. یکی از مهم‌ترین نمونه‌های این شروط، تعیین ساعت کاری بیش از ۴۴ ساعت در هفته است که با قانون کار مغایرت دارد. همچنین گاهی کارفرما برای خود حق فسخ یک‌طرفه قرارداد را با تعیین مدت زمان مشخصی، مانند ۴۵ روز، قائل می‌شود که این شرط نیز برخلاف اصول قانونی روابط کار است.

از دیگر مصادیق شروط غیرقانونی می‌توان به تبعیض‌های جنسیتی در مزایای شغلی اشاره کرد؛ برای مثال، محروم کردن کارکنان زن از دریافت حق اولاد یا حق تأهل، امری غیرقانونی محسوب می‌شود. در برخی قراردادها نیز توافق می‌شود که مبلغ عیدی کمتر از میزان تعیین‌شده توسط قانون پرداخت شود یا دستمزد کارگر کمتر از حداقل دستمزد مصوب وزارت کار تعیین گردد که هر دو مورد باطل و فاقد اعتبار هستند.


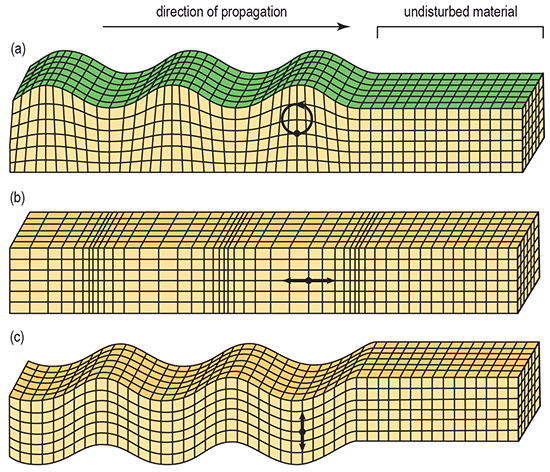
Three types of seismic waves: 

(a) Rayleigh wave  ( Surface wave )

(b) compressional wave ( longitudinal wave )

(c) shear wave


Q30. During ultrasonic inspection (UT) on a 20 mm thick weld, an indication having length 2 mm observed, which is characterised as lack of fusion between the base metal and weld metal. As per the acceptance criteria in ASME Section VIII Division 1, this defect is: 
Not Acceptable
Acceptable
Acceptance depends upon the depth of flaw
None of above

(Explanation: According to ASME Section VIII Division 1, any indication characterized as a lack of fusion is unacceptable regardless of its size. Since the 2 mm long indication in the 20 mm thick weld has been characterized as lack of fusion, it would be unacceptable per ASME Section VIII Division 1 criteria, regardless of its size or depth


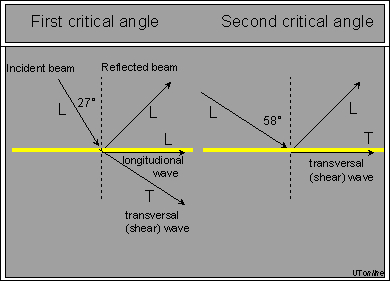
The angle at which 90° refraction of a longitudinalsound wave is reached is called the:

a. angle of incidence.

b. first critical angle.

c. angle of maximum reflection.

d. second critical angle.


When inspecting aluminum by the immersion method using water for a couplant, the following information is known: velocity of sound in water = 1.49 × 105 cm/s, velocity of longitudinal waves in aluminum = 6.32 × 105 cm/s, and angle of incidence = 5°. The angle of refraction for longitudinal waves isapproximately:

a. 22°

b. 18°

c. 26°

d. 16°

Sin5/x = 1.49 / 6.32


Beam divergence ( spread out ) is a function of the dimensions of the crystal and the wavelength of the beam transmitted through a medium, and it:

a. increases if the frequency or crystal diameter decreases.

b. decreases if the frequency or crystal diameterdecreases.

c. increases if the frequency increases and crystaldiameter decreases.

d. decreases if the frequency increases and crystaldiameter decreases.


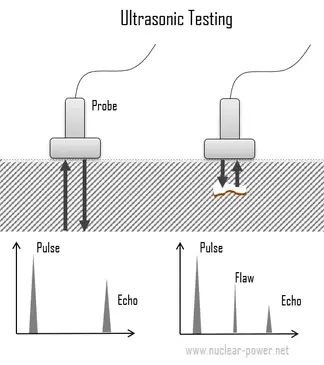
The indication on the instrument display that represents the far boundary of the material being tested is called:

a. grass or hash.
b. the initial pause.
c. the main bang.
d. the back-surface reflection.


Moving a transducer over a test surface either manually or automatically is referred to as:

a. scanning.
b. attenuating.
c. angulating.
d. resonating.


A term  اصطلاحی که used in ultrasonics to express the rate at which sound waves pass through various substances is:

a. frequency.
b. velocity.
c. wavelength.
d. pulse length.


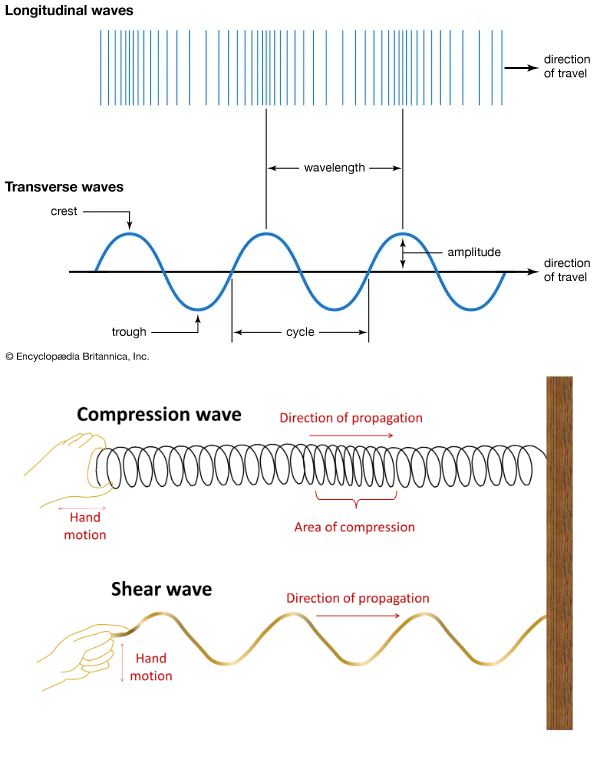
When the motion of the particles حرکت ذرات یک محیط  of a medium is transverse to the direction of propagation, the wave being transmitted is called a:

a. longitudinal wave.
b. shear wave.
c. surface wave.
d. lamb wave.


The boundary between  مرز بین two different materials دو ماده متفاوت  that are in contact with each other is called:

a. a rarefactor.
b. a refractor.
c. an interface.
d. a marker.


For discontinuity geometries other than flat, the echo amplitude دامنه اکو is usually from that observed _________ for a flat discontinuity, of similar orientation perpendicular to the sound beam.

a. identical

b. increased

c. decreased

d. elongated


To evaluate discontinuities that are oriented at anangle to the entry surface so that the sound beam strikes the plane of the discontinuity at right angles,the operator must:

a. change the frequency.

b. grind the surface.

c. angulate the transducer.

d. increase the gain.


In immersion testing, to remove the second water reflection from between the entry surface signal and the first back reflection, you should:

a.increase the repetition rate.

b.decrease the frequency.

c.decrease the sweep length.

d. increase the water path.


If a discontinuity is oriented at an angle other than90° to the sound beam, the results may be a:

a. loss of signal linearity.

b. loss or lack of signal reflected from thediscontinuity.

c. focusing of the sound beam.

d. loss of interference phenomena.


The change in direction of an ultrasonic beam whenit passes from one material to another material inwhich elasticity and density difer is called:

a.reflection 

b.rarefaction

c.angulation.

d.refraction.


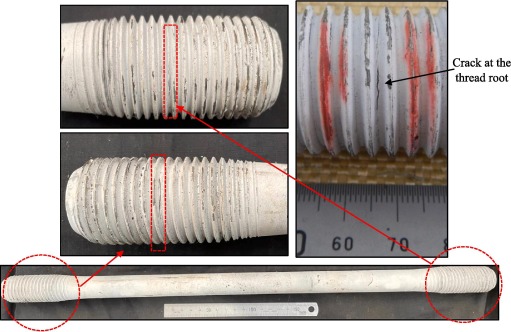
In inspecting a 102 mm (4 in.) diameter threadedsteel cylinder for radial cracks extending from theroot of the threads, it would be preferable to transmit:


a.shear waves at an angle to the threads.

b.longitudinal waves from the end of the cylinder and perpendicular to the direction of the threadroots.

c. surface waves perpendicular to the thread roots.

d. shear waves around the circumference of the cylinder.


The distance from a given point on an ultrasonic wave to the next corresponding point is referred to as:

a. frequency.

b. wavelength.

c. velocity.

d. pulse length.


A testing technique in which the crystal or transducer is parallel to the test surface and ultrasonic waves enter the material being tested in a direction perpendicular to the test surface is:

a. straight beam testing.

b. angle beam testing.

c. surface wave testing.

d. lamb wave.


Which one of the following frequencies wouldprobably result in the greatest ultrasonic attenuationlosses?

a.1 MHz

b.2.25 MHz

c.10 MHz

d.25 MHz


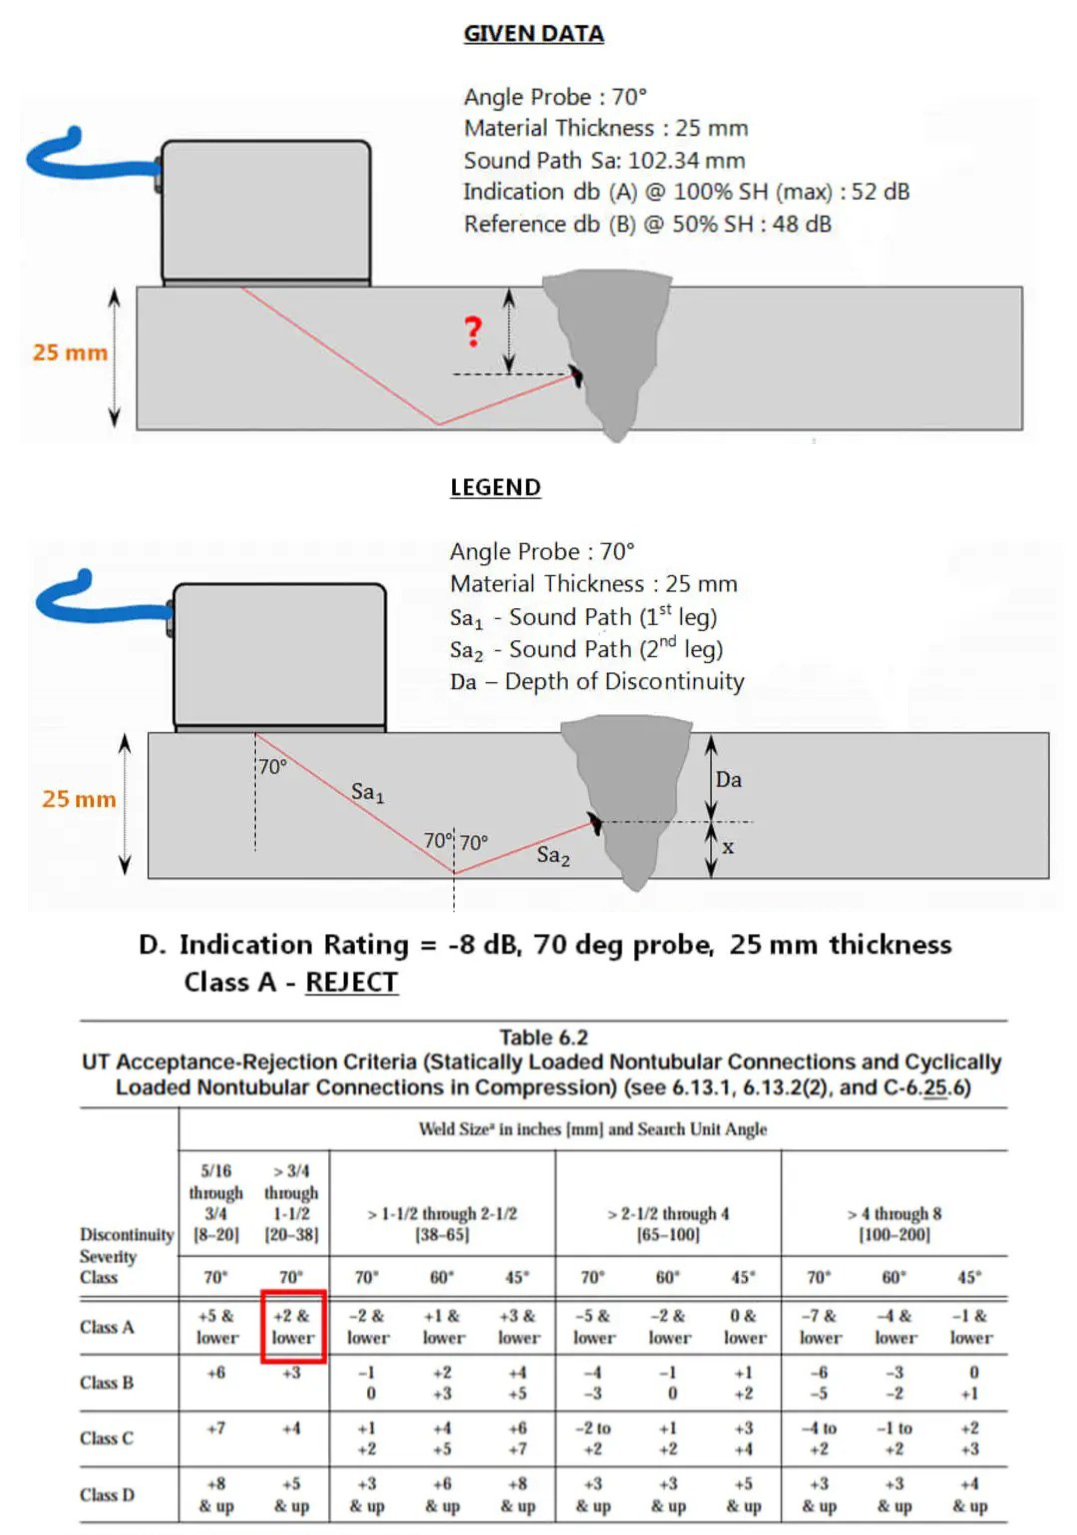
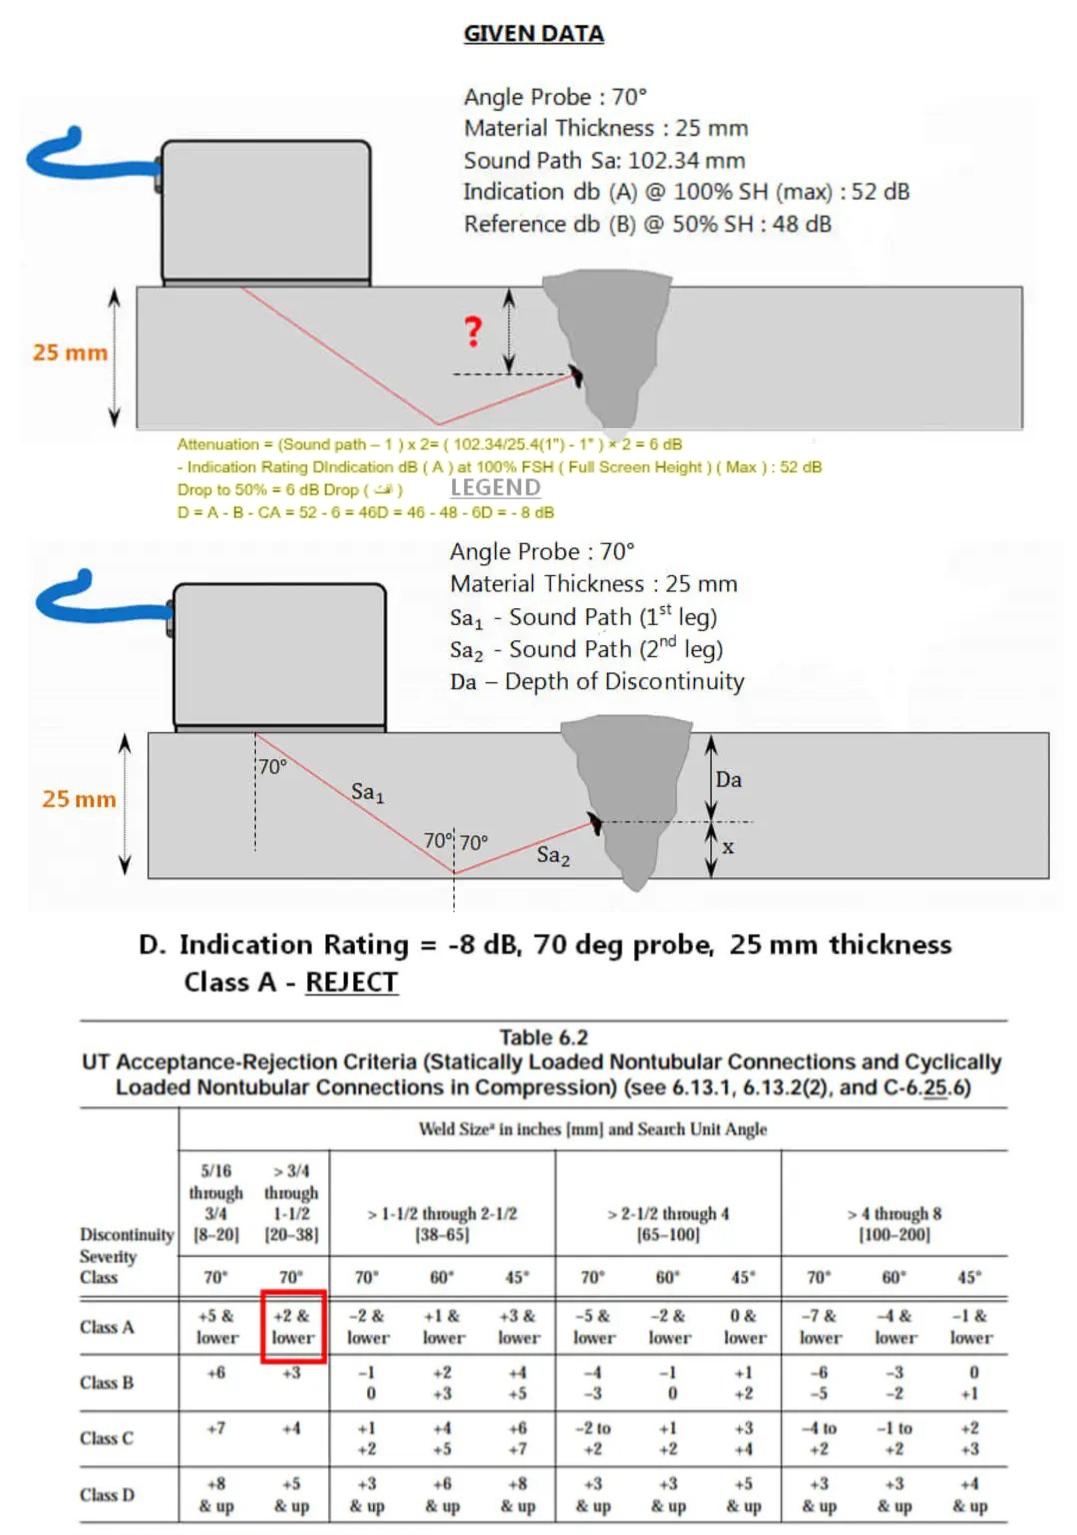
"c" – Attenuation factor is attained by subtracting 1 inch (25mm) from the sound – path distance and multiplying the remainder by ⁰. The factor shall be rounded out to the nearest dB value.


Attenuation = (Sound path – 1 ) x 2

= ( 102.34/25.4(1") - 1" ) × 2 = 6 dB

- Indication Rating D

Indication dB ( A ) at 100% FSH ( Full Screen Height ) ( Max ) : 52 dB

Drop to 50% = 6 dB Drop ( افت ) 

D = A - B - C

A = 52 - 6 = 46

D = 46 - 48 - 6

D = - 8 dB


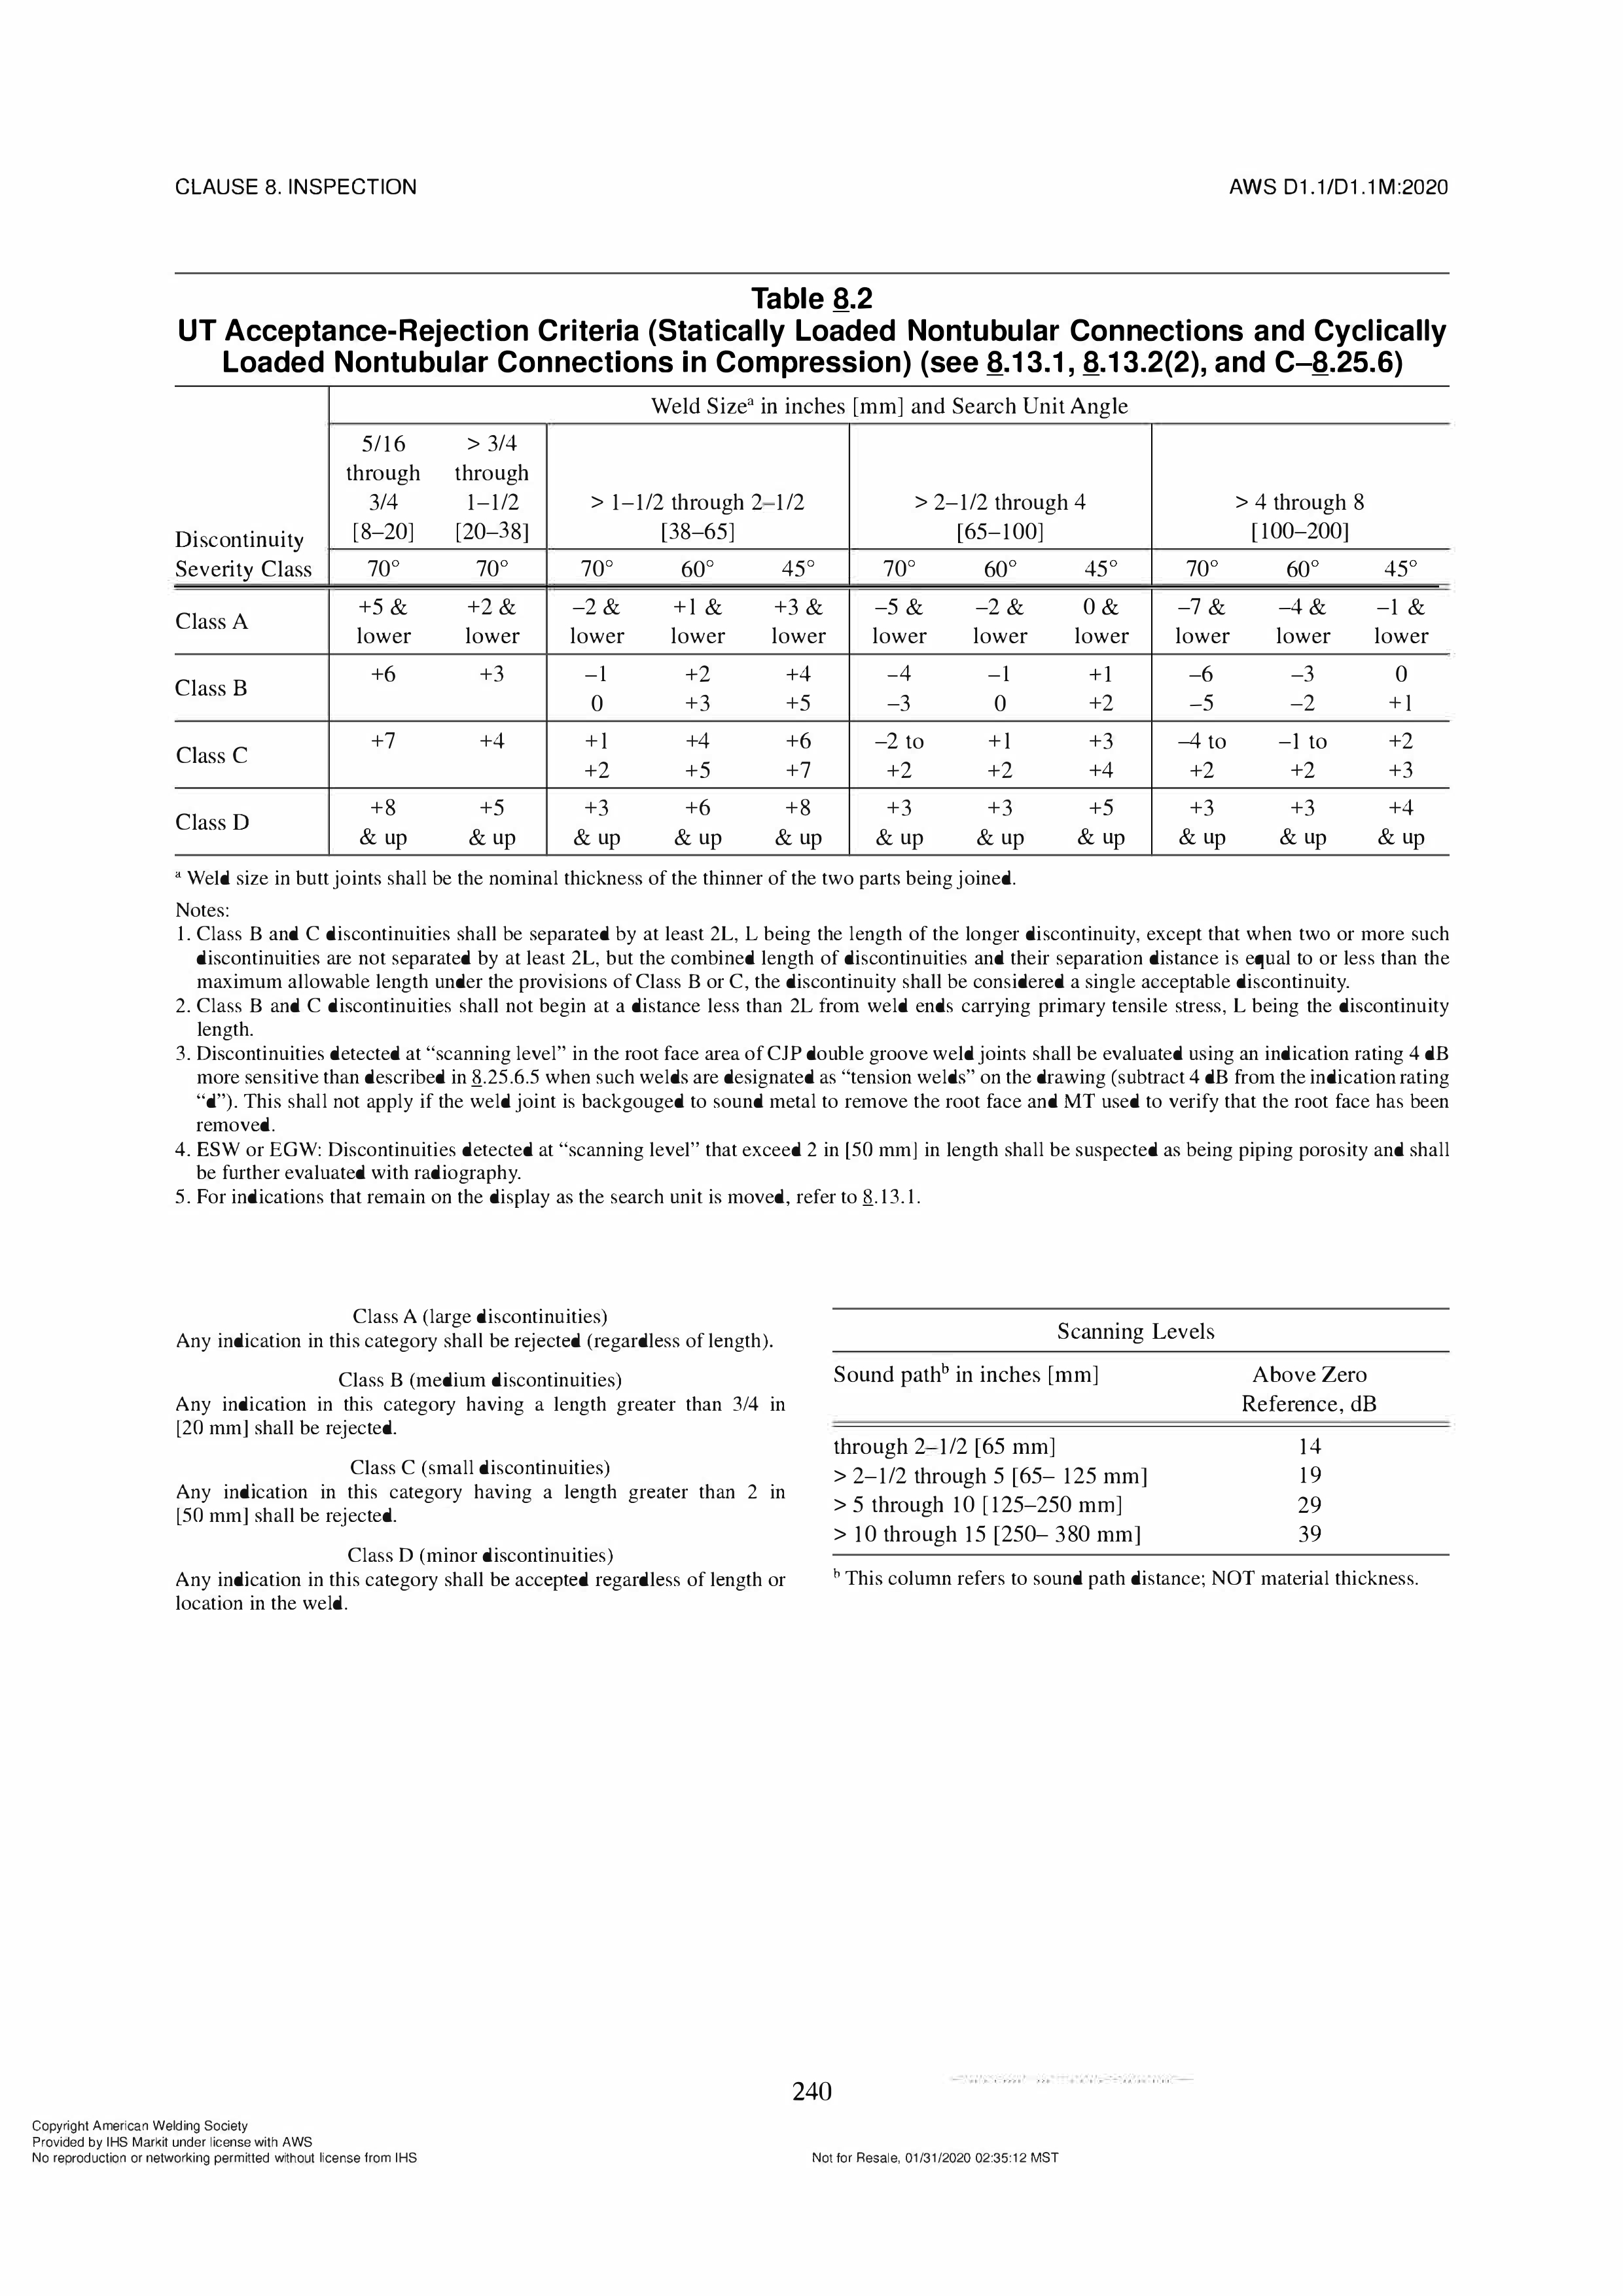
ASME B 31.1 – Power Piping – Ultrasonic Testing .

Welds that are shown by ultrasonic examination to have discontinuities that produce an indication greater than 20% of the reference level shall be investigated to the extent that ultrasonic examination personnel can determine their shape, identity, and location so that they may evaluate each discontinuity for acceptance in accordance with (B.1) and (B.2) below.

(B.1) Discontinuities evaluated as being cracks, lack of fusion,. or incomplete penetration are unacceptable regardless of length.

(B.2) Other discontinuities are unacceptable if the indication exceeds the reference level and their length exceeds the following:

(B.2.1) ¼” (6.0 mm) for t up to ¾” (19.0 mm).

(B.2.2) 1/3 t for from ¾” (19.0 mm) to 2 ¼ “ (57.0 mm).

(B.2.3) ¾”. (19.0 mm) for over 2¼” (57.0 mm)

Where is the thickness of the weld being examined. If the weld joins two members having different thicknesses at the weld, is the thinner of these two thicknesses


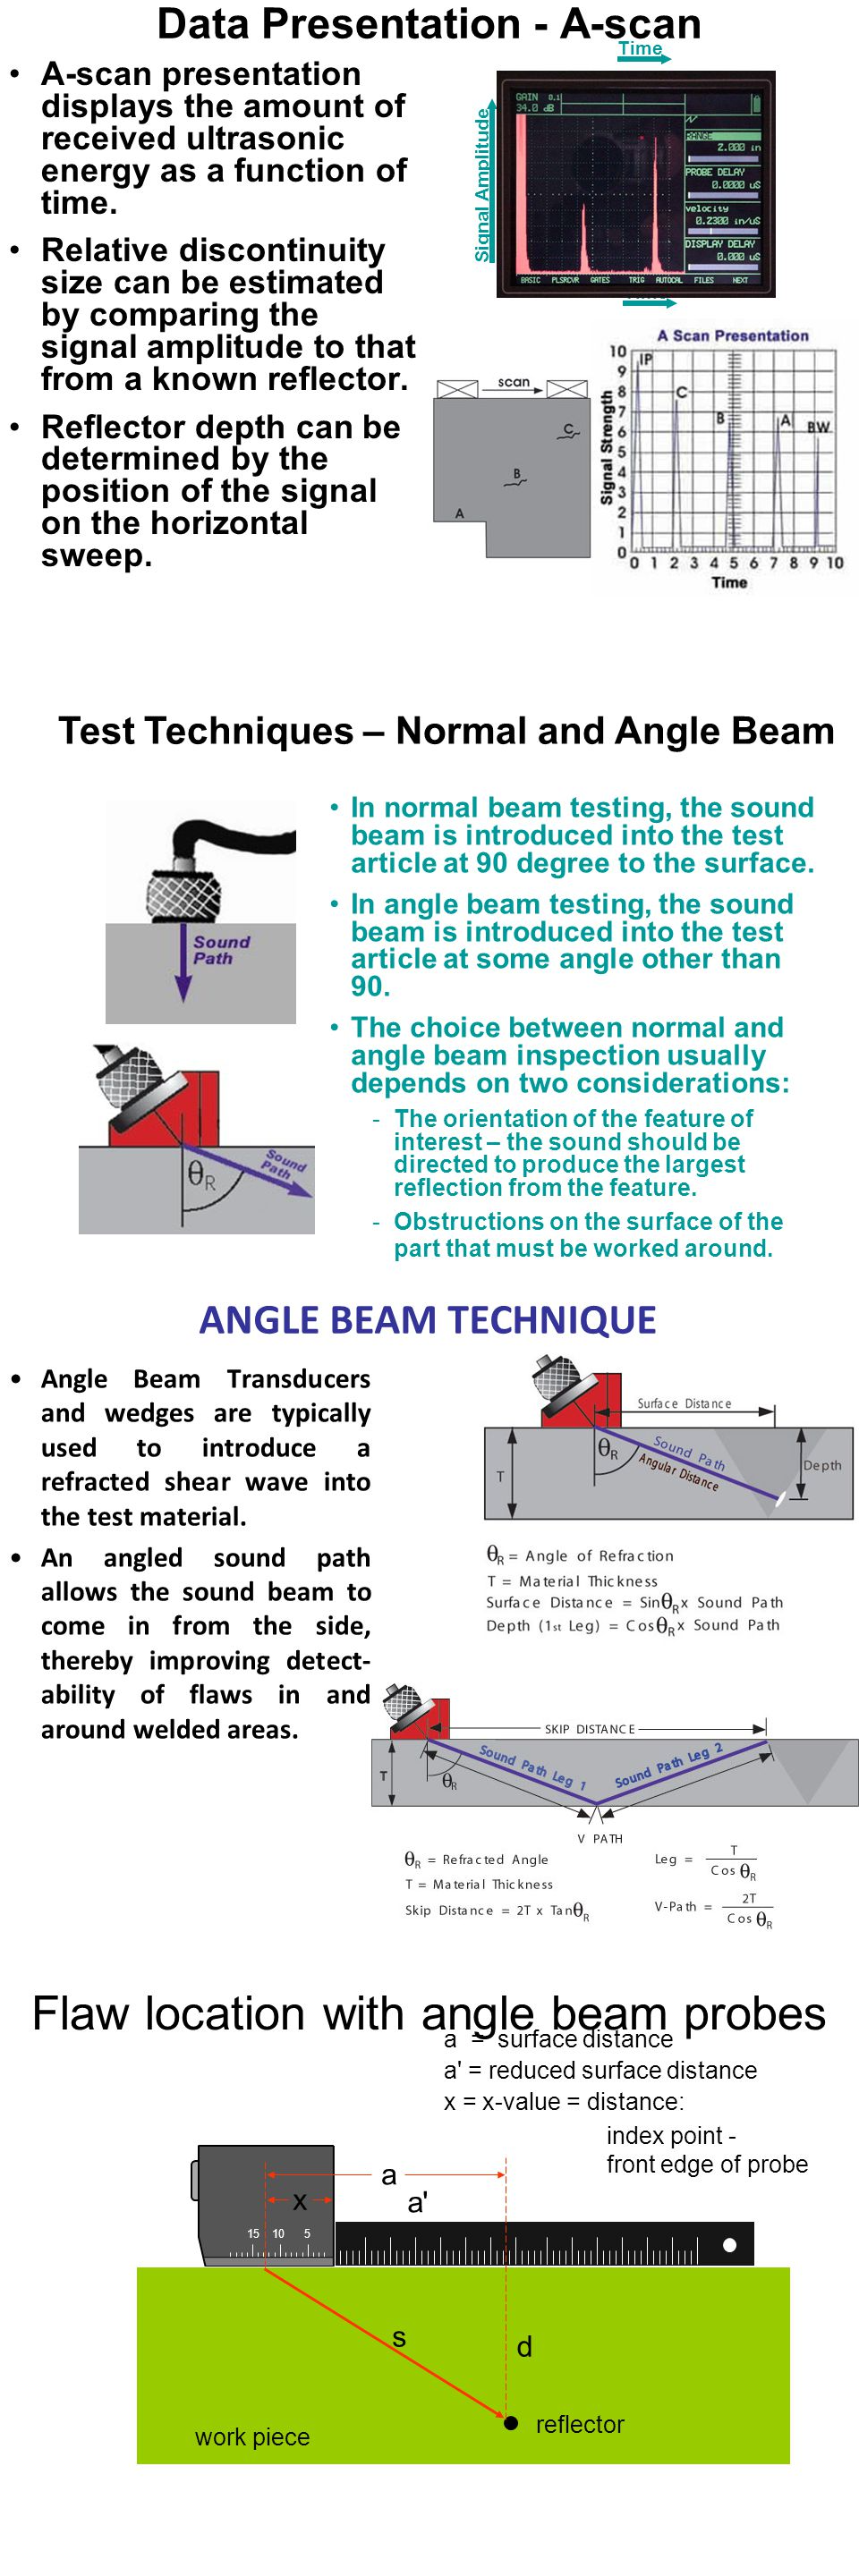
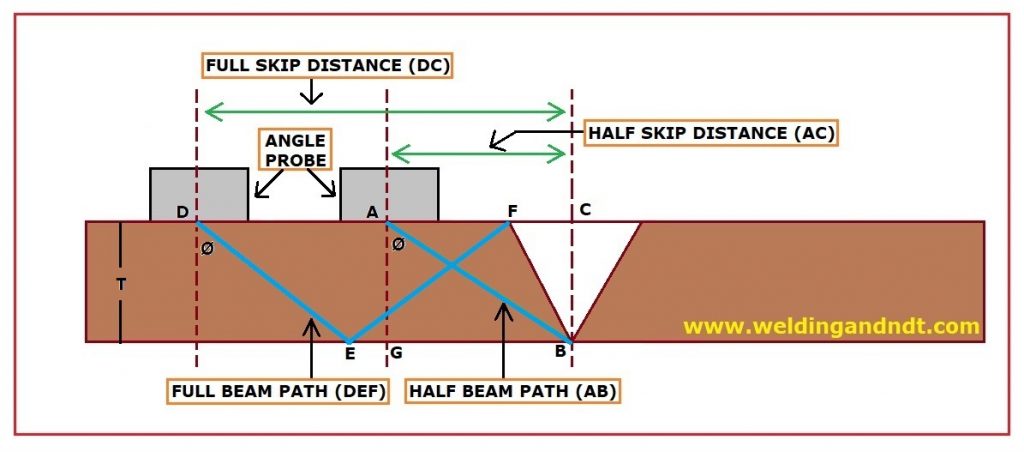
Or, HSD = T X Tan Ø

Similarly, FSD = 2T X Tan Ø

And, 1-1/2 Skip Distance = 3T X Tan Ø


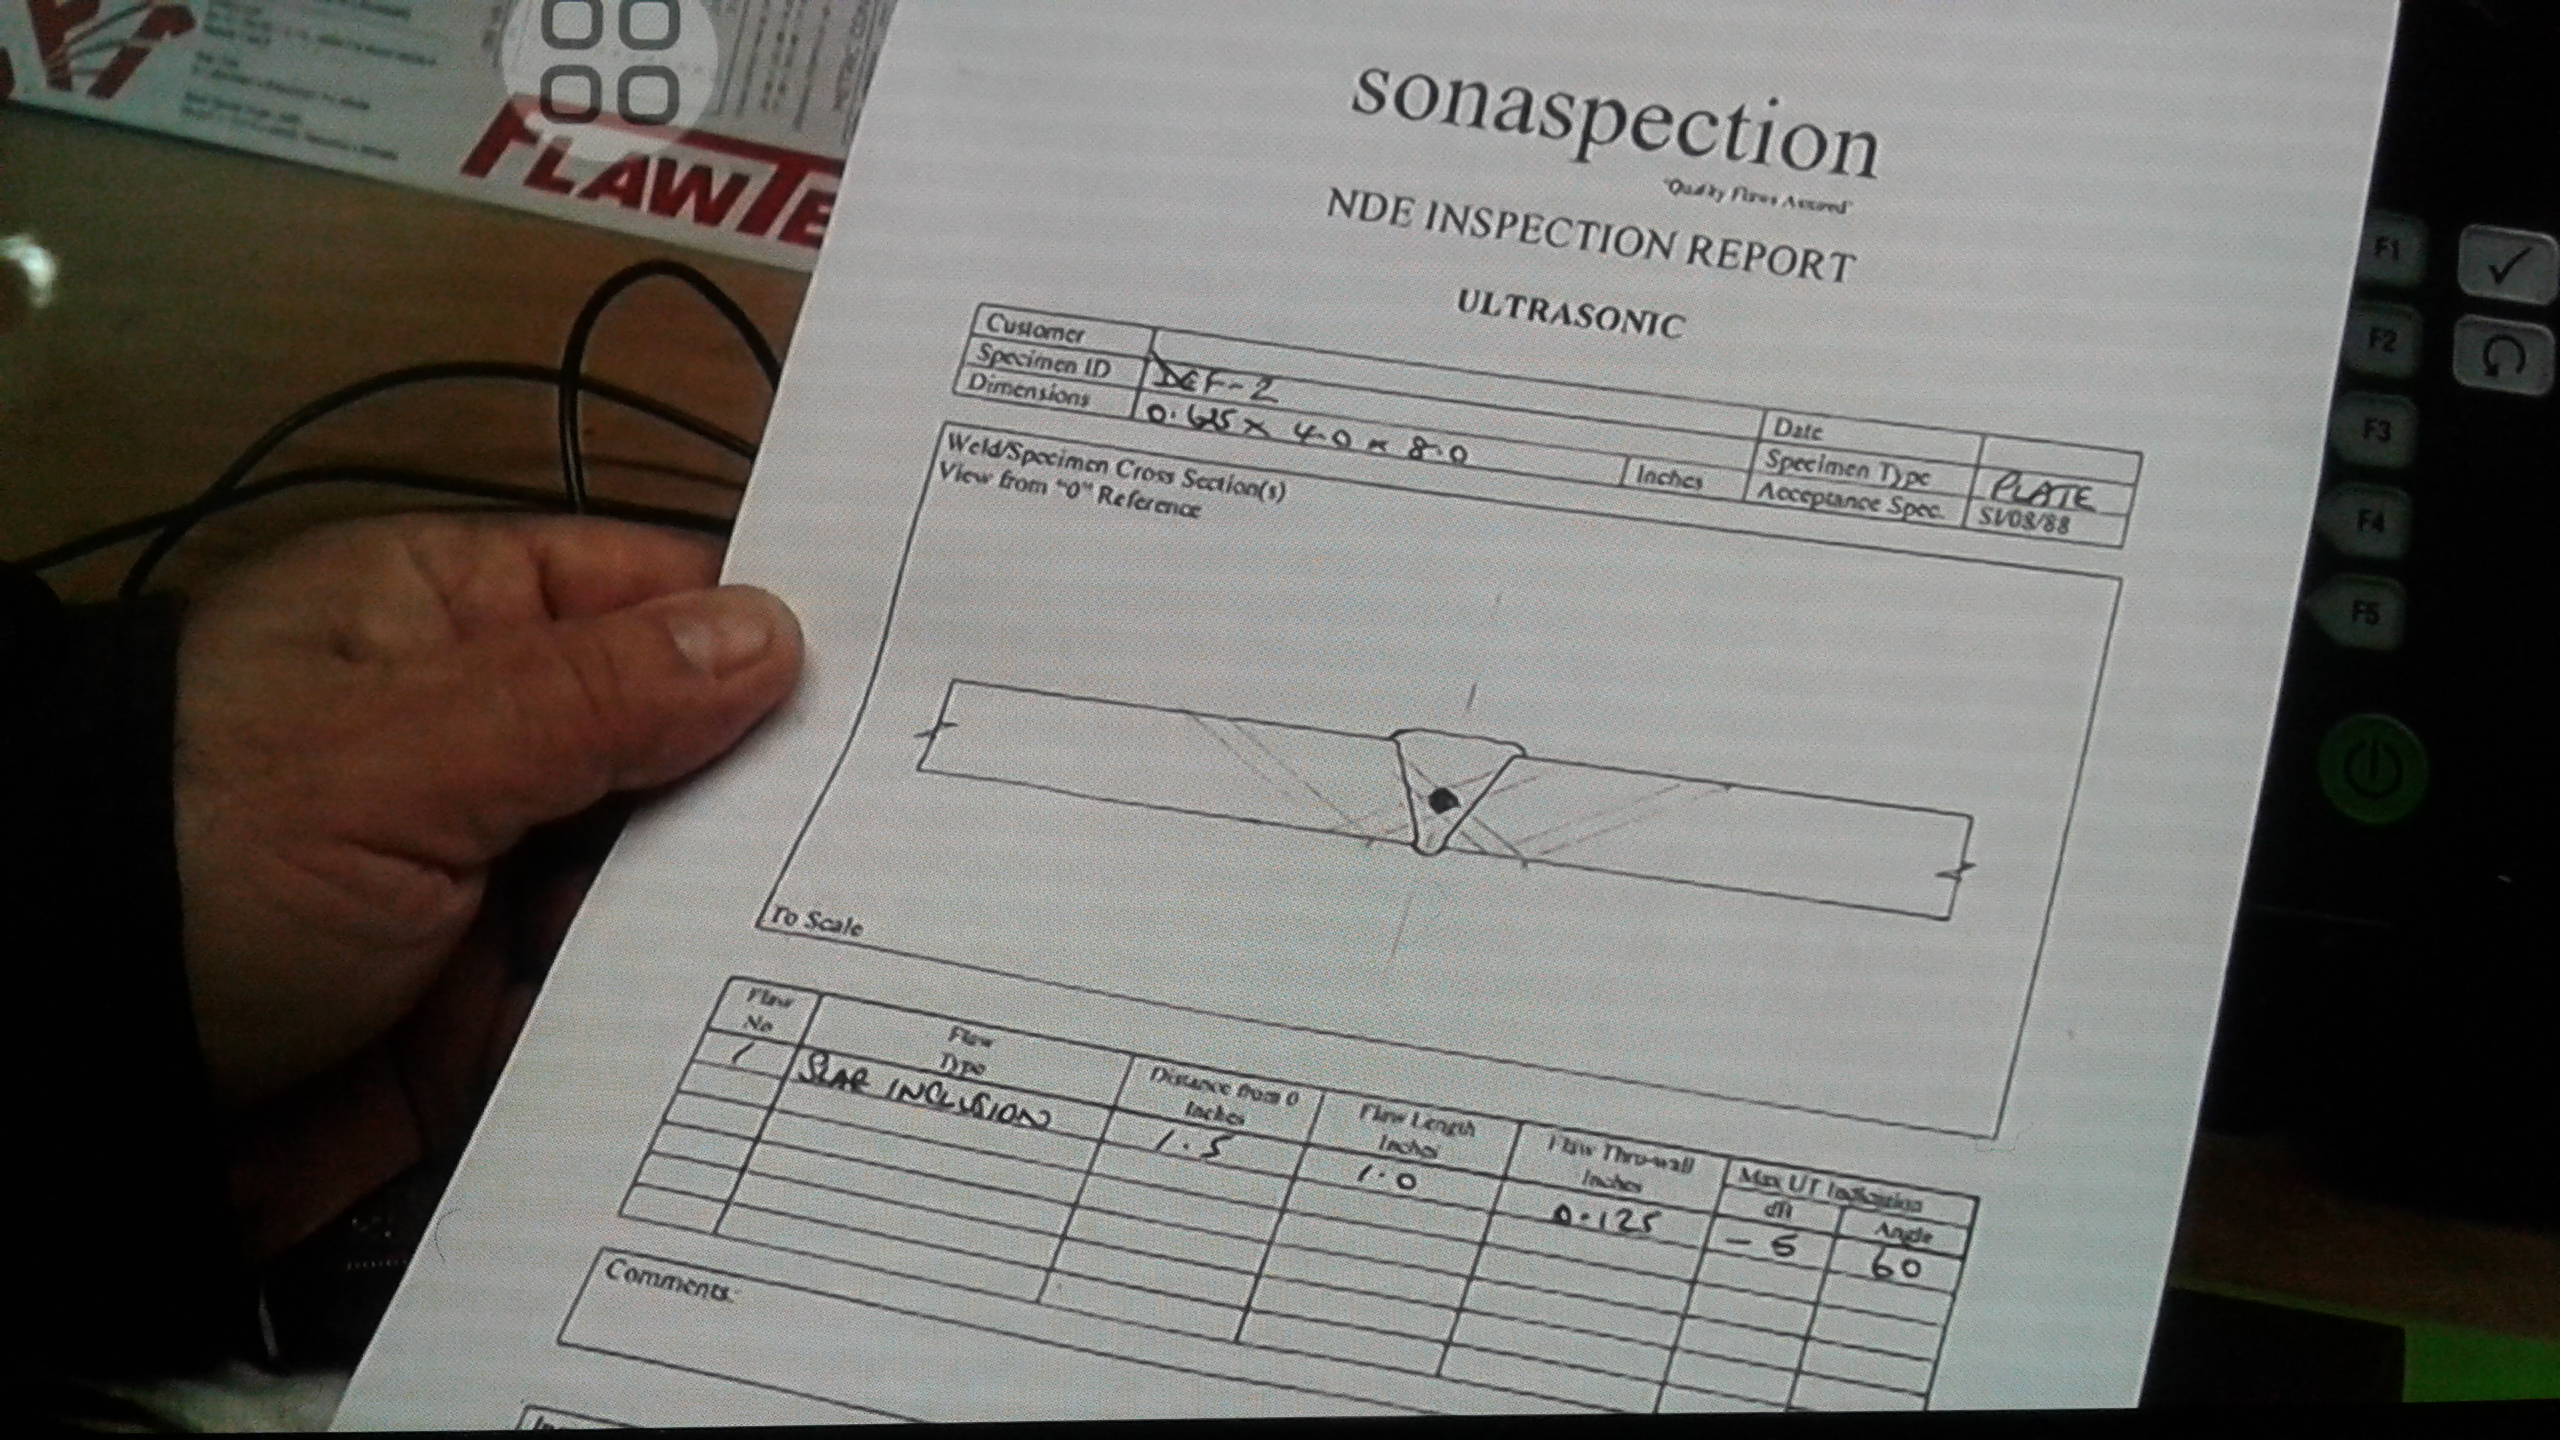
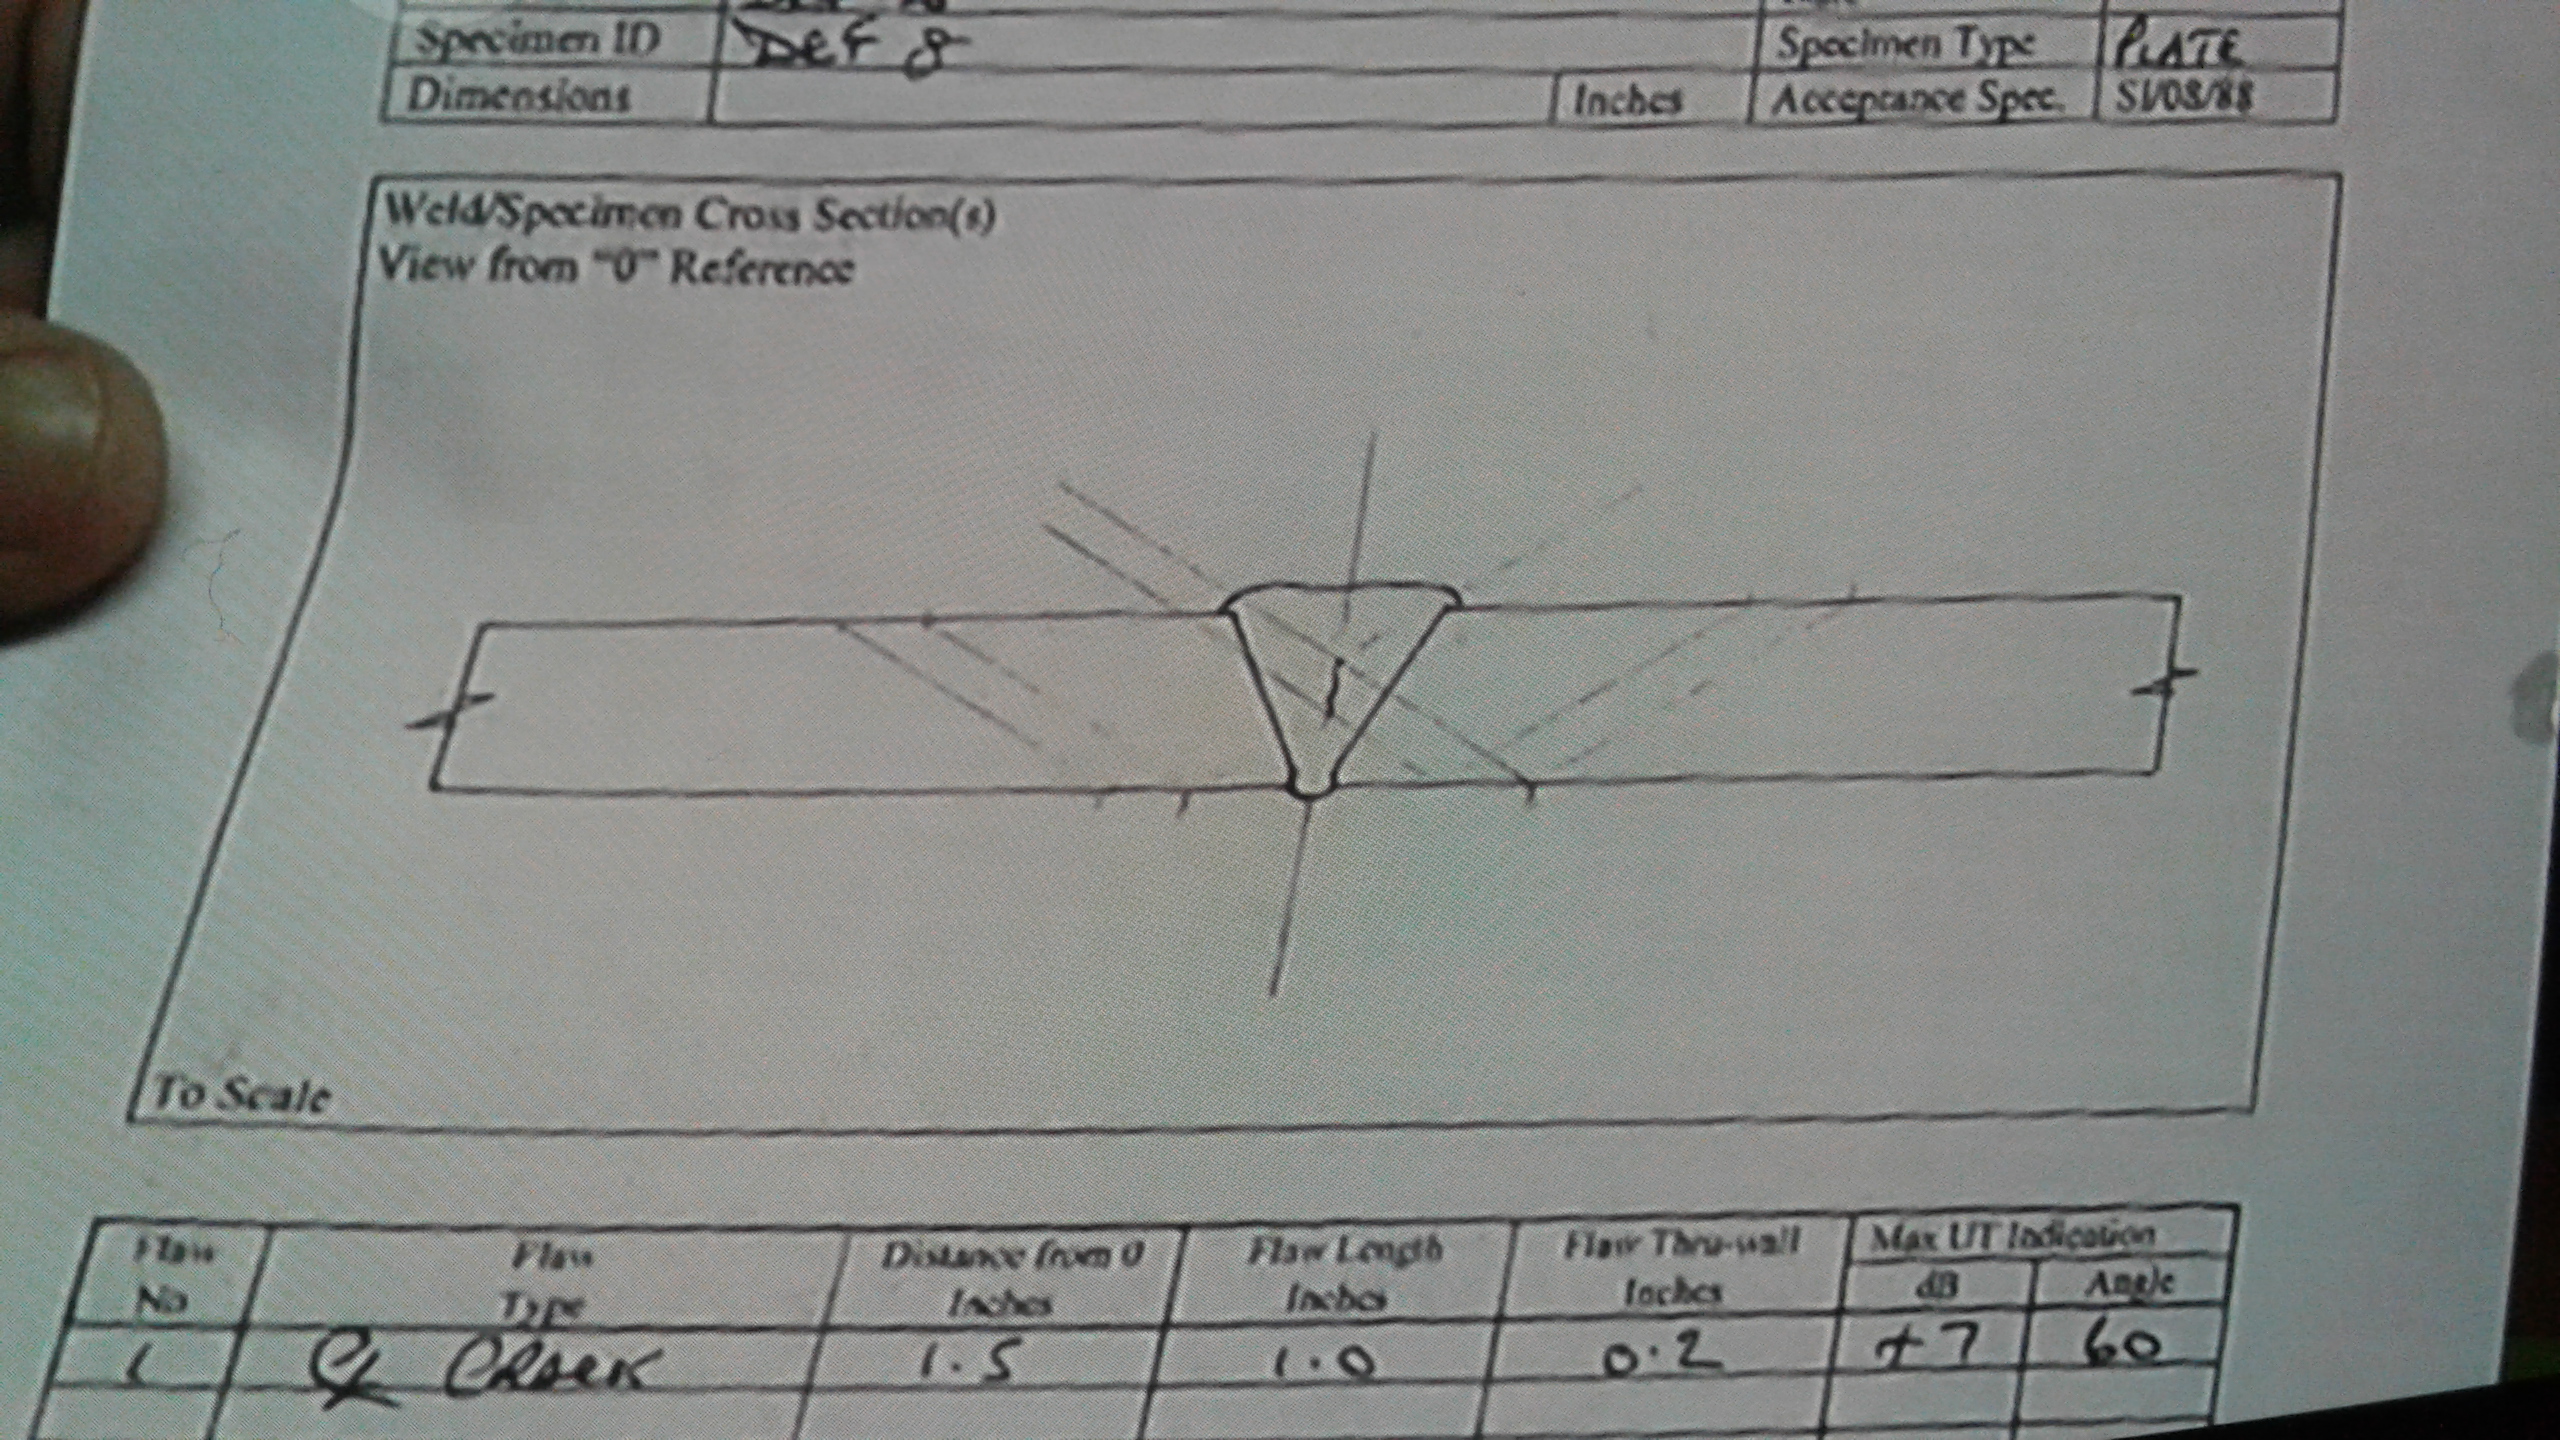
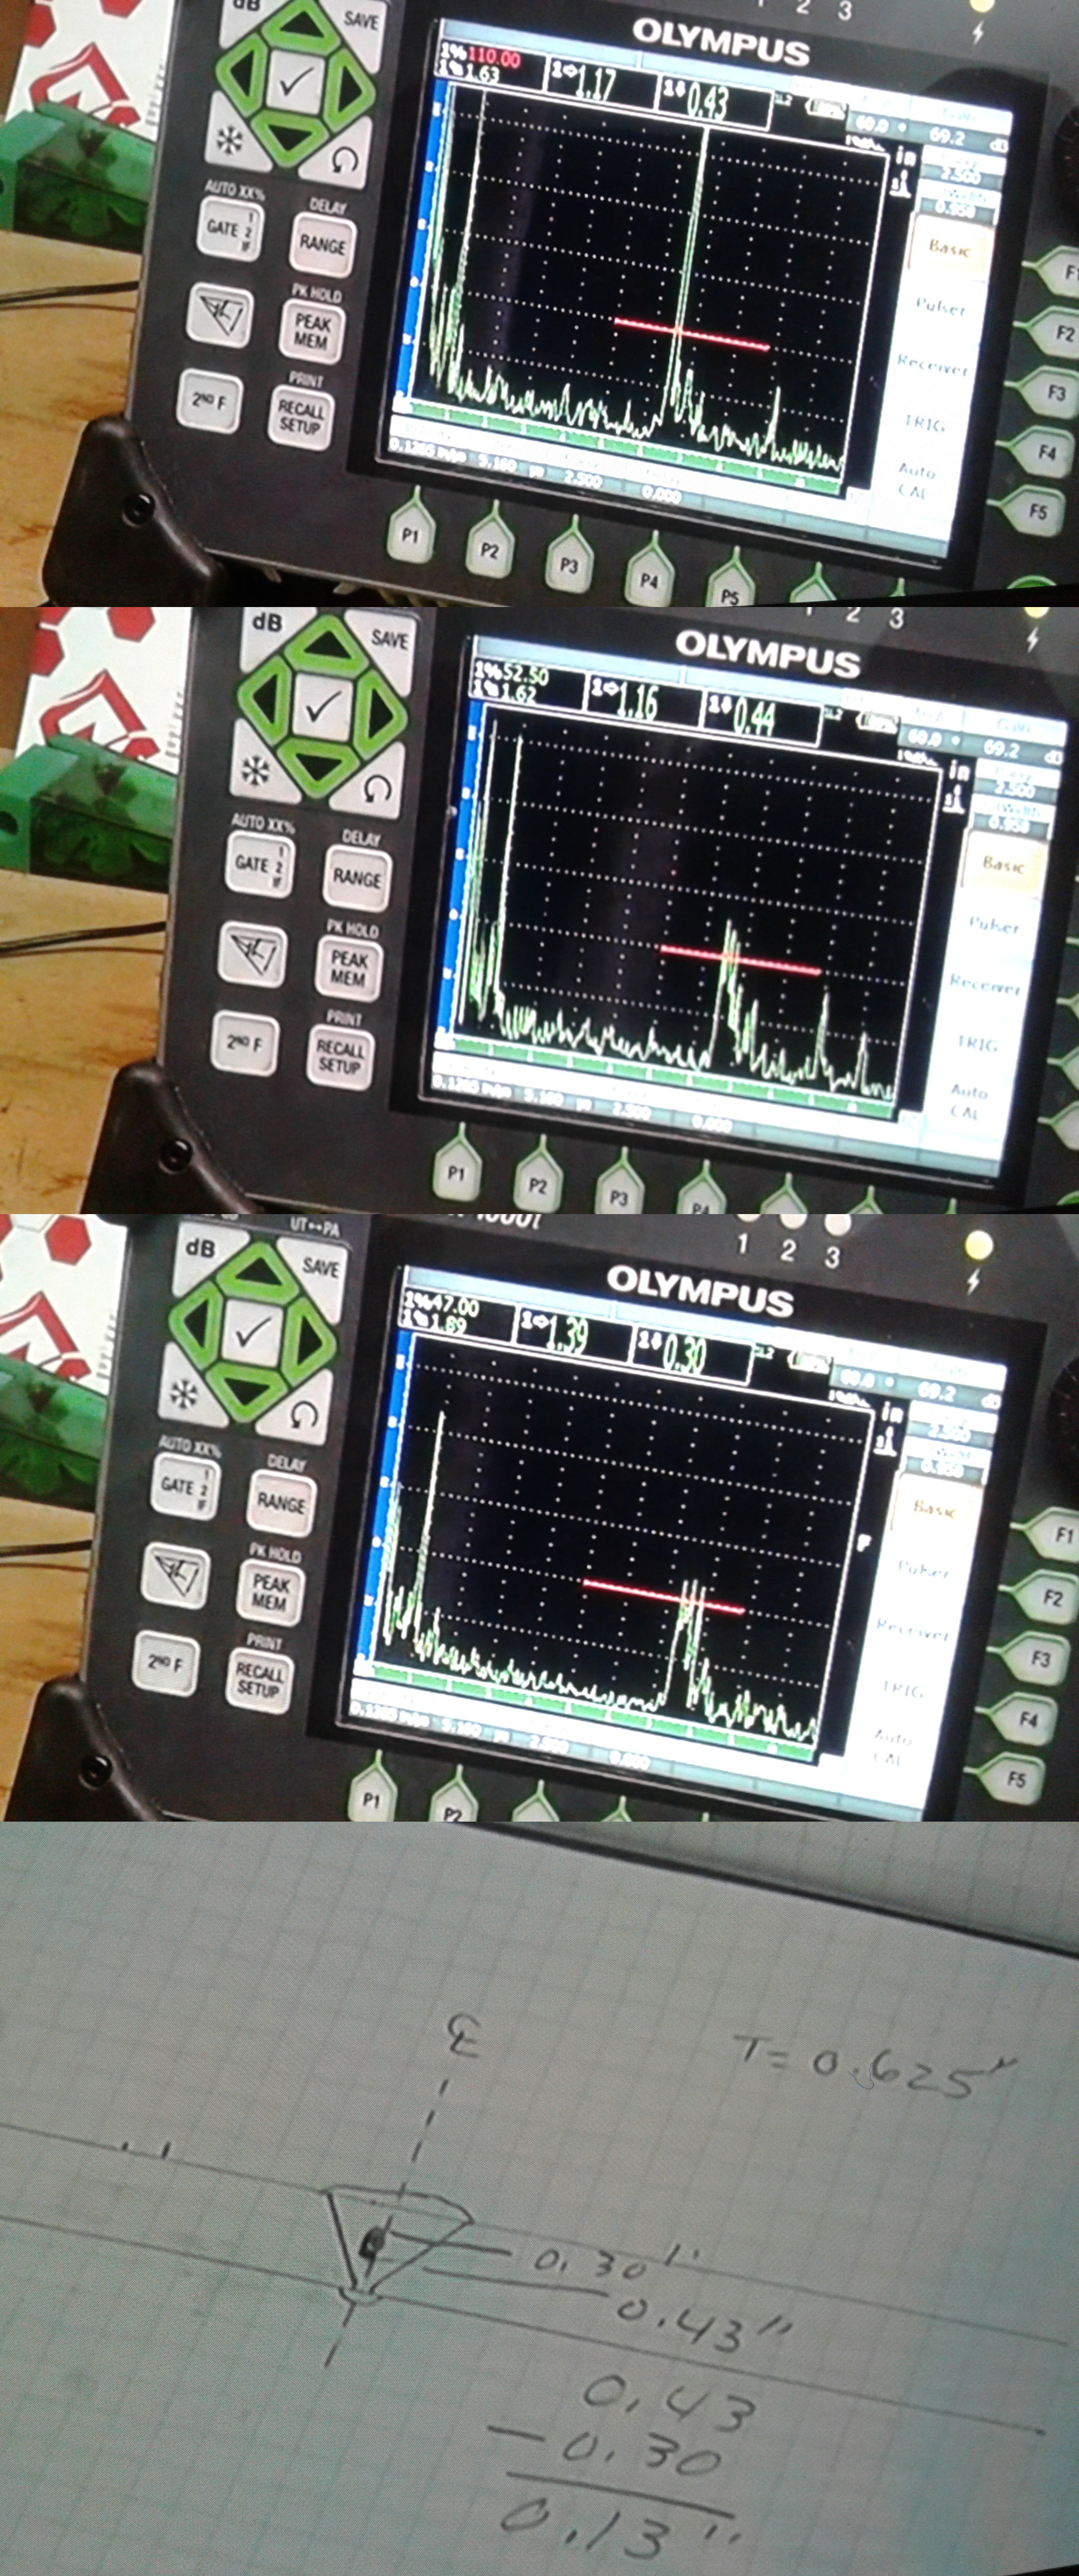
Slag Inclusion 

LEG 2


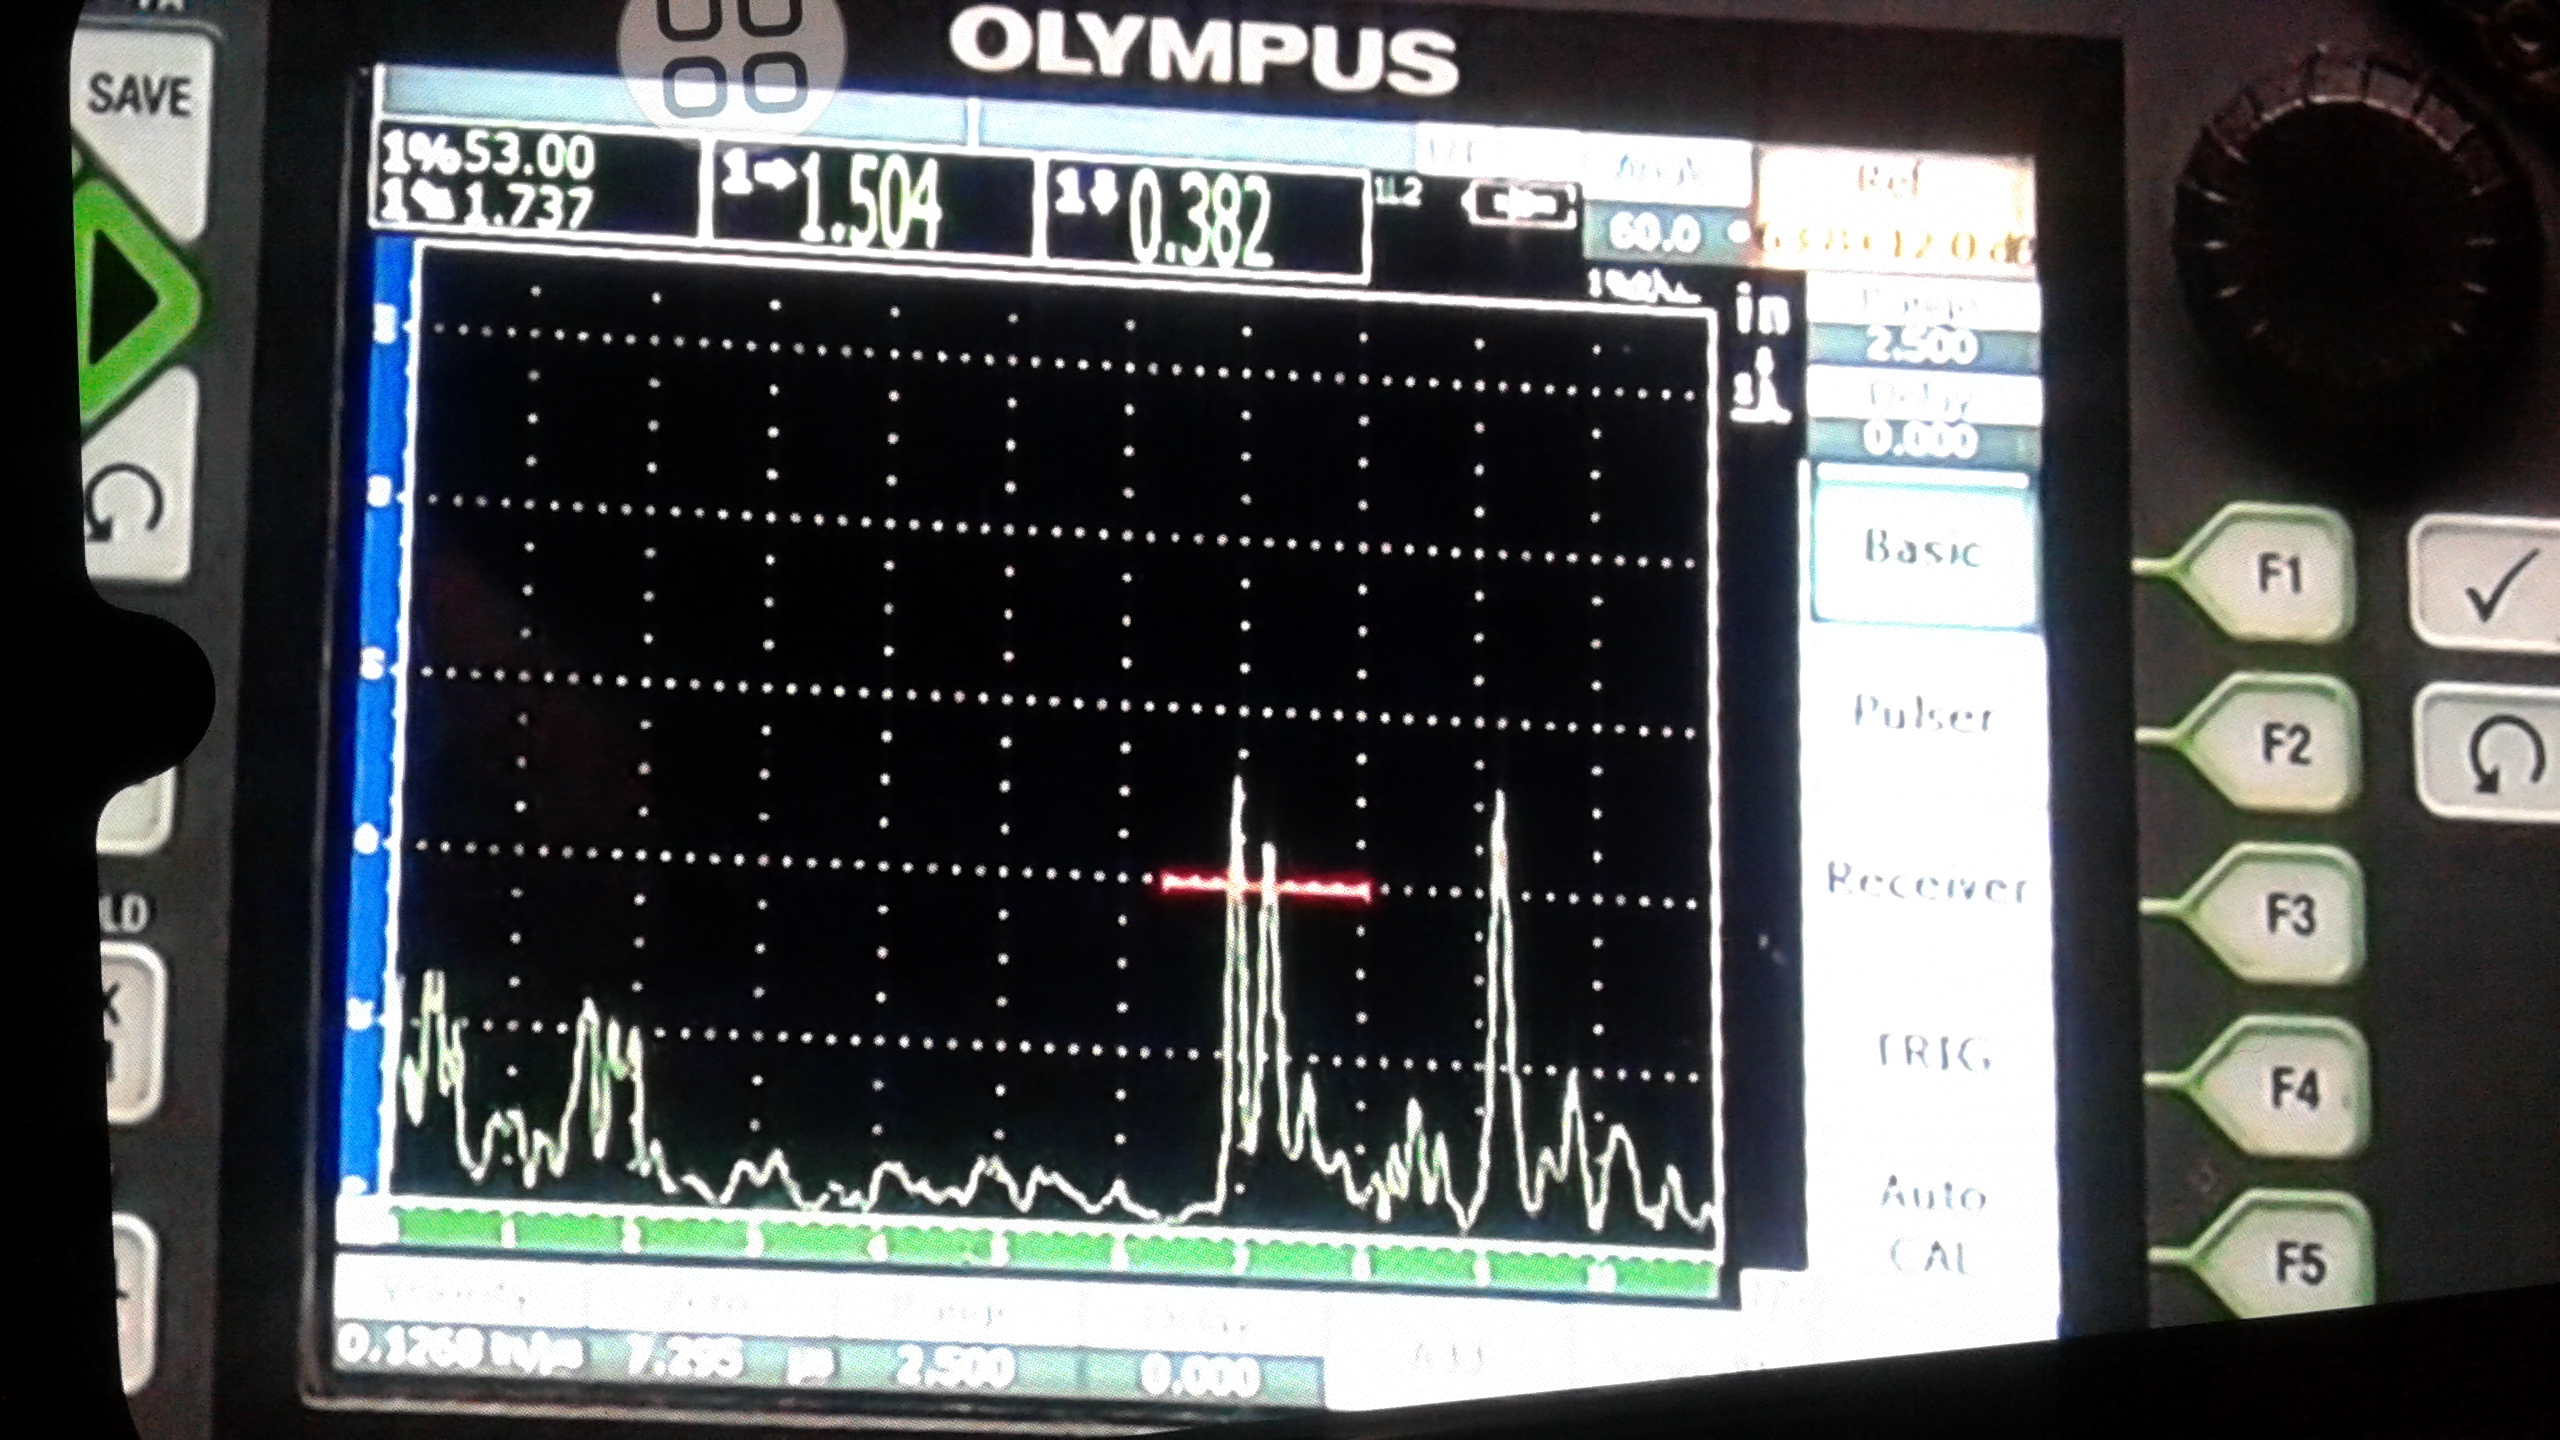
T : 0.625 INCH

SOUND PATH (SA) : 1.736 INCH

DISTANCE FROM ZERO : 1.504

SA1+SA2=1.736

DEPTH : 0.382


POROSITY

SIZING


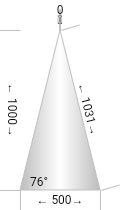
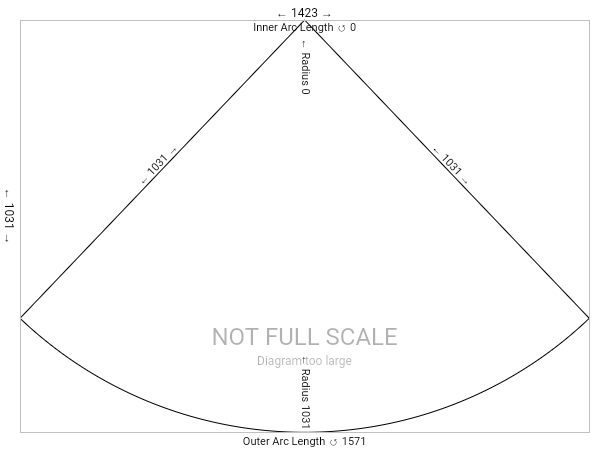
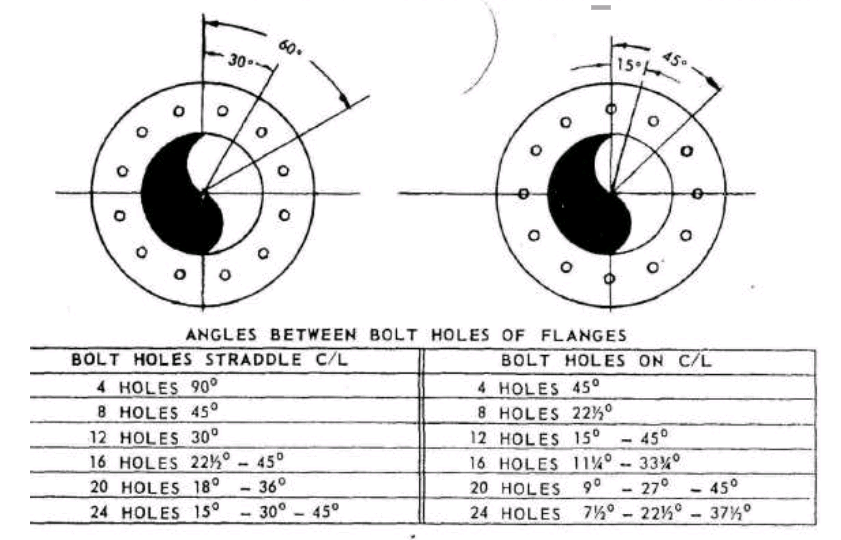
Piping isometric elbow degree calculation


یک استاد دانشگاه درباره اقدام اخیر متروی تهران نوشت: برگزاری مسابقه نامه خودمونی به خدا از سوی مترو کار خوبی است اما بهتر است در کنار این اقدامات که مسجد محل هم می تواند انجام دهد، بخش اجتماعی مترو به کارهای اصلی خود بپردازد. ایجاد نارضایتی و ناراحتی هنر نیست.


بکارگیری اتباع خارجی بدون پروانه کار در مشاغل حوزه سلامت از قبیل مواد غذایی و بهداشت و درمان (رستوران، آشپزخانه، درمانگاه، داروخانه و ...) ممنوع است.


معاونت اجتماعی و پیشگیری از وقوع جرم دادگستری استان تهران 


شروط غیرقانونی در قرارداد کار چه هستند؟

شروط غیرقانونی در قرارداد کار، به توافقاتی گفته می‌شود که برخلاف قوانین آمره کار تنظیم شده‌اند و حتی در صورت رضایت کارگر، فاقد اعتبار قانونی هستند. یکی از مهم‌ترین نمونه‌های این شروط، تعیین ساعت کاری بیش از ۴۴ ساعت در هفته است که با قانون کار مغایرت دارد. همچنین گاهی کارفرما برای خود حق فسخ یک‌طرفه قرارداد را با تعیین مدت زمان مشخصی، مانند ۴۵ روز، قائل می‌شود که این شرط نیز برخلاف اصول قانونی روابط کار است.

از دیگر مصادیق شروط غیرقانونی می‌توان به تبعیض‌های جنسیتی در مزایای شغلی اشاره کرد؛ برای مثال، محروم کردن کارکنان زن از دریافت حق اولاد یا حق تأهل، امری غیرقانونی محسوب می‌شود. در برخی قراردادها نیز توافق می‌شود که مبلغ عیدی کمتر از میزان تعیین‌شده توسط قانون پرداخت شود یا دستمزد کارگر کمتر از حداقل دستمزد مصوب وزارت کار تعیین گردد که هر دو مورد باطل و فاقد اعتبار هستند.


Slope 5/100

B=90 Degree

A=87.14 Degree


Distance : 505.18mm


سوالات تست مایعات نافذ ASNT


Developer types

Dry powder

method of application  : Dust/fog, dip 

Application sequence : After drying

Dwell time : 1/2 penetrant dwell to 4 h

Adv : Easy to use , Easy to remove ,Good for Type I 

Disadv : Not for Type II spray  , Parts must dry first ,

penetrant contaminated

dwell to Penetrant 4 h  

Water soluble

method of application  : Spray, flow , dip

Application sequence : Before drying 

Dwell time :  1/2 penetrant dwell to 2 h

Adv : Needs no agitation , Easy to remove , Applies thin coat

Disadv : Acts as detergent , Not for Method A , Not for Type II , Bacteria/fungus , Evaporation

 Water suspendible 

Method of application : Spray, flow, dip

Application sequence : Before drying

Dwell time : 1/2. Penetrant dwell to 2h

Adv : Visible'coating , Surface contact

Disadv : Critical immersion ,  Frequent agitation , Bacteria/fungus Difficult to remove

Nonaqueous 

Method of application : Spray

Application sequence : After drying

Dwell time : 10 min to 1 h 

Adv : Most sensitive , High contrast ,  Portable

Disadv :  Expensive , 

Type I and Type 11  Flammable ,  Not for large areas ,  Frequent agitation Parts must dry first


Typical equipment calibration

--White light meter

-Type 2 lighting/ambient light for Type 1 

-6 months

--Ultraviolet light meter 

-Ultraviolet light intensity

-6 months

--Refractometer

-Hydrophilic emulsifier concentration

-1 year


Typical process control requirements

--Lipophilic emulsifier water content 

-Method B 

-<5%

-Monthly

--Hydrophilic emulsifier concentration

-Method D

-immersion: < than specified on the AMS-2644 QPL, spray < 5% 

-Weekly


Water or moisture within crack discontinuities can prevent the liquid penetrant from entering the crack.


-If excess liquid penetrant is not removed, false indications are evident. On the other hand, washing too long and too hard can remove liquid penetrant from large or shallow discontinuities, resulting in less intense indications.


-Lack of cleanliness in the inspection area is often a cause of false indications


Developer

The developer makes indications more visible by:

1. providing a contrasting background,

2. pulling liquid penetrant out of openings by a blotting action,

3. making the indication easier to read by enlarging it as the penetrant spreads into the developer and

4. reducing glare چشم زنندگی from reflected light during observations of fluorescent indications.


-One disadvantage of liquid penetrant inspection is that:

a. penetrant materials may cause drying and cracking of the skin.

b. large subsurface discontinuities with openings to the surface will not form indications.

c. it can only be used with nonferrous material.

d. the materials are only available in aerosol spray cans.


-Which of the following is not a physical property associated with penetrant materials?

a. Solvent resistance.

b. Flash point.

c. Viscosity.

d. Chemical inertness.


-The removal of smeared metal by chemical processes is called:

a. grit or sand blasting.

b. machining.

c. etching.

d. quenching.


-A standard classification for a type of developer is:

a. water soluble.

b. water washable.

c. nonfluorescent.

d. solvent removable.


-Compared to a certified Level I inspector, a Level II inspector:

a. can process all forms of a product.

b. is authorized to approve all penetrant procedures.

c. requires more formal training hours and work experience.

d. can determine the acceptance criteria for a part.


-A limitation on materials used to inspect nickel alloy welds in a nuclear or pressure vessel system is that the penetrant materials should have:

a. sulfur and halogen residual of 10% or

less by weight.

b.sulfur, chlorine and fluorine residual of 1 % or less by weight.

c.chlorine and halogen residual of 5% or less by weight.

d.halogen and fluoride residual of 10% or less by weight.


-A weld discontinuity that appears starshaped with small indications emanating from a central point is a:

a. burst

b.grinding crack

c.crater crack

d.heat affected zone (HAZ) crack


-A relevant indication in a casting may be caused by:

a. a burst.

b. a crater crack.

c. laminations.

d. porosity.


-Discontinuities that may be found in aluminum extrusions are:

a. porosity and inclusions.

b. laminations.

c. cracks.

d. laps and seams.


-Ultraviolet lights over a fluorescent penetrant wash station are used to:

a. verify a uniform coating of penetrant has been applied to the part.

b. verify the emulsifier covers the entire surface.

c. monitor the removal of surface penetrant.

d. check the cleanliness of parts before processing.


-Dry developer is checked for fluorescent contamination by:

a. comparing the in-use developer to new material.

b. processing a testing and monitoring panel.

c. a laboratory examination for chemical composition.

d. viewing under an ultraviolet light for fluorescent specks.


-What comparison standard has control over the depth and quantity of cracks?

a. A stainless steel test panel.

b. A cracked aluminum test block.

c. A ceramic test block.

d. A grit blast panel


-Which of the following is not an advantage of postemulsifiable fluorescent penetrants?

a. High sensitivity level to detect very fine defects.

b. They are easily removed with water after proper emulsification dwell time.

c. They are easily removed from sand castings after proper emulsification dwell time.

d. They have higher tolerance to variations in the removal process when compared to water washable penetrants.


-When using the visible, solvent removable process, after the penetrant dwell time, excess penetrant is removed by:

a. spraying solvent on the part and then wiping with a clean, dry rag or paper towel.

b. wiping off excess penetrant with a clean, dry rag or paper towel, moistening the part with solvent and rewiping the part.

c. wiping off excess penetrant with a clean, dry rag or paper towel, moistening a clean cloth with solvent and rewiping the part.

d. wiping off excess penetrant with a clean, dry rag or paper towel, then rewiping with a cloth soaked with solvent.


-When using a fluorescent, postemulsifiable penetrant, the best emulsification time is:

a. 10 s.

b. 5 s.

c. 2 to 3 s.

d. determined by experimentation


-Which of the following is a advantage of fluorescent penetrants over visible type penetrants?
a.The inspection can be carried out in a well lighted area
b.Small indications are more easily seen 
c.They can be used where contact with water is objectionable
d.Less sensitive to contamination of discontinuities


-Emulsifier time:
a.Is important but not normally critical
b.The time needed to rinse the emulsifier and excess penetrant from the surface
c.Is extremely important and will greatly affect test results. (answer)
d.Should be as long as economically practical


-Which of the items listed below is NOT an advantage of the liquid penetrant test method?
a.The method can find all types of discontinuities
b.The method is simple in principle and relatively easy to understand.
c.The method is essentially simple in application.
d.There are few limitations on the size and shape of the article that can be treated by this method.

-When improper processing causes inspection difficulties, what should the inspector do?
a.Swab parts with a solvent
b.Use a correct bleed-back procedure
c.Erase non-relevant fluorescence
d.Reprocess the part


-When using post-emulsification penetrants, difficulties incurred during the washing operation can be overcome by:
a.Reapplying a coat of emulsifier
b.Increasing the water pressure used during the washing operation
c.Completely reprocessing the part from surface preparation on and by  using a longer emulsifier time.
d.Dipping the part in boiling water

-Developer assists in the detection of penetrants retained in the discontinuities by aiding the
a.Post cleaning process.
b.Emulsification process.
c.Bleed-out process.
d.Drying process.


-Difficulties with removal of a postemulsifiable penetrant during the rinse operation can be overcome by:

a. reapplying a coating of emulsifier.

b. using conditioned (soft) water during the washing operation.

c. cleaning, then completely reprocessing the part using a longer emulsification time.

d. increasing the water temperature during the washing operation. 


-Excessive removal of penetrant may result in:

a. undetected discontinuities during evaluation.

b. an excessive background that inhibits the evaluation process.

c. the need to apply the developer twice to obtain significant bleedout.

d. small, tight cracks that are easily detected on parts with a smooth surface.


-A penetrant inspection cannot find:

a. surface porosity.

b. surface cracks.

c. an internal cavity.

d. a surface forging lap.


-Which of the methods listed below is most applicable for detecting fine, tight surface cracks?

a. Visible dye, water washable.

b. Visible dye, postemulsifiable.

c. Fluorescent, water washable.

d. Fluorescent, postemulsifiable. 


-The term used to describe the total time that penetrant remains on the workpiece is:

a. immersion.

b. drain.

c. dwell.

d. presoak.


-Developer assists in the detection of discontinuities by:

a. providing a contrasting background.

b. emulsifying the penetrant bleedout.

c. providing a clean surface.

d. providing a dry surface.


multiple PQRs used to support a single WPS,


مدیران اماکن عمومی و صاحبان و متصرفان اماکن خصوصی موظف‌اند توقف اتباع خارجی را ظرف مدت 24 ساعت پس از ورود آنان، به مرجع انتظامی اطلاع دهند.


معاونت اجتماعی و پیشگیری از وقوع جرم دادگستری استان تهران


۲۲ بهمن ۱۴۰۳ : جراحی بدون جراح زیبایی در بیمارستان آپادانا ... مردم گوش به زنگ باشند
به گزارش خبرآنلاین،در بازرسی سرزده قاضی سعید احمد بیگی، سرپرست دادسرای ویژه جرائم پزشکی به همراه تیمی از پلیس و بازرسان وزارت بهداشت از یک بیمارستان خصوصی در قلب شهر تهران، ۷ تکنیسین هنگام جراحی زیبایی به جرم دخالت در امور پزشکی، مسئول اتاق عمل و ۲ پزشک به خاطر ترک فعل هنگام عمل و تخلف پزشکی و متخصص بی‌هوشی بازداشت شدند.


۲۳ ساعت پیش · در پی این کشف، سه اتاق عمل بیمارستان پلمب و ۷ تکنسین غیررسمی، دو جراح عمومی، متخصص بیهوشی و مسئول اتاق عمل به کلانتری منتقل شدند. به ادعای ...


KayhanLondon کیهان لندن ✓

Twitter › KayhanLondon

پلمب اتاق‌های عمل بیمارستان آپادانا؛ جراح می‌خوابید ( ؟؟؟!!! ) تکنیسین عمل قلب انجام می‌داد! رسانه‌های داخلی از پلمب اتاق‌های عمل بیمارستان آپادانا در تهران به علت تخلف صورت گرفته از سوی جراحان و تکنیسین‌ها در انجام عمل جراحی زیبایی خبر دادند. روزنامه «جوان» بدون اینکه نام بیمارستان…

Twitter • ۲۰ ساعت پیش


یک WPS متشکل از چندین فرآیند را می توان از PQR های مختلف ایجاد کرد، اما حداکثر ضخامت فلز پایه تحت پوشش این WPS نمی تواند از 2 برابر ضخامت باریک ترین کوپن آزمایشی استفاده شده برای هر PQR تجاوز کند و هر فرآیند نمی تواند بیش از 2 برابر ضخامت رسوب شده خود باشد.


ASME BPVC.IX-2021


QW-200.4 Combination of Welding Procedures.


(b) As an alternative to (a), a production weld may be made using a WPS that is supported by more than one PQR, provided the following conditions are met:

(1) All PQRs were qualified

(-a) with GTAW, SMAW, GMAW, FCAW, PAW, LBW, LLBW, or SAW, or combinations of these processes

(-b) on test coupons at least 1/2 in. (13 mm) thick

(2) Note (1) of Tables QW-451.1 and QW-451.2 shall apply to the WPS. The WPS may be used to deposit

(-a) root layers with the process or combinations of processes on one PQR for weld metal deposits up to 2t

(-b) fill layers with the process(es) on the other PQR(s) on base metal up to the maximum thickness qualified by the other PQR(s)


ASME INTERPRETATION : 

Interpretation Number : IX-04-18


A combination GTAW and SMAW WPS is supported by two PQRs. PQR A is welded with SMAW to join 1-1/2 in. (38 mm) thick plates with 1-1/2 in. (38 mm) of SMAW deposit. PQR B is welded with GTAW and SMAW to join 1/2 in. (13 mm) thick plates, with 1/8 in. (3 mm) of GTAW deposit, and 3/8 in. (10 mm) of SMAW deposit.

Question (1): Do PQRs A and B qualify the combination WPS for a base metal thickness range of 3/16 in. (5 mm) to 8 in. (200 mm) when impact testing is not required?

Reply (1): Yes.

Question (2): Do PQRs A and B qualify the combination WPS for a maximum deposited weld metal thickness of 1/4 in. (6 mm) for the GTAW process and 8 in. (200 mm) for the SMAW process?

Reply (2): Yes.

Question (3): When impact tests are performed for both PQRs with acceptable results, do PQRs A and B qualify the combination WPS for a base metal thickness range of 1/2 in. (13 mm) to 8 in. (200 mm) when impact testing is required?

Reply (3): Yes.


۲۴ بهمن ۱۴۰۳

معاون امور جوانان وزارت ورزش و جوانان گفت: در حال حاضر به ۲۰۵ مرکز همسریابی مجوز داده ایم و نظارت ها بر آن انجام می شود و هر گونه مشکلی داشته باشند، پاسخگو هستیم.


وی با تاکید بر اینکه فعالیت مراکز و سایت‌های همسریابی هیچ اشکالی ندارد و در تمام دنیا باب است، گفت: جوانان در این فضا می‌توانند با یکدیگر آشنا شوند و این طرح برای افرادی که به واقع دنبال ازدواج دائمی هستند، مطلوب است و هیچ اشکالی ندارد و زیر سوال بردن این قانون چندان درست نیست. افرادی هم که به دنبال سوءاستفاده در این سایت‌های همسریابی هستند، جاهای مختلف به شکل غیر قانونی وجود دارد.


۲۵ بهمن ۱۴۰۳ · واکنش دانشگاه تهران به قتل یک دانشجو توسط سارقان زورگیر/ مطالبه‌ دانشجویان از پلیس؛ کیوسک نیروی انتظامی در اطراف خوابگاه‌ها مستقر شود


به گزارش خبرنگار ایرنا، تعدادی از دانشجویان عصر جمعه ۲۶ بهمن ماه در واکنش به ضرب، جرح و قتل دانشجوی کارشناسی رشته مدیریت کسب و کار دانشگاه تهران در محوطه کوی دانشگاه تجمع برگزار کردند.

در این تجمع دانشجویی که بیش از دوساعت و نیم به طول انجامید دانشجویان خواستار برقراری هرچه بیشتر امنیت کوی دانشگاه و دانشجویان شدند.


Radio Zamaneh

Twitter › RadioZamaneh

یک دانشجوی دانشگاه تهران به دست زورگویان خیابانی کشته شد سارقان در حین سرقت کوله‌پشتی او، با چاقو به وی حمله کرده و او را مجروح کردند. این دانشجو به دلیل شدت جراحات وارده به مجاری تنفسی، پنج‌شنبه ۲۵ بهمن در بیمارستان شریعتی تهران درگذشت. www.radiozamaneh.com…

Twitter • ۱۱ ساعت پیش


۲۸ بهمن ۱۴۰۳ · همزمان با تحویل محموله بمب ۱۸۰۰ تنی آمریکا به رژیم اسرائیل، وزیر خارجه آمریکا در دیدار با نتانیاهو محور مقاوت و ایران را تهدید کرد؛ در صورتی .


۱ اسفند ۱۴۰۳


رابرت کیوساکی (Robert Kiyosaki)، نویسنده پرفروش‌ترین کتاب «پدر پولدار، پدر فقیر»، از آغاز سال جاری نسبت به وقوع یک فروپاشی اقتصادی جهانی هشدار داده است.

او معتقد است در سال ۲۰۲۵ شاهد بزرگ‌ترین سقوط تاریخ بازارهای مالی خواهیم بود که می‌تواند از رکود بزرگ دهه ۱۹۳۰ نیز شدیدتر باشد.


Thickness Of Base Metal Qualified


۲۱ بهمن ۱۴۰۳ · پدر دانش‌آموزان جانباخته خطاب به وزیر آموزش و پرورش: نه تسلیت می‌خواهم، نه تبریک.


۲۱ بهمن ۱۴۰۳ ( الجولانی سرکرده گروهک تروریستی تحریر الشام )  ... گفته می‌شود که شرط باز بودن حرم زینب «خلوتی» آن است، و در صورت ازدحام جمعیت درها بسته و اجازه ورود زائران داده نمی‌شود.


QW-407.4 DELETED


A groove weld procedure qualification test coupon 1.5 in. thick was welded with the SMAW process using multiple passes of 1/2 in. max. thickness. The test coupon was given a subsequent post weld heat treatment exceeding the upper transformation temperature prior to the completion of mechanical testing.

Question: May this PQR be used to support the weld of partial penetration groove welds per QW-202.2(b) or weld repair and buildup welds per QW- 202.3(b) on base material thickness exceeding 1.65 in.?

Reply: No. Per QW-407.4, a procedure qualification test coupon receiving a post weld heat treatment in which the upper transformation is exceeded, the maximum qualified thickness for production welds is 1.1 times the thickness of the test coupon.


QW-202.2 Groove and Fillet Welds

(a) Qualification for Groove Full Penetration Welds. Groove‐weld test coupons shall qualify the thickness ranges of both base metal and deposited weld metal to be used in production. Limits of qualification shall be in accordance with QW-451. The thickness, t, of deposited weld metal in QW-451 shall be exclusive of weld reinforcement. WPS qualification for groove welds shall be made on groove welds using tension and guided‐bend specimens. Toughness tests shall be made when required by other Section(s) of the Code. The WPS shall be qualified for use with groove welds within the range of essential variables listed.

When dissimilar thickness test coupons are welded, the "Range of Thickness T of Base Metal, Qualified" in QW-451 shall be determined individually for each base metal in the test coupon. When the thicker test coupon is tapered to provide a thickness transition at the weld, the qualified range shall be based on the base metal thickness adjacent to the toe of the weld at the thinnest end of the transition. The test specimens for tensile and bend tests may be machined to the thickness required for the thinner base metal prior to testing.

(b) Qualification for Partial Penetration Groove Welds. Partial penetration groove welds shall be qualified in accordance with the requirements of QW-451 for both base metal and deposited weld metal thickness, except there need be no upper limit on the base metal thickness provided qualification was made on base metal having a thickness of 11/2 in. (38 mm) or more. When dissimilar thickness test coupons are welded, the provisions of (a) for dissimilar thickness test coupons shall be met.

(c) Qualification for Fillet Welds. WPS qualification for fillet welds shall be made on groove‐weld test coupons using test specimens specified in (a) or (b). These qualifi- cations may be used for welding all thicknesses of base metal for all sizes of fillet welds, and all diameters of pipe or tube in accordance with Table QW-451.4. Non pressure‐retaining fillet welds, as defined in other Sections of the Code, may as an alternate be qualified with fillet weld qualification tests. Tests shall be made in accordance with QW-180. Limits of qualification shall be in accordance with Table QW-451.3


QW-202.3 Weld Repair and Buildup. WPS qualified on groove welds shall be applicable for weld repairs to groove and fillet welds and for weld buildup under the following provisions:

(a) There is no limitation on the thickness of base metal or deposited weld metal for fillet welds.

(b) For other than fillet welds, the thickness range for base metal and deposited weld metal for each welding process shall be in accordance with QW-451, except there need be no upper limit on the base metal thickness pro- vided qualification was made on base metal having a thickness of 11/2 in. (38 mm) or more.


TEST COUPON IN PIPE AND MIN LENGTH


مدیران اماکن عمومی و صاحبان و متصرفان اماکن خصوصی موظف‌اند توقف اتباع خارجی را ظرف مدت 24 ساعت پس از ورود آنان، به مرجع انتظامی اطلاع دهند.


معاونت اجتماعی و پیشگیری از وقوع جرم دادگستری استان تهران


QW-302 TYPE OF TEST REQUIRED

QW-302.1 Mechanical Tests. Except as may be specified for special processes (QW-380), the type and number of test specimens required for mechanical testing shall be in accordance with QW-452. Groove weld test specimens shall be removed in a manner similar to that shown in Figures QW-463.2(a) through QW-463.2(g). Fillet weld test specimens shall be removed in a manner similar to that shown in Figures QW-462.4(a) through QW-462.4(d) and Figure QW-463.2(h).

All mechanical tests shall meet the requirements pre- scribed in QW-160 or QW-180, as applicable.

QW-302.2 Volumetric NDE.

When the welder or welding operator is qualified by volumetric NDE, as permitted in QW-304 for welders and QW-305 for welding operators, the minimum length of coupon(s) to be exam- ined shall be 6 in. (150 mm) and shall include the entire weld circumference for pipe(s), except that for small diameter pipe, multiple coupons of the same diameter pipe may be required, but the number need not exceed four consecutively made test coupons. The examination technique and acceptance criteria shall be in accordance with QW-191


QW-302.3 Test Coupons in Pipe.

For test coupons made on pipe in position 1G or 2G of Figure QW-461.4, two specimens shall be removed as shown for bend specimens in Figure QW-463.2(d) or Figure QW-463.2(e), omitting the specimens in the upper‐right and lower‐left quadrants, and replacing the root‐bend specimen in the upper‐left quadrant of Figure QW-463.2(d) with a face‐ bend specimen. For test coupons made on pipe in position 5G or6G of Figure QW-461.4, specimens shall be removed in accordance with Figure QW-463.2(d) or Figure QW-463.2(e) and all four specimens shall pass the test. For test coupons made in both positions 2G and 5G on a single pipe test coupon, specimens shall be removed in accordance with Figure QW-463.2(f) or Figure QW-463.2(g).

QW-302.4 Visual Examination.

For plate coupons all surfaces (except areas designated “discard”) shall be examined visually per QW-194 before cutting of bend specimens. Pipe coupons shall be visually examined per QW-194 over the entire circumference, inside and outside.


QW-304.1 Examination.

Welds made in test coupons for performance qualification may be examined by visual and mechanical examinations (QW-302.1, QW-302.4) or by volumetric NDE (QW-302.2) for the process(es) and mode of arc transfer specified in QW-304. Alternatively, a minimum 6 in. (150 mm) length of the first production weld(s) made by a welder using the process(es) and/or mode of arc transfer specified in QW-304 may be exam- ined by volumetric NDE.

(a) For pipe(s) welded in the 5G, 6G, or special posi- tions, the entire production weld circumference made by the welder shall be examined.

(b) For small diameter pipe where the required minimum length of weld cannot be obtained from a single pro- duction pipe circumference, additional consecutive circumferences of the same pipe diameter made by the welder shall be examined, except that the total number of circumferences need not exceed four.

(c) The examination technique and acceptance criteria for production welds shall be in accordance with QW-191.


هدف از صلاحیت جوشکار


هدف از احراز صلاحیت فردی که از فرآیند اتصال استفاده می کند، نشان دادن توانایی آن فرد برای تولید یک اتصال سالم و بی عیب  هنگام استفاده از یک روش مشخص است.


QG-103 PERFORMANCE QUALIFICATION

ASME BPVC.IX-2021

The purpose of qualifying the person who will use a joining process is to demonstrate that person’s ability to produce a sound joint when using a procedure specification.


VALVE


DBB ( double block and bleed )


شیر انسداد و تخلیه ...  با دو سطح نشیمن که در حالت بسته، در برابر فشار از دو سر شیر با وسیله ای برای هواگیری/تخلیه حفره بین سطوح نشیمن، آب بندی ایجاد می کند.


Downstream


سمتی از شیر که در آن هیچ فشاری وجود ندارد یا فشار کمتری وجود دارد


Actuator


محرک یک وسیله (یا مجموعه) مکانیکی برای باز کردن یا بستن شیر.


piggability


قابلیت یک شیر برای اجازه عبور نامحدود یک pig


Visual Testing Quiz


تقریظ واژه‌ای عربی مأخوذ از «قَرَظَ»، در لغت به‌ معنای مدح و ستایش است.


قَرِظَ قرظاً؛ مهترو ارجمند گردید بعدِ مذلت و خواری


۱۱ بهمن ۱۴۰۳ · محمد فضل هاشمی استاد فلسفه و الهیات در دانشگاه اپسالا می‌گوید قتل سلوان مومیکا در واقع به نحوی اعدام وی بود که بصورت زنده در رسانه‌های


Prior to welding, some typical action items requiring attentionby the visual inspector should includethe following:

(1) Review drawingsand specifications

(2) Check procedureand performance qualifications

(3)Establish holdpoints if required

(4) Establish documentationplan

(5) Review material documentation

(6) Examine basematerial

(7) Examine fitup and alignment

of joints

(8) Review storageof welding consumables


During welding, some typical action items requiring attention by those responsible for weld quality should include thefollowing:

(1) Check preheat and interpass temperatures

(2) Check conformance Specification (WPS) to Welding Procedure

(3) Examine weld root pass

(4)Examine weld layers


This alsoprovides a check to determineif adequate cleaning is being accomplished between passes. This may help toalleviate the occurrenceof slag inclusions in the final weld.


(5) Examine second side prior to welding Any of these factors, if ignored, could result in discontinuities that could cause serious quality degradation.


Critical joint root conditions may exist on the second side of a double-welded joint. This area should be examined after removal of slag and other irregularities. This is to assure that all discontinuities have been removed and that the contour of the excavation provides access for subsequent welding.


After Welding. Following welding, some typical action items requiring attention by the visual inspector should include the following:

(1) Examine weld surface quality

(2) Verify weld dimensions

(3) Verify dimensional accuracy صحت ابعادی

(4) Review subsequent requirements الزامات بعدی


Porosity is a cavity-type discontinuity formed by gas entrapment حبس گاز during solidification انجمادسازی  or in a thermal-spray deposit. The discontinuity formedis generally spherical and may be elongated. A common cause of porosity is contamination during welding.


piping porosity which is a form of porosity having a length greater than its width that lies approximately perpendicular to the weld face. Piping porosity may also be referred to as wormhole porosity.


Aligned Porosity

The pores may be spherical or elongated. Aligned porosity is sometimes referred to as linear porosity.


Undercut is generally associated with either improper welding techniques or excessive welding currents, or both.


Incomplete fusion the result of improper welding techniques, improper preparation of the base metal, or improper joint design 


Incomplete joint penetration may result from insufficient welding heat, improper joint design (e.g., thickness the welding arc cannot penetrate),or improper lateral control of the welding arc 


Underfill is a conditionin which the weld face or root surface of a groove weld extends below the adjacent surfaceof the base metal. It results from the failure of the welder to completely fill the weld joint. 


Overlap is the protrusion of unfused weld metal beyond the weld toe or weld root. Overlap is a surface discontinuity that forms a mechanical notch and is nearly always considered rejectable. Two common causes of overlap may be insufficient travel speed and improper preparation of the base metal


Seams and laps are base metal discontinuities that may be found in rolled , drawn , and forged products. They differ from laminations in that they appear on the surface of the worked product . While seams and laps are surface discontinuities, they may only be detected after fabrication operations suchas bending, rolling, or sand blasting. Welding over seams and laps can cause cracking, porosity, or both


Crack

Cold cracks develop after solidification iscomplete. In carbon and low-alloy steels, cold cracks can occur in either the weld metal, heat-affected zone , or base metal , and are usually the result of dissolved hydrogen. The cracks can form hours or even days after the weldis completed. Cold cracks propagate both between grains and through grain.


Root cracks are longitudinal cracks at the weld root or in the root surface. They may be hot or cold cracks.


Excessive Reinforcement. In groove welds, weld reinforcement isweld metal in excess of the quantity required to fill a joint.Weld reinforcement can be located at either the weld face or weld root surface, and is called face reinforcement and root reinforcement, respectively


1-A visual examiner could expect to find a crater crack:

a. at the beginning of the weld

b. somewhere between the beginning and the end of the weld

c. at either the beginning or the end of the weld

d. at the end of the weld


2-During a visual examination, a welding discontinuity that could not be detected would be:

a. undercut

b. cracks

c. porosity

d. side wall lack of fusion


3-A discontinuity associated with metal overflow during forging is called a:

a. seam

b. flake

c. lap

d. lamination


4-In accordance with SNT-TC-1A certification of visual NDT personnel is the responsibility of:

a. ASNT

b. the employer

c. the NDT Level III

d. an outside agency


5-The undesirable removal of material from contacting surfaces by mechanical action is refered to as:

a. corrosion

b. erosion

c. wear

d. grinding


6-The deterioration of a metal resulting from electrochemical reactions with environment is referred to as:

a. erosion

b. corrosion

c. wear

d. fatigue


7-Welding process in which there is a higher degree of probability of entrapping slag is:

a. GMAW

b. GTAW

c. SMAW

d. all of the above


8-A cause for undercut that occurs during the welding process is called:

a. excessive voltage or current

b. slow travel speed

c. excessive travel speed

d. both a and c above


9-When the weld is to be placed on the arrow side of the joint, the weld symbol in the drawing will be:

a. below the line

b. above the line

c. in the tail

d. at the end of the arrow


10-Joint profiles of finished welds are controlled by:

a. acceptance standards.

b. workmanship standards

c. design requirements

d. all of the above


PT QUIZ


-کندن کانال چندروز طول کشید؟

در مجموع ۵۵ روز کانال کندیم و در ۹ روز آخر فقط من و حسن رعیت بودیم که خوشبختانه توانستیم در یک عملیات بیش از ۲ هزار نفر اسیر کنیم و به نوعی این ابتکار حفر کانال به ما کمک کرد و باعث پیروزی ما شد.

-آیا نکته‌ی پایانی دارید؟

فقط می‌خواهم بگویم که سختی‌ها و تلاش‌هایی که انجام دادیم همیشه در یاد و خاطر ما خواهد ماند و نگارش کتاب‌هایی مانند معبد زیرزمینی می‌تواند این ماندگاری را دنبال کند.


بهمن ۱۴۰۳

در شرایطی که اقتصاد کشور با چالش‌های متعدد دست‌وپنجه نرم می‌کند، دو مسئله‌ی مهم "عدم کفایت دستمزدها" و "کمبود نیروی کار" ( نظرخودم :  اشتباه بزرگ در اخراج افاغنه ) به‌طور فزاینده‌ای در حال گسترش است. این وضعیت نه‌تنها معیشت خانوارها را تحت تأثیر قرار داده، بلکه در بخش‌های مختلف تولید و خدمات نیز بحران ایجاد کرده است.

آمارهای میدانی به راحتی نشان می دهد که بسیاری از کارگران و کارمندان بر این باورند که دستمزدهای فعلی توان تأمین هزینه‌های زندگی را ندارد ( نظر خودم :  پس علت تولد نوزادهای جدید در این تورم چیست ؟  احتمالاً بخاطر دفاع از کشور در آینده ). تورم روزافزون و افزایش قیمت کالاهای اساسی باعث شده که حتی اقلام ضروری از دسترس بخش قابل‌توجهی از جامعه خارج شود. کارگران می گویند با این حقوق‌ها نمی‌توان زندگی کرد. هزینه اجاره خانه، آموزش فرزندان و خوراک هر روز بیشتر می‌شود، اما حقوق ما ثابت مانده است.


غفاری ( تامین احتماعی )  اظهار کرد: کارگر را سخت و زیان آور اعلام کردند، هیچ کجای دنیا به اندازه کشور ما بازنشسته سخت و زیان آور ندارد، و بسیاری از افراد در سنین جوانی ۳۵، ۴۰ و ۴۵ سال بازنشسته شدند.


Liquid penetrant inspection is a nondestructive testing method used to detect surface defects in materials. In this process, a liquid penetrant is applied to the surface of the material and allowed to seep رسوخ کند into any surface defects. To ensure effective penetration, the liquid must have a low surface tension. Low surface tension allows the liquid to spread evenly over the surface and penetrate into small cracks and defects. Therefore, a low surface tension is an important requirement for the liquid used in liquid penetrant inspection.


Advantages of the Penetrant Process

The following are advantages of the liquid penetrant process:

1. very small surface discontinuities can be detected,

2. a wide variety  of materials can be tested,

3. complex geometrical shapes can be inspected in a single operation,

4. various sensitivities and processing methods are available,

5. it is relatively easy to use,

6. it can be portable

7. when compared to other testing methods, it has a low cost.


Disadvantages of the Penetrant Process
The following are disadvantages of the liquid penetrant process:
1. porous materials cannot be tested
2. surfaces must be clean and free of paint, coatings, soil, moisture and contaminants
3. it cannot be used following metal smearing operations such as shot peening, sand blasting, certain machining operations (unless material is acid etched to remove smeared metal)
4. some materials (rubber and plastics) may be adversely affected by the penetrant's petroleum base;
5. it is very dependent on operator skill
6. some penetrant products use ingredients that may cause skin irritation under prolonged contact if proper protective clothing is not worn.


If a system is too sensitive, the results may be misleading ( گمراه کننده ) and time will be wasted ( تلف شود ) in the evaluation process. If the system is not sensitive enough, rejectable defects could remain undetected.


The sensitivity of a liquid penetrant system refers to its capability to detect small defects. This means that a highly sensitive system can identify even the smallest flaws عیوب  or imperfections in the material being tested. Contrast ratios and color intensity may contribute to the system's effectiveness, but the primary factor determining sensitivity is its ability to detect small defects. The frequency of black-light used is not mentioned in the question and therefore cannot be considered as a factor in determining sensitivity.


The tendency تمایل of a liquid penetrant to enter a discontinuity is primarily related to the capillary forces. where a liquid can be drawn into narrow spaces or tubes against the force of gravity. In the case of liquid penetrant testing, capillary forces allow the penetrant to flow into small cracks or defects in a material, making them visible during the inspection process. 


Liquid penetrant testing is a nondestructive testing method used to detect surface discontinuities in materials.  allowing it to seep into any surface cracks or defects, and then removing the excess penetrant. The penetrant is typically brightly colored to make it visible under UV light. However, liquid penetrant testing is not capable of accurately measuring the depth of a crack or discontinuity. It can only detect the presence of surface defects, making it more suitable for finding shallow surface discontinuities rather than measuring the depth of cracks.


it is important to avoid using penetrants containing sulphur and chlorine on nickel surfaces to maintain their integrity and prevent any potential harm.


A water tolerance test is used to determine how much water a postemulsifiable penetrant or a hydrophilic emulsifier can tolerate before becoming unusable. This test helps to establish the maximum amount of water that can be present in the penetrant or emulsi¦er without affecting its effectiveness. By conducting this test, one can ensure that the penetrant or emulsifier is able to withstand مقاومت a certain level of water contamination آلودگی آب and still perform its intended function عملکرد موردنظر.


Contact angle is determined by the balance between the adhesive forces between the liquid and the surface, and the cohesive forces within the liquid. A high contact angle indicates that the liquid is less likely to spread out on the surface, while a low contact angle indicates that the liquid will spread out more easily. The contact angle is important in various applications, such as determining the wettability of a surface or understanding the behavior of liquids on different materials


The ability of the penetrant to enter the discontinuity is based on surface tension; however, the speed at which it enters is determined by viscosity.


A hydrometer is used to measure the specific gravity of a liquid. It works based on the principle that the density of a liquid is directly proportional to its specific gravity. The hydrometer is a cylindrical glass tube with a weighted bulb at the bottom. When placed in a liquid, it floats and the level at which it sinks indicates the specific gravity of the liquid. Therefore, a hydrometer is the correct tool for checking specific gravity.


Immersion dwell is a technique used in non-destructive testing where the test part is immersed in a liquid medium for a prolonged period. This method is employed when there is a need for extended dwell times to ensure thorough inspection. The other options mentioned, such as shallow and wide discontinuities and large numbers of test parts, do not specifically require the use of immersion dwell.


dilation of the pupils enables the operator to see better in the darkened environment and detect any visible dye penetrant indications. Therefore, a minimum of three minutes is required to allow the operator's eyes to fully dilate and achieve maximum seeing in the darkened inspection area.


Type of Penetrant

Penetrant can be fluorescent, visible or dual mode dye that has both visible and fluorescent properties


Fluorescent penetrant contains a dye that is visible under UV-A light. To view the indications, inspection is performed in a darkened area with an ultraviolet light source


Fluorescent penetrants have the advantage of being able to detect smaller indications more easily compared to visible dye penetrants. This is because fluorescent penetrants emit a bright glow under UV light, making even small indications more visible and easier to identify during inspection.


A black light filter is not necessary to activate the fluorescent penetrant dye because the dye is activated by the UV light emitted by the black light bulb itself. It is also not necessary to provide a contrasting background on the material surface as the black light already highlights any fluorescence present on the surface. Additionally, it is not needed to protect the black light bulb from scratches and breakage as this is not its purpose.


The black-light intensity is stated as a minimum of 1000 microwatts per centimeter squared in order to ensure that the fluorescent dye reaches its peak fluorescence. When the black-light intensity is at this level, it provides the optimal conditions for the dye to emit the brightest fluorescence, making it easier for the operator to detect any defects or irregularities on the material surface. This level of intensity ensures that the dye is fully activated and visible, allowing for accurate inspection and evaluation.


Visible penetrant uses a red, orange or purple dye that is highly visible when contrasted against a white developer coating the part surface. Inspection must be performed under white light.


Type I : Advantages of Fluorescent Liquid Penetrants

fluorescent liquid penetrant testing is more sensitive to small discontinuities than visible dye.


Advantages of Visible Dye Penetrants

It does not require a darkened area or a source of electric power for illumination ( روشنایی ). For this reason, it is more often used as a portable testing tool in the shop or field


Disadvantages of penetrant Type : 

-Type I , Fluorescent : 

--Requires special lighting

--Requires electricity

-Type II , Visible Dye

--Less sensitive than Type I

--Does not perform well for wide, shallow discontinuities


Penetrant class is not divided into performance grades as is fluorescent liquid penetrants.The visibility of the indications with respect to the white developer background is a key factor in successfully revealing tight discontinuities


زمان ماندگاری ماده نافذ روی قطعه مورد آزمون

Penetrant Dwell

The total time the penetrant remains on the part surface is the penetrant dwell. The time required for a penetrant to enter a discontinuity is dependent on temperature, the type of discontinuity and the possibility of contaminants entrapped within discontinuities. Large, shallow discontinuities require less dwell time than small, tight cracks. Discontinuities free from contaminants require less dwell time than discontinuities with entrapped soil because it is easier for the penetrant to enter them.


The standard minimum dwell is 5 min unless testing in service parts. If service fatigue cracks are suspected, the minimum dwell time required is often 2 h, but for stress corrosion up to 4 h may be required. When the dwell exceeds 1 h, applying fresh penetrant every hour improves the rate of penetration.


Temperature

The temperature of the penetrant materials and the part must be within an acceptable range for processing. ASTM E 1417 specifies a temperature range of 4 to 52 °C (40 to 125 °F).

The viscosity of most liquids, including penetrants, increases at low temperatures. If a part is quite cold, under 16 °C (60 °F) for example, the liquid penetrant may become chilled and thickened when applied, making the dwell time for very fine discontinuities longer than for parts at higher temperatures. If a part or liquid penetrant is too hot, the volatile components of the liquid penetrant may evaporate, changing the ability for revealing small discontinuities. Material temperatures from 10 to 52 °C (50 to 125 °F) produce optimum results with conventional liquid penetrants,


Most industry and military specifications limit acceptable water temperature to 10 to 38 °C (50 to 100 °F) at a pressure not to exceed 276 kPa (40 psi). The spray nozzle should be a minimum of 30 cm (12 in.) from the part at an angle between 45 and 70 degrees.


روش حذف ماده نافذ اضافی

Penetrant Removal Method

Excess penetrant is removed by water wash, hydrophilic emulsification, lipophilic emulsification, or solvent wipe.

The penetrant must be removed from the part surface without removing it from within a discontinuity. An optimum amount of removal must be obtained. Too little removal will cause an excessive penetrant background and indications will be indistinguishable from the part surface. If too much is removed from the discontinuity, a weak indication or no indication will be formed. The methods for removing surface penetrant and the SAE AMS 2644 designation are:

1. Method A - Water Washable

2. Method B - Lipophilic Emulsifier

3. Method C - Solvent Removable

4. Method D - Hydrophilic Emulsifier

Fluorescent penetrant should be removed in a darkened area equipped with ultraviolet lighting regardless of the removal method.


Water Washable (Method A)

Water washable penetrants contain emulsifying agents that make the oil miscible (mixable) with water. The penetrant may be removed with a manual or automatic coarse water spray, by immersion in an air agitated water wash or by manually wiping.


The rinsing operation must be monitored closely to avoid overwashing. Washing should be stopped as soon as an acceptable background level is observed.


Lipophilic Emulsifier (Method B) چربی دوست

Removal is performed by introducing an oilbased emulsifier as a separate process step. Lipophilic emulsifier diffuses in to the surface penetrant. It is usually applied by immersion; brushing or wiping may cause streaking due to uneven emulsification and are not recommended. This system offers more control and has fewer problems with over and under washing compared to the water washable method. The emulsifier dwell may be anywhere between 5 s up to 5 min.


ASTM E 1417 limits lipophilic emulsifiers to a 3 min maximum dwell time. Finding the optimum time for specific conditions is generally accomplished through experimentation. Experience under similar circumstances related to the type and size of suspected defects, surface roughness of the part, temperature of materials, water contamination levels of the penetrant and emulsifier can be used for a guideline. If the emulsification time is either too short or too long, the part must be entirely cleaned and reprocessed with an adjusted emulsifier dwell.

Following the appropriate dwell, the part should be quickly sprayed with water wash to stop the diffusion process. Once the diffusion process is halted, the emulsified penetrant is rinsed using the same methods as the water washable method.


The postemulsification test is used to detect defects or cracks in materials by applying a penetrant, emulsifying it, and then removing the excess. If the emulsifying time is too long, it can cause the penetrant to be completely removed from the cracks or defects, rendering the test ineffective as it will not be able to detect any flaws عیوب

تست را بی اثر می کند زیرا قادر به تشخیص هیچ نقصی نخواهد بود


Having an ultraviolet light installed at the wash station allows for the inspection of parts without the need for drying. This is because ultraviolet light can reveal any fluorescent dye penetrant that may be present on the parts. By using the ultraviolet light, one can determine if the wash cycle has been effective in removing any remaining dye penetrant from the parts. This helps ensure that the parts have been properly cleaned and prepared for further processes or use.


emulsifier time is extremely important and will greatly affect test results. This implies that the amount of time the emulsifier is allowed to act on the surface has a significant impact on the outcome of the test. The longer the emulsfier time, the better the results are expected to be.


Solvent Removable (Method C)

Solvent remover is usually supplied in aerosol spray cans. The solvent works by diluting the surface penetrant. The part is first wiped with clean, dry, lintfree cloths or towels. After the major portion of penetrant has been wiped from the surface, the surface should be wiped with a clean cloth, lightly sprayed with solvent, until just a trace of penetrant is observed on the cloth. Extreme caution must be used to avoid excessive removal.


Using an excessive amount of solvent when using a solvent-removable penetrant can have negative effects. It can lead to excessive removal of the penetrant from the surface, making it difficult to detect any defects. This can result in false-negative results and compromise the effectiveness of the inspection process. Therefore, it is generally accepted that using an excessive amount of solvent should be avoided as a precautionary measure.


Water-soluble and water-suspensible developers also require the correct drying of the test parts after applying the developer to prevent streaking ( رگه شدن ) and running ( جاری شدن)  of the developer coating. 


Note: Flowchart shows parts being dried before dry powder and nonaqueous developer, but dried after water-soluble and water suspendable developer.


Developers : 


Dry developer is the most suitable developer for parts that are complex or have rough surfaces ,  Aqueous developer is a water-based developer that is more suitable for smooth surfaces, while non-aqueous developer is a developer that is not water-based and may not adhere as well to complex or rough surfaces.


Non-aqueous developers are typically solvent-based and have a higher sensitivity compared to dry and aqueous developers. They are able to detect smaller defects and provide higher contrast images. Dry developers are typically used for magnetic particle testing and do not provide as high sensitivity as non-aqueous developers. Aqueous developers are water-based and have lower sensitivity compared to non- aqueous developers. Therefore, the non-aqueous developer is the most sensitive option.


Non-aqueous->aqueous->dry


1-Difficulties with removal of a postemulsifiable penetrant during the rinse operation can be overcome by:

a. reapplying a coating of emulsifier.

b. using conditioned (soft) water during the washing operation.

c. cleaning, then completely reprocessing the part using a longer emulsification time.

d. increasing the water temperature during the washing operation.


2-Which of the following is an advantage of a fluorescent water washable penetrant system compared to a fluorescent postemulsifiable penetrant system?

a. Water washable is superior for testing critical in service parts.

b. Water washable has fewer processing steps.

c. Only wet developer may be used with postemulsifiable penetrants.

d. Water washable penetrants will more readily detect fine, tight cracks in weldments.


3-When using the visible, solvent removable process, after the penetrant dwell time, excess penetrant is removed by:

a. spraying solvent on the part and then wiping with a clean, dry rag or paper towel.

b. wiping off excess penetrant with a clean, dry rag or paper towel, moistening the part with solvent and rewiping the part.

c. wiping off excess penetrant with a clean, dry rag or paper towel, moistening a clean cloth with solvent and rewiping the part.

d. wiping off excess penetrant with a clean, dry rag or paper towel, then rewiping with a cloth soaked with solvent.


4-Which of the following is not an advantage of postemulsifiable fluorescent penetrants?

a. High sensitivity level to detect very fine defects.

b. They are easily removed with water after proper emulsification dwell time.

c. They are easily removed from sand castings after proper emulsification dwell time.

d. They have higher tolerance to variations in the removal process when compared to water washable penetrants


5-One method for applying dry developer to a localized area of a large part is with:

a. a brush.

b. a powder bulb.

c. an aerosol can.

d. an immersion tank.


6-Prewash and postwash stations are anadvantage when using which of the following penetrant methods?

a. Visible, lipophilic postemulsifiable.

b. Fluorescent, hydrophilic postemulsifiable.

c. Visible, water washable.

d. Fluorescen , lipophilic postemulsifiable.


7-The specific gravity of wet developer is measured with a:

a. developer gage.

b. hydrogage.

c. balance scale.

d. hydrometer.


8-Which of the following describes the comparator that is used to monitor the process performance of the penetrant system?

a. A panel with one half chrome plated containing five crack centers and the other half grit blasted.

b. A cracked aluminu m block with a groove in the center.

c. A chrome plated panel with fine cracks across the face to a depth equal to the plating thickness.

d. Ceramic coated block with fine cracks extending around the entire panel.


9-Ultraviolet light intensity is measured with:

a. a digital or analog UV-A meter.

b. a photographic light meter.

c. an infrared meter.

d. a standard white light meter.


10-What instrument is used to check hydrophilic emulsifier concentration?

a. A hydrometer.

b. A capillary fill barometer.

c. A centrifuge tube.

d. A refractometer.


11-An important difference between non water- washabIe penetrants and water-washabIe penetrants is that:

a. water-washabIe penetrants contain an emuIsifier whiIe non water- washabIe penetrants do not

b. the viscosity of the two penetrants is different

c. the coIor of the two penetrantsis different

d. non water-washabIe penetrants are more easiIy removed than water- washabIe penetrants


12-Which of the foIIowing characteristics ( ویژگی های زیر ) are normaIIy considered when seIecting the type of penetrant to be used a penetrant test?

a. removaI characteristics of the penetrant

b. the fIash point of the penetrant

c. the cost of the penetrant

d. aII of the above


13-Which materiaIs shouId be avoided in the penetrant system when testing titanium aIIoys?

a. carbon or oiI

b. haIogenated soIvents 

c. emuIsifier or oiI

d. fIuorescent agents


14-Which of the foIIowing is an advantage of visibIe dye penetrants over fIuorescent penetrants?

a. smaII indications are more easiIy seen

b.they can be used on anodized and chromate surfaces

c. they make Iess background on rough surfaces

d. no speciaI Iighting is required


15-Which of the foIIowing is an advantage of soIvent-wipe methods over water washing?

a. no speciaI Iighting is necessary during inspection

b. they provide a quicker penetration of smaII openings

c. smaII indications are more easiIy seen

d. they can easiIy be carried out in the fieId and to remote areas


16-The tendency (  تمایل ) of a Iiquid penetrant to enter a discontinuity is primariIy reIated to the:

a. viscosity of the penetrant

b. capiIIary forces

c. chemicaI inertness of the penetrant

d. specific gravity of the penetrant


17-The emuIsifier is used :

a. to wash the penetrant out of discontinuities

b. to aid in washing off the surface of parts when using either the water or soIubIe penetrants

c . to emuIsify the oiI-soIubIe penetrant, thereby making it water-washabIe

d. to pre-cIean parts before appIying penetrant


18-Why is it advisabIe to have a bIack Iight instaIIed at the wash soIution?

a. so inspection can be done without drying parts

b. to speed the bIeeding penetrant out of defects

c. to check the effectiveness of the wash cycIe

d. to determine if parts have been covered with penetrant


19-The prime purpose of the bIack Iight for fIuorescent penetrant inspection is to :

a. magnify indications

b. make the indication visibIe

c. develop indication

d. speed up inspections


20-AII of the foIIowing methods are recommended to remove grease from the surface of a penetratnt test specimen except:

a. vapor degreasing

b. aIkaIine cIeaning

c. cIeaning with soIvent-type materiaI

d. hot water rinsing


21-The penetrant indication for a coId shut on the surface of a casting wiII be a:

a. dotted or smooth continuous Iine

b. cIuster of smaII indications

c. rough deep indication

d. Iarge buIbous indication


22-When improper processing causes inspection difficuIties, what shouId the inspector do?

a. swap parts with a soIvent

b. use a correct bIeed-back procedure

c. erase non-reIevant fIuorescence

d. reprocess the part


23-Which of the foIIowing is most IikeIy to render the post-emuIsification test in effective?

a. the penetrant time is too Iong

b. the deveIoping time is too Iong

c. the emuIsifying time is too Iong

d. none of the above


24- Which of the statements below applies to the liquid penetrant method of testing ?

a. the penetrant test method is less flexible that the eddy current test method

b. the penetrant test method is less reliable that the magnetic particle method for finding surface defects in ferromagnetic materials

c. the penetrant test method will not detect fatigue cracks

d. the penetrant test method is more reliable that radiographic testing when attempting to defect minute surface discontinuities


25-Developer assists in the detection of the visible dye penetrant test indications by:

a. providing a clean surface

c. providing a dry surface 

d. emulsifying the penetrant bleed-out

b. providing a contrasting background


26-The purpose for using a developer on a test specimen is to

a. promote penetration of the penetrant

b. absorb emulsifier residues

c. absorb penetrant from discontinuities and to provide a contrasting background

d. help to dry the surface for better observation


27-Which of the following reasons best describes why excessive drying of a part should be avoided

a. the extra time required is wasted

b. the developer may lose its blotting ability

c. a reduction in resolution may result

d. the excess developer may be difficult to remove


28-Which of the following practices should be avoided when performing a penetrant test?

a. applying emulsifier by dipping the part in emulsifier

b. applying developer by spraying the part with developer

c. removel of water-washable penetrant with a water spray

d. applying emulsifier with a brush

Cause : Brushing the emulsifier on to the part is not recommended either because the bristles of the brush may force emulsifier into discontinuities, causing the entrapped penetrant to be removed.


29-Which of the following penetrant systems is generally considered to be the least ( کمترین ) sensitive?

a. water-washable , visible dye

b. solvent removable , visible dye

c.water-washable , fluorescent dye

d. post-emulsification , visible dye


30-A red against white background discontinuity image is most likely to be seen when:

c. fluorescent post-emulsification penetrants are used

a. dry developers are used

d. wet developers are used

b. visible dye penetrants are used


31-When using wet developer:

a. a thick layer of developer is better than a thin layer for showing very fine cracks

b. compressed air should be used to remove excess developer

c. a black developer will show better contrast than a white developer

d. a thin layer of developer is better than a thick layer for showing very fine ( ریز  )cracks


32-A serious loss of water in a wet developer mix or an excessive over-concentration of developer powder can cause:

a. a loss of fluorescenceduring the inspection operation

b. nonrelevant indications

c. cracking of the developer coating during the drying operation

d. none of the above


33-Which of the following statements does not apply to developers used during penetrant testing?
a. Developers are normally highly fluorescent
b. Some developers furnish a contrasting background during inspection
c. Developers absorb or blot the penetrant that remains in discontinuities after the excess penetrant has been removed
d. Non aqueous developers are better suited for detecting fine crack


34-In penetrant testing, the time period from developer application to inspection is often referred to as the:

a. emulsification

b. development time

c. dwell time 

d. none of the above


35-In penetrant testing, developers should be able to perform all of the following functions except:

a. blotting penetrant from discontinuities

b. aiding in providing an image of a discontinuity

c. adding fluorescence to penetrants

d. helping control bleedout


36-Penetrants may be classified or subdiyided by the method used to remove excess penetrant. Which of the following is a proper classification in accordance with this statement?

a. nonsolvent removable

b. vapor degreased

c. water-washable

d. brush remoyable


37-When drying parts during a penetrant test, the parts:

a. are normally dried at room temperature

b. are normally dried by a circulating hot-air dryer

c. should be dried in an oven set at a temperature of 54 oC (130 °F)

d. should be dried by cool forced air


38-When using dry developer, the drying operation isperformed:

a. immediately after removal of excess penetrant

b. before the inspection step

c. thoroughly

d. all of the above


39-A good penetrant must do all of the following exeept:

a. be able to readily penetrate very fine openings

b. evaporate very rapidly

c. be able to remain in relatively coarse openings

d. be easily removed from the surface after testing


40-Which of the following is a disadvantage of using the Iiquid penetrant testing method?

a. the liquid penetrant test method is adaptable to produetion inspeetion of small parts

b. liquid penetrant testing can locate fine cracks

c. the liquid penetrant test method is a relatively simple test method

d. the Iiquid penetrant test method is not effective at all temperatures


41-Cleaning of the part prior to penetrant inspection is:

a. not required

b. important because if the part is 110 t clean, the developer cannot be improperlyapplied

c. essential because surface contaminants may prevent penetrant from gaining access to discontinuities

d. required to eliminate possibility of showing nonrelevant indications


42-When using fluorescent water-washable penetrant, adequate rinsing of the part is assured by:

a. timing of finse cycle

b. scrubbing of part surface

c. rinsing under ultraviolet light

d. using high pressure air with water


43-Black light is considered to be in the range of:

a. Long wavelength ultraviolet

b. Short wavelength ultraviolet

c. Short wavelength infrared

d. 500 to 800


44-Black light used in penetrant testing has its peak at:

a. 5550 angstroms (555 nm)

b. 4850 angstroms (485 nm)

c. 4250 angstroms (425 nm)

d. 3650 angstroms (365 nm)


45-Both fluorescent and visible dye penetrants are identified by:

A. Dwell times

B. Viscosity

C. Method of application

D. Method of Removal


The method of removal can vary depending on the type of penetrant used and the specific application. It is an important factor to consider as it can affect the overall effectiveness and efficiency of the inspection process


46-Acids and chromates should not be left on the surface of parts that will be inspected with a water-washable fluorescent penetrant because:

a. They may prevent the penetrant from entering any discontinuities

b. They may reduce the bleed-out

c. They may kill the fluorescence of the penetrant 

d. They may produce non-relevant


47-The ability of a liquid to wet a surface is measured by contact angle, i.e. the angle between the liquid and the surface at the point of contact as the liquid advances. Good penetrants should have:

a. A very small contact angle

b. A very large contact angle

c. A contact angle of approximately 45 degrees

d. A contact angle greater than 90


A large contact angle would indicate poor wetting ability and limited penetration. 


48-Which of the following characteristics ویژگیهای does not apply to liquid penetrant testing?

A. This method can accurately measure the depth of a crack or discontinuity

B. This method can be used for on-site testing of large parts

C. This method can be used to ¦nd shallow surface discontinuities

D. This method can be made more or less sensitive using different penetrant


49-Which of the following is an advantage of fluorescent penetrants over visible dye penetrants?

A. The inspection can be carried out in a well-lit area

B. Smaller indications are more easily seen

C. They can be used where contact with water is objectionable

D. They are less sensitive to contamination of dicontinuities


50-Sulphur and chlorine found in penetrants are detrimental to:

A. Aluminum

B. Iron

C. Nickel

D. Both (a) and


51-Emulsifier time:

a. Is important but not critical 

b. Is the time needed to rinse the emulsi¦er and excess penetrant from the surface

c. Is extremely important and will greatly affect test

d. Should be as long as possible


52-When penetrant testing, the temperature of the test area should not be lower than:

A. 30 degrees Celsius

B. 65 degrees Celsius

C. 10 degrees Celsius

D. 5 degrees Celsius


If the temperature is too low, the penetrant may not flow properly and the defects may not be detected.


53-Which of the following is generally accepted as the most important precaution when using a solvent-removable penetrant?

a. Do not apply an excessive amount of emulsifier

b. Do not use insufficient rinse pressure

c. Do not use excessive amount of solvent

d. Both (b) and (c)


54-Contact angle relates to:

a. The temperature at which a liquid will ignite and burn when exposed to an open §ame

b. The angle of the water spray nozzle for removing liquid penetrant

c. The angle at which a liquid sits on a material surface

d. None of the above


55-sensitivity of a liquid penetrant system is determined by:

A. Contrast ratios

B. Colour intensity

C. Ability to detect small defects

D. Frequency of black-light used


56-Which of the following developers is most suitable for parts that are complex or have rough surfaces?

A. Dry developer

B. Aqueous developer

C. Non-aqueous developer

D. None of the above


57-Wich of the following developers is the most sensitive?

A. Dry developer

B. Aqueous developer

C. Non-aqueous developer

D. None of the above


58-The most important property that enables the penetrant to enter into a discontinuity is:

A. Flash point

B. Penetrability

C. Viscosity

D. Surface tension


59-Dark adaptation is stated by most codes as a minimum of three minutes. Why?

a. To allow the operator's eyes time to contract for maximum seeing in the darkened inspection area

b. To allow the operator's eyes time to dilate for maximum seeing in the darkened inspection area

c. To allow the operator's eyes time to expand for maximum seeing of visible dye penetrant indications

d. To allow the operator's eyes time to contract for maximum seeing of §uorescent dye penetrant indications


60-Black-light intensity is stated as a minimum of 1000 microwatts per centimeter squared. Why?

A. To provide adequate visible light in the darkened viewing booth

B. The assist the operator when removing excess §uorescent penetrant from the material surface

C. To cause the §uorescent dye in the penetrant to "glow"

D. To ensure the fluorescent dye reaches its peak fluorescence 


61-The function of an emulsifier is to:

a. Help the penetrant enter a discontinuity by reducing the penetrant's surface tension

b. Mix directly with a fluorescent penetrant to increase its fluorescence 

c. Render the excess post-emulsifiable penetrant water- washable

d. Blot the penetrant back to the surface to produce an indication


62-Pre-cleaning in PT refers to:

a. Ensuring that the surface of the material is free of contaminants

b. Ensuring the penetrants are free of contaminants

c. Ensuring that a discontinuity is free of contaminants آلودگی

d. Both (a) and (c)


63-Dwell time is : 

a. The length of time the emulsifier is left on a material surface

B. The length of time a developer is left on a material surface

c. The length of time a penetrant is left on a material, to enter into a near-to-surface discontinuity

d. None of the above


64-The physics that enables the penetrant to enter into a discontinuity is called:

A. Caterpillar force

B. Gravitational force

C. Capillary force

D. None of the above


-The most important factor which determines the speed penetrant enters a discontinuity is based on viscosity.

A. True

B. False


-The amount of white light in a darkened inspection area must not exceed 2 ftc

A. True

B. False


-Developing time is a minimum of one-half of the penetrant dwell time.

A. True

B. False


نمیدانی نظر بازی گناهست
ز ما تا قبر چهار انگشت ر اه است
تو می گویی قیامت هم شلوغ است؟
تمام حرف ملاها دروغ است؟
تمام مجتهدها حرف مفتند؟
همه بی غیرت و گردن کلفتند؟
برو یک روز بنشین پای منبر
مسایل بشنو از ملای منبر
شب اول که ماتحتت درآید
به بالینت نکیر و منکر آید
چنان کوبد به مغزت توی مرقد
که ... به سنگ روی مرقد!


Wire IQI


۱۳ بهمن ۱۴۰۳  ... ظریف برکنار و محاکمه شود. اما در تجمع مشهد، مشخص شد ظریف در یک دادگاه صحرایی محاکمه و به اعدام، حبس و محرومیت از حقوق اجتماعی محکوم شده است.


According to my calculation, as per asme sec v table t-276,
Film side Wire iqi for 10mm job thick - wire no is 6.

Wire no 6 is 0.25 thk , hence, sensitivity = 0.25 X 100 /(10+3 Reinforcment ) , so sensitivity is 1.9% arrived.

Sensitivity should be less the 2% : 


1.8 minimum for single film viewing for radiographs made with an X-ray source

2.0 minimum for radiographs ( فیلم ها )  made with a gamma ray source


Article 2

T-234 Facilities for Viewing of Radiographs

Viewing facilities shall provide subdued background lighting of an intensity that will not cause troublesome reflections, shadows, or glare on the radiograph. Equip- ment used to view radiographs for interpretation shall provide a variable light source sufficient for the essential IQI hole or designated wire to be visible for the specified density range. The viewing conditions shall be such that light from around the outer edge of the radiograph or coming through low-density portions of the radiograph does not interfere with interpretation.


T-276.2 Size.

The designated hole IQI or essential wire shall be as specified in Table T-276. A thinner or thicker hole-type IQI may be substituted for any section thickness listed in Table T-276, provided an equivalent IQI sensitivity is maintained. See T-283.2.

(a) Welds With Reinforcements. The thickness on which the IQI is based is the nominal single-wall thickness plus the estimated weld reinforcement not to exceed the maximum permitted by the referencing Code Section. Backing rings or strips shall not be considered as part of the thickness in IQI selection. The actual measurement of the weld reinforcement is not required.

(b) Welds Without Reinforcements. The thickness on which the IQI is based is the nominal single-wall thickness. Backing rings or strips shall not be considered as part of the weld thickness in IQI selection.


When the density limits of T-282.2 cannot be met with one IQI, and the exceptional density area(s) is at the interface of the weld metal and the base metal, the material selection for the additional IQIs shall be based on the base material and be in accordance with T-276.1.


T-282 Radiographic Density

T-282.1 Density Limitations. The transmitted film density through the radiographic image of the body of the appropriate hole IQI or adjacent to the designated wire of a wire IQI and the area of interest shall be 1.8 minimum for single film viewing for radiographs made with an X-ray source and 2.0 minimum for radiographs made with a gamma ray source. For composite viewing of multiple film exposures, each film of the composite set shall have a minimum density of 1.3. The maximum density shall be 4.0 for either single or composite viewing. A tolerance of 0.05 in density is allowed for variations between densitometer readings.

T-282.2 Density Variation

(a) General. If the density of the radiograph anywhere through the area of interest varies by more than minus 15% or plus 30% from the density through the body of the hole IQI or adjacent to the designated wire of a wire IQI, within the minimum/maximum allowable density ranges specified in T-282.1, then an additional IQI shall be used for each exceptional area or areas and the radiograph retaken. When calculating the allowable variation in density, the calculation may be rounded to the nearest 0.1 within the range specified in T- 282.1.

(b) With Shims. When shims are used the plus 30% density restriction of (a) above may be exceeded, provided the required IQI sensitivity is displayed and the density limitations of T-282.1 are not exceeded


PIPING-NDT


پسر قاضی مقیسه در صفحه شخصی خود در فضای مجازی نوشت: حاجی دو بار برای عمل جراحی نیروی خدماتی (قاتل منافق) از همه قضات پول جمع کرده بود. ولی طرف به بهانه عمل رفته بود آموزش ترور.


۲ اردیبهشت ۱۳۹۷ · ... آبدارچی، عامل سازمان مجاهدین خلق باشد. روزی که مشخص شد عامل ... های سیاسی فرهنگی و اقتصادی سرمایه گذاری شده بلکه به انحا مختلف روی 


آبدارچی نفوذی از x.com
۲۹ دیماه ۱۴۰۳  مراقب آبدارچی های نفوذی در حکمرانی کشور باشید! آبدارچی هایی که سالها برایتان #چای_دبش آورده اند خود را خدمتگزار شما معرفی می‌کنند، اما 


۳۰ دیماه ۱۴۰۳  محسن مهدیان از رسیدن ترور به ایستگاه بلوغ گفت و نوشت: ممکن است سراغ مقیسه‌ها و رازینی‌ها بروند، اما هدف نهایی و فراترشان اثر ذهنی و ادراکی بر .


نام یکی از روش های رادیوگرافی است، برا ی لوله هایی با قطر خارجی ۸۹ ( ۳ اینچ )  و  کمتر، که اجرا ی آن به صورت سه عدد فیلم با زاو یه های تابش ۱۲۰ یا ۶۰ درجه می باشد و هر فیلم دارای دو تصویر جوش روی هم افتاده قابل تفسیر است ؟

۱-Panoramic

۲- Composite Viewing

۳-Ellipse 

۴-Superimposed


کدام یک از فولادهای آلیاژی زیر ساختار دو فازی ( فریت و آستنیت ) دارد؟

۱-Duplex

۲-Alloy

۳-Incoloy

۴-Hastelloy


کدامیک از عبارات زیر در کد ها و استانداردهای پروژه ها ، بیانگر یک شرط الزام آور اجباری است.

۱-Shall

۲- Should

۳-May

۴-Can

۵- Will


چنانچه توافقی بین خریدار و فروشنده نباشد، حداقل و حداکثر تغییرات مجاز در وزن لوله های متریال ASTM A106 با مقادیر مندرج در استاندارد چقدر است ؟

۱-نباید اختلافی داشته باشد.

۲-به اندازه ی ۱۲.۵ درصد حداقل و حداکثر مجاز است.

۳-بستگی به ضخامت و سایز لوله دارد

۴-حداقل ۳.۵ درصد و حداکثر ۱۰ درصد اختلاف در وزن مجاز است


پیشنهاد شما برای جوشکاری متریال استنلس سری 300 با متریال پایه نیکل N02200 ۲۰۰ در فرآیند SMAW کدام گزینه است.

۱- EniCrFe-2 or ENiCrFe-3

۲- Eni-1

۳- EniCiMo-10

۴- گزینه اول و دوم 


الکترود ENi-1 یک الکترود پایه نیکلی جهت جوشکاری به روش الکترود دستی (SMAW) بوده که برای اتصال نیکل خالص و همچنین برای اتصال فلزات غیرهمجنس مانند نیکل به فولاد بکار میرود.


برای جوشکاری  فیتینگ به فیتینگ  متریال A234-WPB و A234-WP11 Cl.1 کدامیک از فیلر و الکترودهای زیر را پیشنهاد می کنید؟ P-No.1 to P-No.4

۱- ER80S-D and E7018-B2

۲- ER80S-B2 and E8018-B2-H4R

۳- ER70S-6 and E7018

۴- ER90S-B3 and E8018-G


برای جوشکاری اتصال ورق مخزن استنلس استیل با متریال A240 TP-309S با فرآیند SMAW کدامیک از الکترودهاب زیر را می توانید پیشنهاد کنید ؟  P-No.8

۱- بدلیل اینکه متریال استنلس استیل است، نباید به روش SMAW جوش شود و از فرآیند GTAW باید استفاده کرد.

۲- E309L-16

۳ - E308L-16

۴ - E347-16


برای جوشکاری لوله به لوله متریال A335-p22 در فرآیند جوشکاری GTAW کدامیک از فیلرهای زیر را پیشنهاد می کنید.

۱- ER90S-G

۲- ER80S-G

۳- ER80S-Ni1

۴- ER80S-Ni2


A335-P22 : 2.5Cr-1.1Mo


برای جوشکاری متریال Carbon-molybdenum steel با فرآیند SMAW کدام یک از اکترودهای زیر را پیشنهاد می کنید؟

۱- E7018-A1

۲- E7018-B2L

۳- E8018-B3L

۴- E8018-B6


حداقل دمای طراحی متریال های پایپینگ آستنیتی کروم - نیکل مانند A312-TP 304L فارغ از بحث سیال و ضخامت  که نیاز به تست ضربه نداشته باشند ، چقدر است؟

۱- ۹۶F-

۲- ۳۲۵F-

۳- ۴۲۵F-

۴- ۶۹F-


آیا متریال های استنلس استیل آستنیتی کروم-نیکل مانند TP304 یا TP316 که دمای طراحی ( MDMT ) آنها برابر ۱۹۶- درجه سانتیگراد  و گرمتر باشند مطابق با ASME VIII نیاز به تست ضربه دارند؟

- تست ضربه در این دما و متریال ضروری است

- نیاز به تست ضربه ندارند


فرق لوله های Seamless و Welded به ترتیب چیست ؟

۱- بدون درز هستند و جوش طولی ندارند ، درزدار و دارای جوش طولی هستند

۲- درزدار هستند و جوش طولی دارند ، بدون درزدار و دارای طول جوشی نیستند

۳- بدون درز و مخصوص پایپینگ هستند ، درزدار و در خط لوله بکار می روند.

۴- به طول ۶ متر تولید می شوند ، به طول ۱۲ متر تولید می شوند.


تفاوت متریال استنلس استیل تیپ ۳۱۶ و ۳۰۴ از نظر آنالیز شیمیایی کدامیک از موارد زیر است ؟

۱- تیپ۳۱۶ دارای ۲ تا ۳ درصد مولیبدن  است ولی ۳۰۴ این عنصر را ندارد.

۲- تیپ ۳۱۶ دارای ۰.۰۸ درصد کربن و  درصد منگنزاست ولی ۳۰۴ درصد کمتری از این عناصر را دارااست.

۳- تیپ ۳۱۶ فسفر و سولفور بیشتری نسبت به ۳۰۴ دارد.

۴- اختلاف آنها در مقدار سیلیکون موجود است ، سیلیکون ۳۱۶ دوبرابر سیلیکون ۳۰۴ است.


304 contains 18% chromium and 8% nickel while 316 contains 16% chromium, 10% nickel and 2% molybdenum. The molybdenum is added to help resist corrosion to chlorides (like sea water and de-icing salts)


برای جوشکاری متریال استنلس استیل تیپ ۳۰۴ به ۳۰۴ کدامیک از الکترودهای زیر را پیشنهاد می کنید ؟

۱- E304-XX Or E304L-XX

۲- E309-XX Or E309L-XX

۳- E308-XX Or E308L-XX

۴- E310-XX Or 310L-XX


برای جوشکاری متریال استنلس استیل تیپ ۳۰۴ به ۳۱۶ کدامیک از الکترودهای زیر را پیشنهاد می کنید ؟

۱- E308-XX Or E308L-XX

۲- E309-XX Or E309L-XX

۳- E316-XX

۴- گزینه اول و سوم


مشخصات الکترود و فیلر متال ها در کدام کد از استاندارد ASME آمده است ؟

۱- ASME VIII DIV1

۲- ASME SEC II PART C

۳- ASME SEC II PART D

۴- ASME SEC V ARTICLE 6


محدوه ضخامت برای تنش گیری متریال Alloy steel چند میلیمتر می باشد ؟

۱- بالای ۱۶

۲- بالای ۱۵

۳- بالای ۲۰

۴-بالای ۳۲


شاخص کیفیت در فیلم های رادیوگرافی کدام یک از موارد زیر است ؟

۱- Sensivity

۲- UG

۳- IQI

۴- Panoramic


حد مجاز Leg جوش چقدر است ؟

۱- ۰.۷ ضخامت یا ۶ میلیمتر

۲- ۰.۶ ضخامت یا ۷ میلیمتر

۳- ۰.۵ ضخامت یا ۸ میلیمتر

۴- هیچ کدام


معنی P-Number کدامیک از موارد زیر است ؟

۱- دسته بندی فیلر متال طبق آنالیز شیمیایی

۲- دسته بندی متریال بر اساس آنالیز شیمیایی و خواص مکانیکی فلز پایه

۳- دسته بندی الکترودها طبق خواص شیمیایی

۴- هیچ کدام


کدام کد از استاندارد ASME مربوط به روش تست های غیرمخرب می باشد ؟

۱- ASME SEC IX

۲- ASME SEC VIII

۳- ASME SEC V

۴- ASME SEC IV


دمای مجاز قطعه برای تست مایعات نافذ کدام است ؟

۱- ۱۰ تا ۵۲ درجه سانتیگراد

۲-  ۶ تا ۵۲ درجه سانتیگراد

۳- ۵ تا ۵۲ درجه سانتیگراد

۴- ۱۰ تا ۴۳ درجه سانتیگراد


دانسیته فیلم های رادیوگرافی برای اشعه گاما و ایکس در استاندارد چقدر است؟

۱- ۱.۸ تا ۴ ، ۲ تا ۴

۲- ۲ تا ۴ ، ۱.۸ تا ۴

۳-  ۲ تا ۴ ، ۱.۵ تا ۴

۴- ۱.۵ تا ۴ ، ۲ تا ۴


T-282 Radiographic Density

T-282.1 Density Limitations. The transmitted film density through the radiographic image of the body of the appropriate hole IQI or adjacent to the designated wire of a wire IQI and the area of interest shall be 1.8 minimum for single film viewing for radiographs made with an X-ray source and 2.0 minimum for radiographs made with a gamma ray source. For com- posite viewing of multiple film exposures, each film of the composite set shall have a minimum density of 1.3. The maximum density shall be 4.0 for either single or composite viewing. A tolerance of 0.05 in density is allowed for variations between densitometer readings.


انجام تست جوش با روش مایعات نافذ


بهمن ماه ۱۴۰۳

پسر قاضی مقیسه در صفحه شخصی خود در فضای مجازی نوشت: حاجی دو بار برای عمل جراحی نیروی خدماتی (قاتل منافق) از همه قضات پول جمع کرده بود. ولی طرف به بهانه عمل رفته بود آموزش ترور.


سخنان آقا زاده : 

کارکنان زیردست خود بودند و برای ارتقای وضعیت شغلی آنها تلاش می‌کردند. همین آقایی که ایشان را ترور کرد، به مدت ۶ ماه حاج آقا در پی این بود که حقوقش را افزایش دهند. او دائماً پیگیری می‌کرد تا برایش کار‌های بهتری پیدا کند و می‌گفت حیف است که او این‌گونه زندگی کند. باید مقامش بالا برود و مملکتمان به گونه‌ای باشد که تحصیل‌کرده‌ها بتوانند در جایگاه‌های بالاتری فعالیت کنند.»

گفتنی است درباره هویت ضارب نیز پیش‌تر اطلاعاتی منتشر شده است. نام او فرشاد اسدی و متولد ۱۳۶۵ است. او در چند سال اخیر به‌عنوان نیروی خدماتی و آبدارچی و به‌صورت قراردادی در ساختمان دادگستری کل کشور مشغول به‌کار شده بود.


آخه لیسانس برای خدمات و نظافت توالت میگیرن !!!! چرا پیمانکاری و نیرو رسان یا manpower برای یک جای مهم!!!


۱ روز پیش · ضارب پس از هدف قرار دادن قضات و مأمور محافظ، بلافاصله با همان اسلحه از شعبه خارج شده و به طبقه سوم فرار کرده و آنجا با شلیک یک گلوله به قلبش ...


یک ماده نافذ خوب که میتواند عملکرد خوبی در شناسایی نواقص داشته باشد، باید دارای ویژگیهای فیزیکی زیر باشد:

کشش سطحی بالا ( جمع شدن مایع روی سطح به شکل ورقهای کشسان).

خاصیت ترکنندگی بالا ( گسترش و پخش شدن مایع روی سطح با زاویه کم).

گرا  روی ( Viscosity ) کم  ( مقاوم به جاری شدن).

خاصیت مویینگی بالا ( نفوذ و جاری شدن در منافذ باریک)

شفافیت رنگ ( رنگ با خاصیت درخشندگی بالا ).

حل کنندگی بالا ( قابلیت حل کردن ناخالصیهای درون نقص).


در بازرسی با مواد نافذ، موارد زیر را همیشه در نظر داشته باشید. 

مواد نافذ سمی و اشتعال زاست. 

مواد نافذ تأثیر نامطلوب روی پوست و چشم دارد. 

نور فرابنفش برای پوست و چشم مضر میباشد. 

محل بازرسی باید دارای تهویه و شیر آب برای شستوشوی چشم و پوست باشد.


-در بازرسی با مواد نافذ نباید سطح نمونه دارای چربی یا هرگونه پوشش یا رنگ باشد.

-روش تمیزکاری باید با توجه به جنس نمونه و با دقت انتخاب شود تا آسیبی به  کارایی قطعه وارد نیاید. 

-در روش ًهای تمیزکاری با آب، نمونه باید حتما به اندازه کافی خشک شود زیرا آب  مانع ورود مواد نافذ به نقص میگردد.


T-642 Surface Preparation

قبل از آزمایش  سطح مورد آزمون و تمام مناطق مجاور به اندازه حداقل یک اینچ باید خشک  و عاری از هر گونه آلودگی مثل رنگ یا پوسته های رنگ یا چربی و ...باشد

b) Prior to each liquid penetrant examination, the surface to be examined and all adjacent areas within at least 1 in. (25 mm) shall be dry and free of all dirt, grease, lint, scale, welding flux, weld spatter, paint, oil, and other extraneous matter that could obscure surface openings or otherwise interfere with the examination.


After the precleaning operation, the drying process is used to assure the evaporation of any water, solvents, or other cleaning agents that might remain in a discontinuity and thereby contaminate the penetrant when it is applied. Typically a 5-minute minimum drying time is required by the procedure.


Common drying methods include:

• Hand wiping with dry cloth or paper towel,

• Compressed air drying,

• Room air drying,

• Warm air drying,

• Oven drying, and

• Recirculating hot air drying.


۱- آماده سازی سطح : 

زدودن هر گونه آلودگی از سطح ( روغن ، گریس ) 

Asme Sec V Article 6

T-643 Drying After Preparation

After cleaning, drying of the surfaces to be examined shall be accomplished by normal evaporation or with forced hot or cold air. A minimum period of time shall be established to ensure that the cleaning solution has evaporated prior to application of the penetrant.


۲- اعمال مایع نافذ : ( Penetrant )

بعد از تمیزکاری و خشک کردن سطح با استفاده از  روش اسپری کردن یا قلمو زدن یا غوطه وری در حمام ماده نافذ


بعد از مرحله تمیزکاری سطحی، باید مایع نافذ را بر روی سطح اعمال نمود که این عمل را با توجه به امکانات و  یا شرایط قطعه میتوان به وسیله ی اسپری کردن، غوطه وری در مخزن مایع نافذ و یا به وسیله ی فرچه رنگ انجام داد. مایع نافذ سطح موردنظر را میپوشاند و بر اثر خاصیت مویینگی، مایع نافوذ به درون ترک ها نفوذ می کند.


۳- زمان وقفه بعد از اعمال مایع نافذ :  معمولاً طبق پیشنهاد تولید کننده است . زمان ها بسته به application ، ماده نافذ مورد استفاده ، شکل متریال مورد بازرسی  و نوع پیوستگی مورد بازرسی متفاوت است .حداقل محدوده  زمان وقفه عموماً از ۵ تا ۶۰ دقیقه است . این زمان وقفه بر اساس تجربه تعیین میشود.

۴-حذف مایع نافذ اضافی : 

بسته به روش ماده نافذ استفاده شده ممکن است تمیزکاری با یک حلال ، شستشوی مستقیم با آب ، یا ابتدا آماده سازی با یک امولسیفایر و  سپس شستشو با آب انجام گیرد.


T-673 Excess Penetrant Removal

مراقبت شود که حذف مواد نافذ از ناپیوستگی به حداقل ب سد

After the specified penetration (dwell) time has elapsed, any penetrant remaining on the surface shall be removed, taking care to minimize removal of penetrant from disconti- nuities.


۵-اعمال آشکار کننده : ( Developer ) 

با اشکال متفاوتی است می تواند با پاشیدن ( dusting )  ( پودر خشک ) ، فرو  بردن ( dipping )  یا اسپری کردن ( آشکار کننده wet )  اعمال گردد.

۶-ظهور نشانه : 


آشکارساز مجاز است برای مدت زمانی کافی روی یک سطح بایستد تا امکان استخراج ماده نافذ محبوس شده را از هرگونه نقص سطحی فراهم کند. مدت زمان حداقل ده دقیقه است البته برای ترک های تنگ و کیپ مدت زمان بیشتری لازم است.

۷-بازرسی : 

بازرسی در نور کافی مناسب برای یافتن نشانه ها ( indications ) ازهر عیبی انجام می پذیرد.

۸-پاکسازی سطح : 

گام آخر در این فرآیند پاکسازی کامل برای زدودن آشکارساز از سطح است.


T-674 Drying After Excess Penetrant Removal

خشک کردن بعد از حذف ماده نافذ اضافی برای تکنیک های  water washabke یا post emulsifying سطوح 

میتوانند با خشک کردن با متریال های تمیز یا چرخش هوا خشک شوند به شرطی که دمای سطح از ۵۲ درجه بالاتر نرود

(a) For the water washable or post-emulsifying tech- nique, the surfaces may be dried by blotting with clean materials or by using circulating air, provided the tempera- ture of the surface is not raised above 125°F (52°C).

(b) For the solvent removable technique, the surfaces may be dried by normal evaporation, blotting,wiping, or forced air.


ماده نافذ مرئی و فلورسنتی


ماده نافذ Visible :

- از رنگ قرمز ( red dye ) تشکیل شده.

- حساسیت کمتری دارند.

- جهت بازرسی احتیاج به محیط تاریک و اشعه فرابنفش دارند.

- کمتر در برابر آلودگی آسیب پذیرند ( Vulnerable )

ماده نافذ فلورسنتی :

- شامل رنگدانه هایی است که زمان تابش به آنها درخشنده و شفاف می شوند.

- حساسیت بیشتری دارند.

- برای انجام بازرسی به محیط تاریک و اشعه فرابنفش نیاز دارند.

- در برابر آلودگی آسیب پذیرند.


مزایا و معایب نسبت به سایر روش های NDT 


مزایا : 

-حساسیت بالا ( ناپیوستگی های کوچک می توانند آشکار شوند ) 

-محدودیت های کم در بازرسی متریال ( فلزی و غیر فلزی ، مغناطیسی و غیر مغناطیسی ، هادی و نارسانا ) 

-بازرسی سریع مناطق و احجام وسیع

-مناسب برای قطعات با اشکال پیچیده.

-نشانه ها مستقیم در سطح قطعه تشکیل میشود و بنابراین با چشم قابل مشاهده خواهند بود.

-قابل حمل هستند ( بواسطه اینکه مواد در قوطی های اسپری موجودند ).

-هزینه ارزان ( مواد و تجهیزات مربوطه گران نیستند).


معایب : 

-فقط عیوب سطحی قابل آشکار هستند.

-فقط متریال ها با سطح غیر متخلخل ( nonporpus ) قابلیت بازرسی دارند.

-تمیزکاری ابتدایی یک اصل است بعلت اینکه آلودگی می تواند باعث پوشیده شدن عیوب شود.

-لکه گیری ( smearing ) فلزات حاصل از ماشینکاری ، سنگ زنی و بلاست شن یا بخار باید حذف شود.

-بازرس باید دسترسی مستقیم به سطح مورد بازرسی داشته باشد.

-چندین عملیات فرآیندی باید انجام و کنترل شوند.

-تمیزکاری قطعات یا متریال های مورد پذیرش باید انجام گردد.

-حمل و نقل شیمیایی و دفع مناسب نیاز دارد.


T-650 TECHNIQUE 

T-651 Techniques

Either a color contrast (visible) penetrant or a fluorescent penetrant shall be used with one of the following three penetrant processes:

(a) water washable

(b) post-emulsifying

(c) solvent removable


Solvent removable penetrants are removed in the following manner:

The surface of the part is first wiped with a clean, lint free, dry cloth or absorbent paper towel to remove as much of the surface penetrant as possible. The remainder of the surface penetrant is then removed by wiping the surface with a lint free cloth or absorbent paper towel that has been dampened with the penetrant remover (solvent). The surface of the part must not be flushed with the remover, and the cloth or paper towel should not be saturated ( smear : کاملاً آعشته شود ) with the remover.

NOTE: It may be necessary to repeat this step in order to adequately remove the surface penetrant.


سطح قطعه و پارچه یا حوله باید تحت نور ( illumination ) مناسب مشاهده شود تا از حذف کافی ماده نافذ سطح اطمینان حاصل شود. برای جلوگیری از برداشتن بیش از حد باید مراقب باشید. پس از ( following ) حذف ماده نافذ سطح ، سطح قطعه باید با آغشتن یا خیساندن با پارچه یا حوله خشک بدون پرز ( lint free )  یا با تبخیر هوا ( air evapouration ) خشک شود.


دمای استاندارد سطح مورد آزمون باید بین ۵ تا ۵۲ درجه باشد در مواردیکه این محدودیت دمایی عملی نیست طبق T-653 عمل گردد.


T-652 Techniques for Standard Temperatures

As a standard technique, the temperature of the penetrant and the surface of the part to be processed shall not be below 40°F (5°C) nor above 125°F (52°C) throughout the examination period. Local heating or cooling is permitted provided the part temperature remains in the range of 40°F to 125°F (5°C to 52°C) during the examination. Where it is not practical to comply with these temperature limitations, other temperatures and times may be used, provided the procedures are qualified as specified in T-653.


T-653 Techniques for Nonstandard Temperatures

When it is not practical to conduct a liquid penetrant examination within the temperature range of 40°F to 125°F (5°C to 52°C), the examination procedure at the proposed lower or higher temperature range requires qualification of the penetrant materials and processing in accordance with Mandatory Appendix III of this Article.


زمان توقف یا Dwell time که بعد از اعمال ماده نافذ یا Penetrant داده میشود به فرم و نوع ناپیوستگی بستگی دارد.


در جدول T-672 حداقل زمان توقف بعد از اعمال مایع نافذ برای متریال های مختلف طبق شکل قطعه  و نوع ناپیوستگی ذکر شده مثلا برای فولاد به شکل casting یا welds و نوع ناپیوستگی ها مثل LOF PROSITY CRACKS این حداقل زمان ۵ دقیقه است.

در تبصره جدول حداقل زمان برای دمای بین ۵ تا ۱۰ درجه دوبرابر چیزی است که در جدول بیان شده .


E1417

7.2 Penetrant Application—Unless otherwise specified, the entire surface of the component shall be covered with pen- etrant. Large components may be examined in sections. Pen- etrant shall be applied by spraying, dipping, brushing, or other method to provide coverage as required. The component, penetrant, and ambient temperatures shall all be in the range from 40 to 125 °F [4 to 52 °C] unless otherwise specified.

7.2.1 Penetrant Dwell Time—The dwell time, unless other- wise specified, shall be a minimum of 10 min. For temperatures between 40 and 50 °F [4.4 and 10 °C], dwell time shall be a minimum of 20 min. It is recommended to rotate or otherwise move components as necessary during dwell to prevent pooling of the penetrant. For dwell times greater than 2 h, the penetrant shall be reapplied as required.


T-673.1 Water-Washable Penetrants.

ماده نافذ قابل شستشو با آب اضافی باید با اسپری کردن آب حذف شود . فشار نباید از ۵۰PSI تجاوز کند و دمای آب نباید از ۴۳ درجه سانتیگراد بالاتر باشد

Excess water- washable penetrant shall be removed with a water spray. The water pressure shall not exceed 50 psi (350 kPa), and the water temperature shall not exceed 110°F (43°C).


7.1 Equipment:

7.1.1 Solvent Removable Visible Dye Penetrant materials consist of:

a) Penetrant. b) Penetrant remover/cleaner. c) Developer. d) Lint free cloth. e) Light meter capable of measuring visible light intensity in lux / foot candles (f.c.). The light meter shall meet the calibration requirement of T-660 of ASME Code Section V

Application of the developer:

a) Apply the non-aqueous wet developer directly to the area being inspected, by spraying from the aerosol container.

b) The non-aqueous developer evaporates rapidly at room temperature and therefore does not require the use of a dryer.

c) Areas being inspected shall be sprayed in such a manner so as to assure complete coverage with a thin, even film of developer.

d) Dipping or flooding parts with non-aqueous developer is prohibited.

e) Developing dwell time shall not be less than 10 min., The maximum permitted developing time is 1 h for nonaqueous developers as stated in accordance with (ASME-V.Article24, SE-165) unless otherwise specified by the client, in a more restrictive manne


Removal Method 

As  mentioned  previously,  penetrant  systems  are  classified  into  four  categories  according to the method used for excess penetrant removal.   ­

Method A: Water­Washable  

­Method B: Post­Emulsifiable, Lipophilic   Method C: Solvent Removable  

­ Method D: Post­Emulsifiable, Hydrophilic  


Method C, Solvent Removable, is used primarily for inspecting small localized areas.   This method requires hand wiping the surface with a cloth moistened with the solvent  remover, and is, therefore, too labor intensive for most production situations.  

Method A, Water­Washable, is the most economical to apply of the different methods  and  it  is  easy  to  use.  Water­washable  or  self­emulsifiable  penetrants  contain  an  emulsifier  as  an  integral  part  of  the  formulation.  The  excess  penetrant  may  be  removed from the object surface with a simple water rinse. 

When removal of the penetrant from the defect due to over­washing of the part is a  concern,  a  post­emulsifiable  penetrant  system  can  be  used.  The  post­emulsifiable  methods  are  generally  only  used  when  very  high  sensitivity  is  needed.  Post­ emulsifiable penetrants require a separate emulsifier to breakdown the penetrant and  make it water washable. The part is usually immersed in the emulsifier but hydrophilic  emulsifiers may also be sprayed on the object. Brushing the emulsifier on to the part is  not  recommended  because  the  bristles  of  the  brush  may  force  emulsifier  into  discontinuities,  causing  the  entrapped  penetrant  to  be  removed.  The  emulsifier is  allowed sufficient time to react with the penetrant on the surface of the part but not  given  time  to  make  its  way  into  defects  to  react  with  the  trapped  penetrant.  Controlling the reaction time is of essential importance when using a post­emulsifiable  system. If the emulsification time is too short, an excessive amount of penetrant will  be left on the surface, leading to high background levels. If the emulsification time is  too long, the  emulsifier will react with the  penetrant  entrapped in  discontinuities,  making it possible to deplete the amount needed to form an indication.  

The hydrophilic post­emulsifiable method (Method D) is gives better sensitivity than  the  lipophilic  post­emulsifiable  method  (Method  B).  The  major  advantage  of  hydrophilic emulsifiers is that they are less sensitive to variation in the contact and  removal time.  


III-610 SCOPE

When a liquid penetrant examination cannot be conducted within the standard temperature range of 40°F to 125°F (5°C to 52°C), the temperature of the examination shall be qualified in accordance with this Appendix.

III-630 MATERIALS

A liquid penetrant comparator block shall be made as follows. The liquid penetrant comparator blocks shall be made of aluminum, ASTM B 209, Type 2024, 3⁄8 in. (9.5 mm) thick, and should have approximate face dimen- sions of 2 in.  3 in. (50 mm  75 mm). At the center of each face, an area approximately 1 in. (25 mm) in diameter shall be marked with a 950°F (510°C) tempera- ture-indicating crayon or paint. The marked area shall be heated with a blowtorch, a Bunsen burner, or similar device to a temperature between 950°F (510°C) and 975°F (524°C).The specimen shall then be immediately quenched in cold water, which produces a network of fine cracks on each face.

The block shall then be dried by heating to approxi- mately 300°F (149°C). After cooling, the block shall be cut in half. One-half of the specimen shall be designated block “A” and the other block “B” for identification in subsequent processing. Figure III-630 illustrates the com- parator blocks “A” and “B.” As an alternate to cutting the block in half to make blocks “A” and “B,” separate blocks 2 in.  3 in. (50 mm  75 mm) can be made using the heating and quenching technique as described above. Two comparator blocks with closely matched crack patterns may be used. The blocks shall be marked “A” and “B.”


-کدام یک از انواع ناپیوستگی های زیر را معمولاً می توان با آزمون مایع نافذ پیدا کرد؟

الف) سرباره داخلی در جوش

ب) سرباره داخلی در ریخته گری

(ج) حساسیت در فولاد زنگ نزن آستنیتی

(د) ترک های خستگی


-کدام یک از عبارات زیر به طور دقیق قابلیت های آزمایش مایع نافذ را توصیف می کند؟

(الف) آزمایش مایع نافذ برای مکان یابی ناپیوستگی های زیرسطحی در یک قطعه آزمایش مفید است.

(ب) آزمایش نفوذ مایع برای مکان یابی ناپیوستگی در مواد متخلخل مفید است

(ج) آزمایش مایع نافذ برای مکان یابی ناپیوستگی هایی که به سطح در مواد غیر متخلخل باز هستند مفید است.

د) هیچ یک از موارد فوق


-کدام یک از روش های زیر مطلوب ترین روش برای  تمیز کاری اولیه یک قطعه آزمایش قبل از آزمایش نافذ است؟

الف) سند بلاست

ب) چربی زدایی با بخار

ج) پارچه سنباده ( Emery cloth )

د) برس سیمی


-کدام یک از فرآیندهای تمیزکاری اولیه زیر توصیه نمی شود؟

(الف) تمیز کردن مواد شوینده ( detergent cleaning)

ب) چربی زدایی با بخار ( vapour degreasing )

ج) شات بلاست

(د) تمیز کردن اولتراسونیک


-برای تمیز کردن اولیه باید از برس سیمی استفاده کرد:

الف) زمانی که گریس و روغن باید حذف شوند

ب) تنها به عنوان آخرین راه حل

ج) زمانی که زنگ زدگی باید از بین برود ( rust)

(د) هنگام سنگ زنی، فرزها باید برداشته شوند.


-مواد نافذ با قابلبت حذف با حلال و مرئی برای:

(الف) بازرسی قطعات با سطوح ناهموار

(ب) بازرسی دسته‌های قطعات کوچک

(ج) بازرسی قطعات در مکان‌های دور ( remote )

(د) بازرسی قطعات دارای سطوح متخلخل بسیار مفید هستند.


-برای نتایج آزمایش کافی، نور سیاه مورد استفاده در آزمون نافذ فلورسنت باید حداقل چه شدت نور سیاهی  در سطح آزمون را فراهم کند؟

(الف)  100 فوت کندل در هر سانتی متر مربع

(ب) 1000 میکرووات بر سانتی متر مربع

(ج) 800 فوت کندل

(د) 35 میکرووات بر سانتی متر مربع


- حداقل زمان گرم کردن برای عملکرد قابل قبول یک نور سیاه قوس بخار جیوه ای  ( mercury vaopour arc black light )  مورد نیاز است؟

(الف) هیچ کدام

ب) 2 دقیقه

ج) 5 دقیقه

د) 10 دقیقه


- کدام یک از مواد نافذ زیر حاوی ماده امولسیون کننده است؟

(الف) قابل پاک شدن با حلال ( Solvent removable )

ب) قابل شستشو با آب ( Water washable )

(ج) امولسیون شونده  ( Post-emulsifiable )

(د) فلورسنت ( Fluorescent )


- کدام یک از مواد نافذ زیر باید قبل از حذف آب با امولسیفایر اعمال شود؟

(الف) پاک کردن با حلال ( Solvent reomvable )

ب) قابل شستشو با آب ( Water washable )

(ج) امولسیون شونده ( Post emulsifiable )

(د) فلورسنت ( Fluorescent )


- وظیفه امولسیفایر چیست؟

(الف) برای حذف ماده نافذ اضافی

(ب) برای ایجاد نشانه ها با یک سیستم نفوذ پذیر پس از امولسیون

(ج) برای کمک به نفوذ با یک سیستم نافذ امولسیون شونده

(د) برای ساختن ماده نافذ قابل شستشو با آب پس از امولسیون سازی


- یک امولسیفایر بر پایه روغن ( Oil based ) نامیده می شود:

الف) آب دوست ( Hydrophilic ) 

(ب) آبگریز ( Hydrophobic )

ج) چربی دوست ( Lipophilic )

(د) فلوروسکوپی ( Fluoroscopic )


- به امولسیفایرهای مبتنی بر آب  ( Water based ) می گویند:

الف) آب دوست ( Hydrophilic )

(ب) آبگریز ( Hydrophobic )

ج) چربی دوست ( Lipophilic )

(د) فلوروسکوپی


- کدام یک از انواع فرآیندهای تمیز کاری مقدماتی زیر ممکن است برای آزمایش مایع نافذ استفاده شود؟

(الف) فقط مسواک زدن سیمی

(ب) فقط مواد شوینده و آب

(ج) فقط چربی زدایی بخار

(د) هر فرآیندی که قطعه را تمیز و خشک می کند، به قطعه آسیب نمی رساند و با مواد نافذ سازگار است.


- نتیجه محتمل حذف ناقص تمام مواد نافذ اضافی از سطح قطعه آزمایش چیست؟

الف) ایجاد نشانه های نادرست ( false indication )

(ب) تشکیل نشانه های مربوطه

ج) اغراق در اندازه نشانه های مربوطه

(د) هیچ یک از موارد فوق


- خطرات مرتبط با استفاده از برس سیمی در هنگام تمیز کاری اولیه چیست؟

(الف) موهای ( bristled ) برس سیمی ممکن است نشانه های نادرستی ایجاد کنند.

(ب) آلاینده های برس سیمی ممکن است باعث تاخیر در ترک هیدروژنی فولادهای پر کربن شود.

(ج) برس سیمی ممکن است به اندازه کافی لکه های (  soil ) ذاتی را حذف نکند

(د) برس سیمی ممکن است  مسدود کند یا روی فلز را لکه دار کند. ( smear  خط انداختن )


- روش ترجیحی برای حذف رنگ قبل از انجام آزمایش نافذ چیست؟

(الف) سندبلاست

ب) حذف کننده های شیمیایی

ج) برس سیمی برقی

(د) شات بلاست 


- چه آماده سازی یا تمیز کردن سطح اضافی باید بر روی یک ریخته گری ( casting )  آلومینیومی ماشینکاری شده یا فرز کاری شده قبل از آزمایش نافذ انجام شود؟

الف) چربی زدایی با بخار ( vapour degreasing ) 

ب) اچ کردن ( Etching ) 

ج) شستشو با مواد شوینده ( Detegent wash )

(د) هیچ کدام


- روش قابل قبول کاربرد مواد نافذ عبارتند از:

الف) اسپری کردن ( Spraying )

(ب) غوطه وری ( Dipping ) 

ج) کشیدن با قلمو ( Brushing )

د) تمام موارد فوق


- دوره زمانی که ماده نافذ در سطح قطعه آزمون باقی می ماند را می گویند:

الف) زمان اقامت ( Dwell time )

ب) زمان خیساندن ( Soaking time ) 

ج) زمان تثبیت ( Fixing Time )

(د) زمان گسترش ( Development )


- حذف مایع نافذ اضافی ( Excess ) یک فرآیند دو مرحله ای با کدام یک از روش های نافذ زیر است؟

الف) قابل شستشو با آب ( Water washable )

(ب) امولسیون پذیر ( Post emulsifiable )

(ج) حلال قابل جابجایی ( Solvent removable )

(د) کاربردهای اکسیژن مایع


یک توسعه دهنده به بیرون آمدن ( bleed out )  نافذ کمک می کند بخاطر  : 

(الف) حذف کافی ماده نافذ اضافی

(ب) ارائه پس زمینه متضاد برای نشانه های رنگ قابل مشاهده

ج) عمل موئینگی ( Capillary )

(د) عملکرد امولسیفایر مناسب


- در فرآیند نافذ پاک کردن با حلال، مازاد نافذ با موارد زیر حذف می شود:

الف) اسپری آب

ب) اسکرابر آبدوست

ج) اسپری حلال

(د) حوله های تمیز بدون پرز که کمی ( slightly )  با حلال مرطوب ( moistened )  شده اند.


- آشکارساز مرطوب مبتنی بر آب اعمال می شود:

(الف) بلافاصله قبل از حذف ماده نافذ اضافی

(ب) بلافاصله پس از حذف ماده نافذ اضافی

ج) پس از یک دوره خشک شدن بعد از حذف ماده نافذ اضافی

(د) برای حداکثر حساسیت نتایج
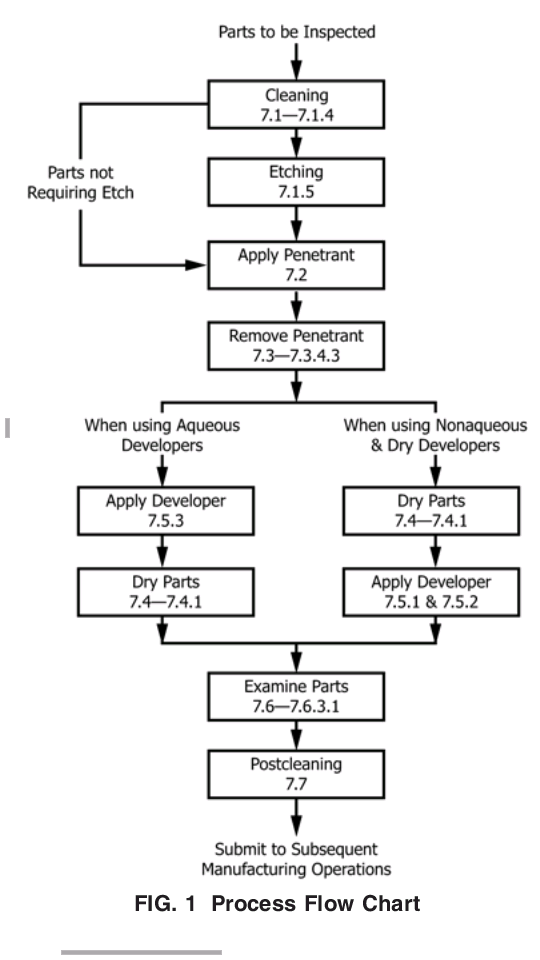


- آشکارساز مرطوب غیر آبی اعمال می شود:

(الف) بلافاصله قبل از حذف ماده نافذ اضافی

(ب) بلافاصله پس از حذف ماده نافذ اضافی

(ج) پس از حذف ماده نافذ اضافی و خشک شدن سطح قطعه

(د) برای حداکثر حساسیت نتایج


- آشکارساز Dry اعمال می شود:

(الف) بلافاصله قبل از حذف ماده نافذ اضافی

(ب) بلافاصله پس از حذف ماده نافذ اضافی

ج) پس از خشک شدن قطعه

(د) برای حداکثر حساسیت نتایج


- اگر ماده نافذ به طور ناخواسته ( inadvertently ) روی قطعه آزمایش خشک شود چه اقدامی لازم است؟

(الف) آزمایش را تکرار کنید، با عملیات  تمیز کاری اولیه شروع کنید

(ب) ماده نافذ را دوباره خیس کنید، زمان ماندن را دوباره شروع کنید و ادامه دهید

(ج) ماده نافذ را از روی سطح پاک کنید و به طور معمول رشد کنید

(د) ماده نافذ را از روی سطح پاک کنید، 5 دقیقه صبر کنید و به طور معمول توسعه یابد.


- حداکثر فشار آبکشی  ( water rinse ) برای حذف ماده نافذ اضافی در فرآیند نافذ قابل شستشو با آب که ایمن در نظر گرفته می شود؟

(الف) تا حد امکان فشار کم، حداکثر 50Psi

(ب) تا 200Psi

(ج) حداکثر PSI

(د) تا 500Psi


- هنگام استفاده از امولسیفایر آبدوست ( Hydrophilic ) ، مقدار ماده نافذ حذف شده بیشتر تحت تأثیر موارد زیر است:

(الف) استحکام محلول و زمان اسپری

(ب) زمان اقامت ماده نافذ ( Dwell time )

(ج) زمان ماندگاری امولسیفایر ( Dwell time )

(د) کفایت تمیزکاری اولیه


- اگر mercury vapour arc black light به طور ناخواسته (inadvertently) خاموش شود، چه مدت ممکن است دوباره راه اندازی شود؟

(الف) بلافاصله

ب) 5 دقیقه

ج) 10 دقیقه

د) 15 دقیقه


- کدام یک از موارد زیر معمولاً به عنوان روشی برای حذف مازاد نافذ هنگام استفاده از فرآیند نافذ قابل حذف با حلال ممنوع است؟

الف) اسپری آب

ب) اسکرابر آبدوست

ج) اسپری حلال

(د) با حوله های تمیز و بدون پرز ( lint free ) مرطوب شده با حلال 


- هنگام انجام آزمون نافذ فلورسنت ، مازاد نافذ معمولاً حذف می شود:

(الف) توسط اسکرابر آبدوست

ب) زیر نور UV

ج) با اسپری حلال

د) با چربی زدایی با بخار ( Vapour degreasing )


- در طول یک آزمون نافذ قابل مرئی و پاک شدن با حلال، حذف کامل ماده نافذ با موارد زیر نشان داده می شود:

(الف) عدم وجود نشانه های قرمز روی سطح قطعه آزمایش

(ب) آب شستشوی تمیز

ج) تکمیل چرخه شستشو

د) عدم وجود رنگ قرمز روی حوله های تمیز کننده


کدام یک از موارد زیر کارکرد یک آشکارساز است ؟

(الف) ارائه پس زمینه متضاد برای مشاهده نشانه ها

ب) قابل شستشو کردن ماده نافذ با آب

(ج) نفوذ ( penetrating into ) به ناپیوستگی های باز به سطح

(د) محلول شدن لکه های ( soil ) های ذاتی ( Organic )  در سطح قطعه آزمون


- کدام یک از موارد زیر عمل یک آشکارسازاست؟

(الف) ارائه پس زمینه متضاد برای مشاهده نشانه ها

(ب) حضور ناپیوستگی ها را با ایجاد یک نشانه نافذ در یک منطقه بزرگتر تشدید می کند.

(ج) مسیرهای موئینگی را برای کمک به فرآیند بیرون کشیدن ( bleed out ) فراهم می کند.

د) تمام موارد فوق


-کدام یک از آشکار های زیر قبل از عملیات خشک کردن استفاده می شود؟

(الف) خشک ( Dry ) 

ب) مرطوب غیر آبی ( Nonaqueous wet )

ج) مرطوب مبتنی بر آب ( Water based wet )

(د) هیچ یک از موارد فوق


- حساس ترین نوع آشکارساز برای تشخیص ناپیوستگی های ظریف عبارتند از:

الف) محلول در آب ( Water soluble )

ب) مرطوب غیر آبی ( Non-aqueous wet )

ج) خشک ( Dry )

د) آب قابل تعلیق ( Water suspendable )


- کدام یک از موارد زیر حساس ترین آشکارساز به ترتیب نزولی ( Descending )  است؟

(الف) خشک، محلول در آب، قابل تعلیق در آب

(ب) مرطوب غیر آبی، محلول در آب، قابل تعلیق در آب، خشک

(ج) غیر آبی مرطوب، خشک، محلول در آب

(د) قابل تعلیق در آب، محلول در آب، مرطوب غیر آبی


- کدام نوع آشکارساز ممکن است بصورت تعلیق یا  حلال باشد؟

(الف) خشک 

ب) مرطوب غیر آبی

ج) مرطوب مبتنی بر آب ( Water based wer )

(د) هیچ یک از موارد فوق


- دمای آبکشی ( Water rinse ) مورد استفاده در فرآیند نافذ قابل شستشو با آب باید:

(الف) 60 تا 110 درجه سانتیگراد

(ب) 40 تا 100 درجه سانتیگراد

(ج) 16 تا 43 درجه سانتی گراد

(د) 70 تا 140 درجه سانتیگراد


- خطر شستشوی بیش از حد در طول آزمون نافذ قابل شستشو با آب این است که:

(الف) ماده نافذ اضافی از قطعه آزمایش حذف خواهد شد.

(ب) نافذ از ناپیوستگی حذف خواهد شد.

(ج) آب هدر رفته ( Waste water ) حاوی غلظت بسیار بالایی از مواد نافذ خواهد بود.

(د) یک پوشش اکسید محافظ روی قطعه آزمون تشکیل شده است


- کدام فرآیند نافذ برای نرخ بالای تولید بسیاری از قطعات کوچک مناسب‌تر است؟

(الف) قابل حذف با حلال

ب) قابل شستشو با آب

(ج) امولسیون پذیر

(د) فلورسنت


- کدام فرآیند نافذ برای تشخیص ناپیوستگی های ظریف حساس تر است؟

(الف) حلال قابل جابجایی

ب) قابل شستشو با آب

(ج) فلورسنت پس از امولسیون

(د) فلورسنت قابل شستشو با آب


- کدام فرآیند نافذ برای کاربردهای قابل حمل در این زمینه مناسب تر است؟

(الف) قابل حذف با حلال ( Solvent removable )

ب) قابل شستشو با آب

(ج) امولسیون پذیر

(د) فلورسنت


- در صورت پیش بینی آزمون های مکرر از کدام فرآیند نافذ باید استفاده کرد؟

(الف) قابل حذف با حلال ( Solvent removable )

ب) قابل شستشو با آب ( Water washable )

(ج) پس امولسیون پذیر ( Post emulsifiable )

(د) فلورسنت ( Fluorescent )


- هنگام آزمایش فولاد ضد زنگ و تیتانیوم، کدام یک از عناصر شیمیایی زیر معمولاً در مواد نافذ مایع باید در حداقل باشد ؟ minimum held

الف) هیدروژن

ب) کلر ( Chlorine )

ج) کربن

د) نفت

هنگام آزمایش آلیاژهای مبتنی بر نیکل، کدام یک از عناصر شیمیایی زیر معمولاً در مادا نافذ باید در حداقل نگاه داشته شود ؟

الف) گوگرد ( Sulphur )

ب) اکسیژن

ج) کربن

د) نیتروژن


گروه هالوژن ها : 

هالوژن (به معنای «نمک‌زا») واژه‌ای یونانی است که از ترکیب hal (به معنای «نمک») و gen (به معنای «تولید کردن») ساخته شده‌است. گروه هالوژن‌ها شامل عناصر گروه ۱۷ (گروه ۷ اصلی) جدول تناوبی است؛ یعنی عنصرهای فلوئور (F)، کلر (Cl)، برم (Br)، ید (I)، آستاتین (At) و تنسین (Ts).
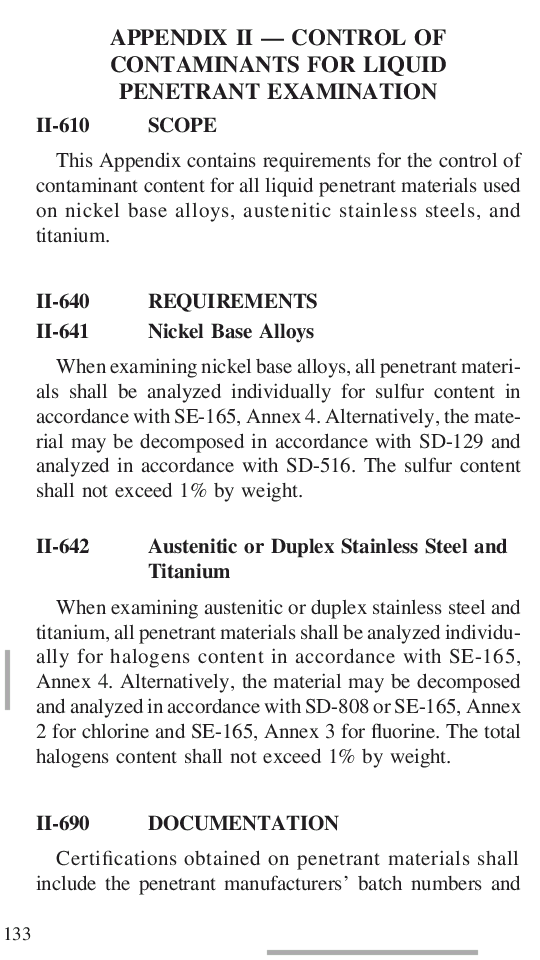


Acceptance criteria_Asme_Viii_Appendix_8


ارزیابی نشانه ها : 


تنها نشانه ها ( indications ) با بعد بزرگتر از ۱.۵ میلیمتر بعنوان Relevant بررسی میشود

الف) نشانه خطی ( Linear ) دارای طول بیش از ۳ برابر عرض

ب) نشانه گرد ( Rounded ) یکی از فرم های گرد یا بیضی با طول کوچکتر مساوی ۳ برابر عرض

ج) هر گونه نشانه شک برانگیز یا قابل سوال باید مجدداً مورد آزمون قرار گیرد برای اینکه مرتبط هستند یا خیر.


استانداردهای پذیرش : 

در موارد زیر قابل قبول نیستند

الف)  نشانه های خطی مرتبط

ب) نشانه های گرد بیش از ۵ میلیمتر ( ۴.۸ البته )

ج) نشانه های گرد مرتبط ۴ یا بیشتر در یک خط بافاصله کوچکترمساوی ۱.۵ میلیمتر


An indication of an imperfection may be larger than the imperfection that causes it; however, the size of the indi- cation is the basis for acceptance evaluation.


(a) Treatment of Indications Believed Nonrelevant. Any indication which is believed to be nonrelevant shall be regarded as an imperfection unless it is shown by reexamination by the same method or by the use of other nondestructive methods and/or by surface conditioning that no unacceptable imperfection is present.


آزمون مناطقی از جوش که عیوب حذف و برداشته شده اند :

بعد از برداشتن عیوب و قبل از انجام جوش تعمیری آن منطقه باید با روش مناسبی آزمون مجدد شود تا اطمینان حاصل شود حذف شده یا به یک سایز مورد قبول کاهش پیدا کرده است.


(b) Examination of Areas From Which Defects Have Been Removed. After a defect is thought to have been re- moved and prior to making weld repairs, the area shall be rexamined by suitable methods to ensure it has been re- moved or reduced to an acceptably sized imperfection.


آزمون مجدد نواحی تعمیر : 

بعد از تعمیر آزمون مجدد mandatory است. اگر عمق تعمیر کمتر از حساسیت فیلم موردنیاز باشد رادیوگرافی می تواند صرفنظر شود.


(c) Reexamination of Repair Areas. After repairs have been made, the repaired area shall be blended into the surrounding surface so as to avoid sharp notches,crevices, or corners and reexamined by the liquid penetrant method and by all other methods of examination that were originally required for the affected area, except that, when the depth of repair is less than the radiographic sensitivity required, reradiography may be omitted.


مزایای اعمال ماده نافذ رنگی ( dye ) روش قابل شستشو با آب 

Penetrant Method A ( Water-Washable )

advantages include:

  • No black light or darkened examination area required;
  • Can be used for detecting a wide range of discontinuities;
  •  Penetrant can be easily removed with water;
  • Adaptable to a large volume of small parts;
  •  Excellent for rough surfaces, keyways. and threads; and
  • Relatively inexpensive.


معایب اعمال ماده نافذ رنگی ( dye ) روش قابل شستشو با آب 

Penetrant Method A ( Water-Washable )

Disadvantages include:

  •  Fine discontinuities may not be detected
  •  Can be affected by acids and chromates,
  •  Not reliable on anodized surfaces,
  • Susceptible to over-washing,
  • Water contamination may destroy usefulness of penetrant, and
  • Wide, shallow discontinuities (width greater than depth) may not be detected.


-Cutting oils may be effectively removed from parts before penetrant testing by:

a. preheating

b. vapor degreasing

c. washing with water 

d. all of the above

-Subsurface discontinuities can be best detected by:

a. the post-emulsification penetrant method

b. the visible dye penetrant method

c. the fluorescent)water-washable penetrant method

d. none of rhe ahove

-The mast common type of contaminant in fluorescent penetrant fluid is:

a. metal filings

b. oil

d. water

c. detergents (from c1eaning)

-Water washable penetrants may be applied by :

a. brushing

b. spraying

c. dipping

d. all of the above

-Ultraviolet light with a proper functioning filter in place. used for fluorescent penetrant inspection can cause permanent damage :

a. human tissues

b. human eyes

c. human blood cells

d. none of the aboye

-the first step in conducting a liquid penetrant test on a surface that has been painted is to:

a. carefully apply the penetrant over the surface

b. completely remove the paint

c. thoroughly wash the surface with a detergent

d. wire brush the surface to roughen the smooth surface coating of paint

-AII of the following basic inspection principIes apply to the visible penetrant methods except : 

a. the penetrant must enter the discontinuity in order to form an indication 

b. indications glow when illuminated with an ultraviolet light

c. a longer penetration time is required for smaller discontinuities

d. if the penetrant is washed out of the discontinuity , an indication will not be formed by that discontinuity

-When using a post-emulsification penetrant, it is necessary to apply the emulsifier : 

a. before applying the penetrant

b. after the water-wash operation

c. after the dwell time has elapsed

d. after the development time  has elapsed

-When conducting a water-washable liquid penetrant test, the wet developer is applied: 

a. immediately after the penetrant has been applied 

b. immediately before the penetrant is applied

c. after removal of the penetrant

d. after removal of the emulsifier

-Usually, the most desirable method of removing excess water-washable penetrant after the dwell time is by using:

a. a low pressure coarse water spray

b. water and brush

c. a solid stream of water 

d. water and clean rags

-The term used to describe the action of a particular developer in soaking up the penetrant in a discontinuity, so as to cause the maximum bleedout of the liquid penetrant for increased contrast and sensitivity, is known as:
a. blotting
b. capillaryaction
c. concentration
d. attraction
-The term used to define the tendency of certain liquids ( تمایل اصلی مایعات)  to penetrate into small openings such as cracks or fissures is:
a. saturation
b. capillary action
c. blotting
d. wetting agent
-When conducting a liquid penetrant test using a post-emulsifiable visible dye penetrant the generally accepted method for applying the wet developer is by:
a. brushing
b. swabbing
c. dipping
d. spraying

-Using an ultraviolet light lamp with a cracked filter or without the filter in place can cause damage to human eyes because the lamp emits:
a. black light
b. ultraviolet light
c. infrared light
d. none of the above
-Which of the following characteristics does not apply to liquid penetrant testing?
a. this method can accurately measure the depth of a crack or discontinuity
b. this method can be used for on-site testing of large parts
c. this method can be used to find shallow surface discontinuities
d. this method can be made more or less sensitive by using different penetrant materials

-The term used to define the period of time in which the test part is covered with penetrant is:
a. waiting time
b. soak time (drain time)
c. penetration time (dwell time)
d. bleed in time
-Which of the following discontinuities is most likely to be missed due to improper rinse techniques?
a. a forging lap
b. deep pitting
c. shallow and broad discontiouities
d. the rinse technique will not affect the detection of discontinuities

-Which of the following surface conditioos could have a detrimental (harmful ) effct on a liquid penetrant test?

a. a wet surface

b. a rough weld

c. an oily surface

d. all of the above

-Excess penetrant (all penetrant except that which is in discontinuities) is removed from the specimen:

a. after the required penetrant dwell time has elapsed

b. before the application of an emulsifier if a post-emulsifier penetrant is used

c. by means of a steam cleaner

d. only when water-washable penetrants are used

-Liquid penetrant testing is capable of detecting:

a. subsurface intergranular stress corrosion cracking discontinuities

b. discontinuities open to the surface

c. subsurface discontinuities

d. lack of fusion (subsurface)

-Ultraviolet Iight equipment is required when penetrant testing by:

a. the fluorescent penetrant method

b. the visible dye penetrant method

c. the nonfluorescent penetrant method

d. all of the above

-When using a post-emulsifiable penetrant. the emulsifier time should be:

a. as long as the penetrant dwell time

b. half the penetrant dwell time

c. the same as the developer time

d. only as long as necessary to remove the interfering background

-When an inspector is working in a darkened area, he/she should become adjusted to the dark before inspecting parts. The generally accepted minimum time period for becoming accustomed ( خو گرفتن ) to the dark is:

a. 1 min to 5 min

b. 5 min to 10 min

c. 10 min to 15 min

d. no waiting period is necessary

-Liquid penetrant inspection cannot find:

a. surface porosity

b. surface cracks

c. an internal cavity

d. a surface forging lap

-AII of the following materials ean be tested by the usualliquid penetrant tests except:

a. unglazed porous  متخلخل ) ceramic

b. titanium

e. high alloy steel

d. cast iron

-Liquid penetrant testing can be used to detect:

a. diseontinuities 1.6 mm (0.06 in.) below the surface

b. internal discontinuities

c. discontinuities open to the surface

d. all discontinuities

-Which of the following are commonly accepted methods for applying penetrant?

a. dipping the part in penetrant (dipping)

b. pouring the penetrant ayer the test specimen (flowing)

c. spraying the penetrant on the test specimen (spraying)

d. all of the above

-A solvent used to clean the surface of a test specimen must possess all of the following characteristics except that the:

3. cleaner must be capable of dissolving oils and greases commonly found on  the surface

b. cleaner must not be flammable

c. cleaner must be free of excessive contaminants

d. cleaner must leave a minimal residue ( deposit )  on the surface

-Which of the statements below best states the danger of sandblasting (without subsequent chemical etching) for cleaning surfaces to be penetrant tested?

a. the discontinuities may be peened over and closed

b. oil contaminants might be sealed in the discontinuities

c. The sand used in the sandblasting operatian may be forced into the discontinuity

d. the sandblasting operation may introduce discontinuities

-The penetrant applied to the surface of a test specimen:

a. seeps into discontinuities

b. is absorbed by discontinuities

c. is drawn into discontinuities by capillary action

d. is drawn into discontinuities by gravity

-Which of the following statements concerning liquid penetrant testing is correct?

a. fluorescent penetrants will produce red against white discontilluity indications
b. nonfluorescent penetrants require the use of ultraviolet lights
c. fluorescent indications will be seen when exposed to ultraviolet light
d. nonfluorescent discontinuities glow in the dark for easy viewing and interpretation

-When removing excess penetrant from the surface of a test specimen:
a. the penetrant removal operation must not remove the penetrant from discontinuities
b. sufficient excess penetrant must be removed to eliminate an interfering background
c. the use of a solvent-dampened cloth is a common method of penetrant removal
d. all of the above
-Which of the following is an advantage of visible dye penetrants over fluorescent penetrants?
a. visible dye penetrants do not require ultraviolet light
b. visible dye penetrants are more sensitive than fluorescent penetrants
c. visible dye penetrants are superior in penetrating characteristics
d. visible dye penetrants are not taxicwhile fluorescent penetrants are taxic

40. The most widely  ( رایج ترین ) accepted method for removing excessive water-washable penetrant from the surface of a test specimen is by:

a. using a wet rag

b. using a water spray rinse

c. washing the part directly under water running from a tap

d. immersing the part in water

The final inspection of a test specimen for discontinuities should take place:

a. immediately after the developer has been applied

b. any time after the developer has been applied

c. after the developer has been on the test specimen for the proper development time

d. Immediately after the rinse operation

-Which of the following is the most  commonly used method for rermoving nonwater-washable visible dye penetrant from the surface of a test specimen?

a. dipping in a solvent

b. spraying

c. hand wiping

d. blowing

The terms dry. aqueous wet and nonaqueous wet are used to describe three different types of:

a. emulsifiers

b. cleaners

c. developers

d. penetrants

-Which of the following is not a generally accepted method for applying penetrants?

a. rubbing the penetrant over the surface

b. brushing the penetrant on the part

c. spraying the penetrant on the part

d. dipping the part in the penetrant

-Which of the following is an acceptable method for applying wet developers?

a. application with a soft brush

b. application with a hand powder bulb

c. rubbing with a saturated doth

d. spraying or dipping

-When using solvent removable penetrants, the excess penetrant may be removed by:

a. dipping the part in solvent

b. spraying the part with water and a solvent

c. rubbing the part with a wet rag

d. wiping the part with a rag (کهنه ) or cloth that has been lightly moistened ( نمدارکردن ) with solvent

-While conducting (اجرای ) a penetrant test, all of the following health precautions should be applied except:

a. washing any excess penetrant from skin using gasoline

b. washing any penetrant from skin with soap and water as soon as possible

c. keeping penetrant off clothes

d. keeping the work area clean

-Which of the following surface contaminants cannot be removed by cleaning parts in a vapor degreaser?

a. grease

b. rust ( زنگ )

c. heavy oil

d. soluble oil

-Before conducting ( اجرای ) a liquid penetrant test, it is important to ensure that the surface of the part is free of:

a. oil or grease

b. acids or chromates

c. traces of water

d. all of the above

-When performing a penetrant test using a post-emulsification penetrant, which of the following is the most critical with respect to proper timing?

a. dwell time

b. developing time

c. emulsification time

d. drying time

-Which of the following is the most likely result of an excessive emulsification time when penetrant testing with post- emulsification penetrants?

a. a large number of nonrelevant indications could appear on the part

b. shallow discontinuity indications could be lost

c. excess penetrant could remain after the wash operation

d. the emulsifier could harden, preventing the developer from blotting the penetrant in discontinuities

-In penetrant testing, developers should be able to perform all of the following functions except:

a. blotting penetrant from discontinuities

b. aiding in providing an image of a discontinuity

c. adding fluorescence to penetrants

d. helping control bleedout

-Which of the fol!owing is the primary limitatian of liquid penetrant testing?

a. penetrant testing cannot Iacate ( مکان یابی ) subsurface discontinuities

b. penetrant testing cannot Iocate shallow ( کم عمق )  surface discontinuities

c. penetrant testing cannot be used on nonmetallic surfaces

d. penetrant testing cannot be used on ferromagnetic material

-In penetrant testing, the time period from developer application to inspection is often referred to as the:

a. emulsification time

b. development time

c. dwell time

d. none of the above

-Liquid penetrant testing is a nondestructive test that can be used for:

a. locating and evaluating all types of discontinuities in a test specimen

b. locating and determining the length, width, and depth of discontinuities in a test specimen

c. determining the tensile strength of a test specimen

d. locating discontinuities open to the surface

-When conducting ( زمان اجرای ) a penetrant test using ( با استفاده از ) fluorescent penetrant, ultraviolet light equipment is required to:

a. cause the penetrant to fluoresce

b. aid the normal capillary action characteristics of a penetrant

c. neutralize excess penetrant on the surface

d. decrease the surface tension of the part

-Which of the following is a type of developer used in penetrant inspection?

a. dry

b. aqueous particulate

c. nonaqueous particulate

d. all of the above

-When penetrant testing parts, the temperature of the parts should be near room temperature. If the part is at a low temperature when tested, the:

a. penetrant may become viscous ( چسبناک )

b. penetrant may evaporate very rapidly

c. color intensity of the penetrant will decrease

d. penetrant will tend to adhere to the surface of rhe part

-If a part to be penetrant tested is hot, the penetrant:

a. may become viscous

b. may reduce sensitivity to small defects

c. may lose some of its color brilliance

d. may evaporate

-Penetrants may be classified or subdivided by the method used to remove excess penetrant. Which of the following is a proper classification in accordance with this statement?

a. nonsolvent removable

b. vapor degreased

c. water-washable

d. brush removable

-AII of the following methods are recornmended to remove grease from the surface of a penetrant test specimen except:

a. vapor degreasing

b. alkaline c1eaning

c. cleaning with salvent type material

d. hot water rinsing

-Which of the following is a possible cause for false penetrant indications?

a. excessive washing

b. inadequate application of developers

c. penetrant or part too cold during penetratian time

d. Lint or dirt  ( پرز یا کثیفی )

-Developer assists in the detection of the visible dye penetrant test indications by:

a. providing a clean surface

b. providing a contrasting background

c. providing a dry surface

d. emulsifying the penetrant bleedout

-When using post-emulsification penetrants, difficulties incurred during the washing operation can be overcome by:

a. reapplying a coating of emulsifier

b. increasing the water pressure used during the washing operation

c. completely reprocessing the part from surface preparation on and by using a longer emulsifier time, if allowed

d. dipping the part in boiling water

-When conducting a penetrant test, spherical indications on the surface of a part could be indicative of:

a. fatigue cracks

b. porosity

c.Weld laps

d. hot tears

-Penetrant developer is commonly available in all of the following forms except:

a. dry developer

b. nonaqueous developer

c. wet developer

d. high viscosity developer

-The penetrant indication of a forging lap will normally be a:

a. round or nearly round indication

b. cluster of indications

c. continuous line

d. dotted line

-The penetrant indication for a cold shut on the surface of a casting will be a:

a. dotted or smooth continuous line

b. cluster of small indications

c. rough deep indication

d. large bulbous indication

-Which of the following methods for applying nonaqueous developer is normally considered the most effective?

a. spraying

b. swabbing

c. brushing

d. dipping

-Of the methods listed below, the most effective means of precleaning a test item to remove organic contaminants such as grease prior to a penetrant test is:

a. vapor degreasing

b. detergent cleaning

c. hot water rinse

d. solvent wiping

-Fluorescent materials used in fluorescent penetrants respond most actively to radiant energy with a wavelength of approximately:

a. 700 nm

b. 250 kV

e. 365 nm

d. 1 klx (100 fc ) foot candle

-Emulsifier time:

a. is important but not normally critical

b. is the time needed to rinse the emulsifier and excess penetrant from the surface

c. is extremely important and will greatly affect test results

d. should be as long as economically practical

-When performing a liquid penetrant test using solvent removable visible dye penetrant, there are several ways to remove excess penetrant from the surface of the part, Which of the methods listed below is generally regarded as most suitable for giving accurate test results?

a. squirting salvent ayer the surface with no more than 276 kPa (40 psi) pressure

b. wiping with a soaking wet cloth, then wiping with a dry cloth

c. wiping with a solvent dampened cloth, then wiping with dry cloths

d. wiping with dry paper wipes, then wiping with a solvent dampened cloth, and finally wiping with dry cloth

-Prior to the penetrant testing of a previously machined soft metal part, which of the cleaning methods listed below would best remove any smeared metal that couId mask discontinuities?

a. etehing

b. shot peening

c. alkaline cleaning

d. water cleaning with detergents

-Why is the drying proeess used in penetrant testing?

a. the drying process is used to ensure that all excess penetrant will evaporate

b. the drying process ensures the uniform drying of dry developer applied over a wet emulsifier

c. the drying process reduces penetration time

d. after the application of a wet developer, the drying process aids in securing a uniform developer coating ( پوشش یکنواخت )

-Which of the following variables must be considered to use the time required for an indication to develop as a measure of the extent of the discontinuity?

a. the type of penetrant and sensitivity of technique

b. the type of discontinuity

c. the temperature of the material being tested

d. all of the above

-The function of the emulsifier in the post-emulsification penetrant method is to:

a. more rapidly drive the penetrant into deep, tight cracks

b. react with the surface penetrant to make the penetrant water-washable

c. add fluorescent dye or pigment to the penetrant

d. provide a coating to which dry powderdeveloper can adhere

-When penetrant testing for shallow discontinuities using a post- emulsification penetrant, the emulsification time should be long enough to:

a. mix the emulsifier with the excess surface penetrant only

b. mix the emulsifier with all the penetrant on the surface and in discontinuities

c. mix the emulsifier with penetrant in the discontinuities

d. allow the emulsifier to dry out lo a white powder

-Which of the following statements concerning contaminating materials on the surface of a penetrant test specimen is false?

a. the contaminant may be of a composition that attacks the penetrant and reduces the fluorescence or color of the penetrant

b. the contaminant may reduce or even prevent capillary action by the penetrant

c. the contaminant may retain ( نگه دارد ) the penetrant and thus increase the sensitivity of the inspection

d. the contaminant may completely fill the crack and thus prevent the entry of penetrant

-Which of the following practices should be avoided when performing a penetrant test?

a. applying emulsifier by dipping the part in emulsifier

b. applying developer by spraying the part with developer

c. removal of water-washable penetrant with a water spray

d. applying emulsifier with a brush

-A commonly used method of checking on the overall performance of a liquid penetrant system is by:

a. determining rhe viscosity of the penetrant

b. measuring the wetability of the penetrant

c. comparing sections of artificially ( مصنوعی ) cracked specimens

d. all of the above

-An important difference between nonwater-washable penetrants and water- washable penetrants is that:

a. water-washable penetrants contain an emulsifier while nonwater-washable penetrants do not

b. the viscosity of the to penetrants is different

c. the color of the to penetrants is different

d. nonwater-washable penetrants are more easily removed than water- washable penetrants

-Which of the following is a discontinuity that might be found in rolled bar stock?

a. shrinkage

b. bleedout

c. laps

d. undercut

-Which of the following characteristics are normally considered when selecting the type of penetrant to be used in a penetrant test.

a. removal characteristics of the penetrant

b. sensitivity level

c. the cost of the penetrant

d. all of the above

-Which materials should be avoided in the penetrant system when testing titanium alloys?

a. carbon or oil

b. halogenated solvents

c. emulsifier or oil

d. fluorescent agents

-Which of the following is a discontinuity that might be found in sand castings?

a. incomplete penetration

b. undercut

c. pIpe

d. shrinkage

-Which of the following is a discontinuity that might be found in a welded fabrication?

a. shrinkage

b. center bead crack, cracks in heat- affected zone, or cratercracks

c. seams

d. laps

-Which of the following is a discontinuity that might be found in rolled plate?

a. laminations

b. shrinkage

c. lack of fusion

d. undercut

-Which of the following contaminants could affect the sensitivity of a penetrant?

a. acid

b. water

c. salts

d. all of the above

-Which of the following is an advantage of visible dye penetrants over fluorescent penetrants?

a. small indications are more easily seeo

b. they can be used on anodized and

chromate surfaces

c. they make less background on rough surfaces

d. no special lighting is required

-Which of the following is a discontinuity that might be found in a forging?

a. shrinkage cracks

b. laps

c. cold shuts

d. insufficient penetration

-Which of the following is a discontinuity that might be found in rolled plate stock?

a. inclusions

b. shrinkage cracks

c. forging laps

d. blow holes

-Which of the following is an advantage of fluorescent penetrants over visible type penetrants?

a. the inspection can be carried out in a well lighted area

b. small indications are more easily seen

c. they can be used where contact with water is objectionable

d. they are less sensitive to contamination of discontinuities

-Which of the following is an advantage of visible dye penetrants over fluorescent penetrants?

a. small indications are more easily seen

b. they can be used on anodized and

chromate surfaces

c. they make less background on rough surfaces

d. no special lighting is required

-Which of the following is an advantage of solvent wipe methods over water washing?

a. no special lighting is necessary during inspection

b. they provide a quicker penetration of small openings

c. small indications are more easily seen

d. they can easily be carried out in the field and remote areas

-The tendency of a liquid penetrant to enter a discontinuity is primarily related to the:

a. viscosity of the penetrant

b. capillary forces

c. chemical inertness of the penetrant

d. specific gravity of the penetrant

-The emulsifier is used:

a. to wash the penetrant out of discontinuities

b. to aid in washing off the surface of parts when using either the water or oil soluble penetrants

c. to emulsify the oil soluble penetrant, thereby making it water washable

d. to preclean parts before applying penetrant

-Developer powder should always be:

a. highly Auorescent

b. applied wet

c. colorless

d. evenly applied ( بطور یکنواخت )

-The prime purpose of the ultraviolet light

for fluorescent penetrant inspection is to:  a.magnify indications

b. make the indications visible

c. develop indications

d. speed up inspection

-When improper processing causes inspection difficulties, what should the inspector do?

a. swab parts with a solvent

b. use a correct bleedback procedure

c.erase nonrelevant fluorescence

d. reprocess the part

-Which of the following is most likely to render the post-emulsification test ineffective?

3. the penetrant time is too long

b. the developing time is too long

c. the emulsifying time is too long

d. none of the above

-Dry developer should be applied:

a. so that a heavy coat of developer Covers all surfaces

b. so that a light dusting covers all surfaces to be inspected

c. with a dry paint brush

d. by dipping

-Which factor would apply in determining the dwell time required for the penetrant to be effective?

a. type of discontinuity sought

b. shape of part

c. size of part

d. surface roughness

-The part is an aluminum forging. Description - the indication is sharp, halfmoon shaped, not deep. It is called:

a. a lap

b. center line porosity

c. a heat treat crack

d. a false indication

-The part is a 13 mm (0.5 in.) thick aluminum plate with a V fusian weld. Description - the indicatían appears as a straight lineThe indication is:

a. shrinkage

b. nonrelevant

c. a quench crack

d. lack of fusion

-Shrinkage cracks are usually found in what areas of a casting?

a. thín sections only

b. heavy sections only

c. at abrupt ( ناگهانی ) changes in thickness

d. no longer a problem

-The term nonrelevant indication is used to describe certain types of penetrant testing indications. Which of the following would be a typical nonrelevant indication?

a. indications due to part geometry or part design configurations

b. nonmagnetic indications

c. multiple indications

d. nonlinear indications

-Which of lhe statements below best states the danger of using sandblasting for cleaning surfaces to be penetrant tested?

a. the discontinuities may be closed

b. oil contaminants might be sealed in the discontinuities

c. the sand used in the sandblasting operation may be forced into the discontinuity

d. the sandblasting operation may introduce discontinuities in the part

-A continuous linear indicatian can be caused by which of the following discontinuities?

a. porosity

b. slag inclusions

c. pitting

d. cracks

-Which of the following could be a source of false indications on a test specimen?

a. penetrant on the test table

b. penetrant on the hands of the inspector

c. contamination of dry or wet developer with penetrant

d. all of the above

-A crack type discontinuity will generally appearas:

a. a round indication

b. a continuous line, either straight or jagged

c. a straight, single solid line

d. random round or e10ngated holes

-Which of the following discontinuities would be impossible to detect using a liquid penetrant test?

a. a forging lap

b. a crater crack

c. grinding cracks

d. nonmetallic internal inclusions

-When removing excess post-emulsifiable  penetrant in a production situation involving relatively large irregularly shaped parts, you may use a:

a. coarse spray

b. strong waterblast

c. cornmercial salvent

d. hot water immersion

-The sensitivity of wet developers can be seriously impaired:

a. when the developer temperature is greater than the ambient temperature

b. when the thickness of the coating becomes too heavy

c. if the corrosion inhibitors are added to the developer

d. if the surface of the part is polished

-When is a nonaqueous wet developer generally preferred?

a. when the dryer oven temperature is above 121°C (250°F)

b. when it is essential to use the most sensitive developers

c. when using a fluorescent penetrant on an as-cast surface

d. when using a fluorescent penetrant on a wire brushed weld


Since visible dye penetrants do not require a darkened area for the use of an ultraviolet light, visible systems are more easy to use in the field. Solvent removable penetrants, when properly applied, can have the highest sensitivity and are very convenient to use.  However, they are usually not practical for large area inspection or in high-volume production settings.

Another consideration in the selection of a penetrant system is whether water washable, post-emulsifiable or solvent removable penetrants will be used. Post-emulsifiable systems are designed to reduce the possibility of over-washing, which is one of the factors known to reduce sensitivity . However, these systems add another step, and thus cost, to the inspection process.


1-The pentrants that are used to detect the smallest defects:

a. Should only be used on aerospace parts

b. Will also produce the largest amount of irrelevant indications

cCan only be used on small parts less than 10 inches in surface area

d. Should not be used in the field

2-The total time the penetrant is in contact with the part surface is called the:

a. Penetrant dwell time 

b.Developer time 

c. Emulsifier time 

d.Penetrant evaporation time

3-The advantage that liquid penetrant testing has over an unaided visual inspection is that:

a. The actual size of the discontinuity can be measured 

b. The depth of the defect can be measured 

c. The cause of the impact can be seen

d. It makes defects easier to see for the inspector

4-POD stands for:

a. Product of discontinuities

b. Probability of defects

c. Probability of detection

d. Personnel over distributor

5-Which of the following is a disadvantage of LPI?

a. Only surface breaking flaws can be detected

b. Surface finish and roughness can affect inspection sensitivity

c. Post cleaning is required

d. All of the above

6-Application of the emulsifier should not be performed with a:

aSpray

b.Brush

c. Dip

d.Both A and B

7-It is well recognized that machining, honing, lapping and hand sanding will result:

a. In a better penetrant inspection

b.In a longer dwell time in order to produce adequate penetration of the penetrant

c. Longer dwell times

d. Metal smearing

8-What industry and military specifications control a penetrants?

a. Toxicity

b.Flash point

c.Corrosiveness

d.All of the above

9-Water suspendible developers consist of a group of chemicals that are:

a. Saturated in water and experience a chemical shift allowing it to

fluoresce on the parts surface

b. Only used on rough porous surfaces c. Dissolved in water

d. Insoluble in water but can be suspended in the water after mixing or agitation

10-Penetrants are designed to:

a. Perform equally

Perform the same no matter who manufacturers them Shift in grade and value when the temperature changes Remain fluid so it can be drawn back to the surface of the part

11-Which emulsifier system is oil based?

a. Hydrophilic emulsifier

b. Lipophilic emulsifier

c.Solvent removable emulsifier

d. All of the above have an oil base

12-The steps listed would represent which type of penetrant method? 1. Pre-clean 2. Apply penetrant and allow to dwell. 3. Pre-rinse to remove first layer of penetrant. 4. Apply hydrophilic emulsifier 5. Rinse to remove excess penetrant 6. Dry part 7. Apply developer and allow part to develop 8. Inspect. 

a. Type I method A

b .Type I method B

c.Type I method D

d. Type II method D

13-The threshold of visual acuity for a person with 20/20 vision is about:

a. 0.003 inches

b. 0.03 inches

c. 0.03 mm

d. 0.3cm

14-Post emulsified penetrants:

a. Are most often used in the field

b. Should never be used in the field

c. Require a separate emulsifier to break the penetrant down and make it water washable

d.Require a separate emulsifier to break down the cleaner and make it solvent removable

15-Large defects can be hidden under a paint surface because:

a. The paint will fill in the cracks and change the fluorescence of the penetrant

b. Paint is more elastic than metal and will not fracture  رنگ ،کشسانی بیشتری نسبت به فلز دار و شکسته نخواهد شد 

c. The penetrant will adhere to the paint resulting in maximum fluorescence

d. All of the above apply

16-Surface contaminants can lead to:

a. A shift in the fluorescent wavelength to a lower angstrom level

b. The part needing to be redipped in order to produce good results

c. Higher background fluorescence

d. All of the above

17-Which developer form is used for dry powder developer? 

a. Form a

b. Form b

c. Form c

d. Form d

18-The performance of a penetrant:

a. Will remain consistent as long is it is stored in a temperature range of 50 to 100F

b. Will only degrade of the temperature exceeds 120F

c. Can be affected by contamination and aging

c. Can be adjusted with the dwell time

19-White light intensity at the surface of the part when using a visible dye penetrant should be:

a. A minimum of 50 foot-candles l

b.A maximum of 50 foot-candles

c. A maximum of 100 foot-candles

d. A minimum of 100 foot-candles

20-Which method of penetrant removal is solvent removable?

a. Method A

b. Method B

c. Method C

d. Method D

21-When fluorescent penetrant inspection is performed, the penetrant materials are formulated to glow brightly and to give off light at a wavelength:

a. Close to infrared light

b. Close to the wavelength of x-rays

c.That the eye is most sensitive to under dim lighting conditions

d. In the red spectrum

22-Which type of penetrant is most sensitive?

a. Type I

b. Type II

c. Type III

d. Type IV

23-Which of the following is an advantage to LPI?

a. Large areas can be inspected

b. Parts with complex shapes can be inspected

c. It is portable

d. All of the above is an advantage

24-When removal of penetrant from the defect due to overwashing of the part is a concern, which method would most often be used?

a. Fluorescent water washable method

b. Visible dye solvent removable method

c. Visible dye water washable method

d. Fluorescent post emulsified method

25-Which method of penetrant removal is post emulsified, hydrophilic?

a. Method A

b. Method B

c. Method C

d. Method D

26-Developers come in a variety of forms and can be applied by:

a. Dusting

b. Dipping

c. Spraying

d. All of the above

27-Which penetrant method is easiest to use in the field?

a. Fluorescent, post-emulsifiable

b. Visible dye, water washable

c. Visible dye,solvent removable

d. Fluorescent, water washable

28-The water content of water washable penetrant:s:

a. Should be performed daily

b. Should be performed weekly

c. Should be performed monthly

d. Must be checked regularly

29-A good cleaning procedure will:

a. Remove all contamination from the part and not leave any reside that may interfere with the inspection process

b. Remove a small amount of metal from the surface of the part

c. Should leave the part slightly flourescent in order to identify any discontinuities

d . Should etch the part slightly only if it is made from 4041 aluminum

30-When performing a liquid penetrant test, the surface of the part under inspection should be:

a. Slightly damp

b. Clean and smooth to the touch

c. Free of oil, grease, water and other contaminants

d. All of the above

31-When removing water washable penetrant the maximum water pressure should be:

a. 25 psi

b. 40 psi ????

c. 50 psi

d.70 psi

32-Which emulsifier is most sensitive to contact time when applied to the parts surface?

a. Hydrophilic emulsifier

b. Lipophilic emulsifier

c. Fluorescent emulsifier

d. Visible dye emulsifier

33-If the surface of the part has been machined, sanded or grit blasted:

a. The part may also require etching

b. It can be immersed in penetrant for its entire dwell time

c. It will require a shorter dwell time

d. It will need to be heated in order to open any cracks that have been peened over

34-Water based, water washable penetrant are checked with a:

a. Centrifuge

b. Refractometer

c. Centrifuge scope

d. Crack block

35-Generally, there is no harm in using a longer penetrant dwell time as long as the penetrant:

a. Is not allowed to dry

b. Stays viscous

c. Does not form clumps on the surface of the part

d. Is mixed with emulsifier

36-When the excess penetrant is removed from the surface of the part, a course water spray should be directed at an angle of:

a. 20 degrees

b. 45 degrees

c. 90 degrees

d. It does not matter what angle the spray is applied

37-Minimum penetrant dwell times are usually:

a. 1-5 minutes

b. 1-30 minutes

c. 5-60 minutes

d. 60-100 minutes

38-Penetrant can be applied by:

a. Dipping

b. Brushing

c. Spraying

d. All of the above

39-For UV lights used in LPI, the accepted intensity is _______ microwatts per square centimeter.

a. 100

b. 500

c. 700

d. 1000

40-Most specifications limit water contamination to around:

a. 1 percent

b. 2 percent

c. 5 percent

d. 10 percent

41-Once the surface of the part has been cleaned properly, penetrant can be applied by:

a. Spraying

b. Brushing

c. Dipping

d. All of the above

42-Black lights should:

a. Only be used with a Franklin filter

b. Only be used with Type II penetrants

c. Never be used with a cracked filter

d. Never be used with Knoop filters

43-Which type of penetrant is a visible penetrant?

a. Type I

b. Type II

c. Type III

d. Type IV

44-The total time that the penetrant is in contact with the part surface is called the:

a. Soak time

b. Baking time

c. Dwell time

d. Immersion time

45-Which method is used to primarily to inspect small localized areas?

a. Method A

b. Method B

c. Method C

d. Method D

46-Which method of penetrant removal is water washable?

a. Method A

b. Method B

c. Method C

d. Method D

47-Which method of penetrant removal is post emulsified, lipophilic?

a. Method A ---> Water washable

b. Method B

c. Method C ---> Solvant removable

d. Method D ---> Hydropholic

48-Which of the following will produce higher sensitivity of a penetrant test?

a. Leaving the part immersed in the penetrant for the entire dwell time

b. Leaving the part immersed in the wet developer for the entire developer time

c. Using a nonaqueous wet developer

d. Allowing the specimen to drain-dwell during its dwell time

49-Which level of penetrant is the most sensitive?

a. Level I

b. Level II

c. Level III

d. Level IV

50-When removing excess penetrant with water, the wash time should be:

a. As long as the specifications allow

b. Based on the temperature of the part

c. As long as necessary to decrease the background to an acceptable level

d. Longer if the water temperature increases


Cone


ترک ها ضرب المثلی دارند که : balık baştan kokar یعنی ماهی از سر گندیده میشود. منظور این است که آب از سرچشمه گل آلود میشود، یعنی فساد در خانواده یا سازمان یا هر تشکیلاتی از بالا شروع میشود.


۱ دیماه ۱۴۰۳


هاکان فیدان وزیر خارجه ترکیه در مصاحبه با فرانس ۲۴ در خصوص وضعیت منطقه و احتمال جنگ بین رژیم اسرائیل و ایران گفت: احتمال آن را بسیار بالا می‌دانم

وی در پاسخ به این سوال که آیا احتمال این جنگ را به دلیل ضعیف شدن ایران می‌دانید یا خیر گفت: به هر دلیلی که می‌خواهد باشد. احتمال اتفاق افتادن آن وجود دارد. 

تنها چیزی که می‌دانم این است که ایرانی‌ها خواهان این نیستند. آنها از یک جنگ بزرگ پرهیز می‌کنند. این را از دیدار با دوستان ایرانی‌ام دریافته‌ام.


Arc Angle : 87.31


Arc Angle : 44.65


Arc Angle : 107.38


Arc Angle : 281.11 °


Arc Angle : 334.25 °


sketch_1


EQUAL

lateral_40_deg_6_thk7_11


قضیه تالس 


قضیهٔ تالس: خط BC با خط DE موازی است پس نسبت پاره خط‌های AD به DB برابر است با نسبت پاره خط AE به EC. 


AD / AB = DE / BC

10 / 21 = 10 / x

x = 21


3 / 2x + 3 = 2 / x + 5

2 ( 2x + 3 ) = 3 ( x + 5 )

4x + 6 = 3x + 15

x = 15 - 6 = 9 

3 / 24 = 2 / y

y = 24 × 2 / 8 = 6


تحمیل آتش بس به اسرائیل ، شکست بزرگ اسرائیل و متحدانش

 پایگاه اینترنتی صهیونیستی i24NEWS اعلام کرد: هدف اساسی حماس از توافق آتش بس باقی ماندن در غزه و حفظ تسلط بر این منطقه بود، علاوه بر آنکه


 جزئیاتی از توافق آتش بس بین اسرائیل و حماس | تبادل اسرا طی ۴۲ روز | بازسازی ۳ تا ۵ ساله غزه تحت نظارت مصر، قطر و سازمان ملل


بمباران هوایی و قتل عام مردم غزه تا یکشنبه ی آتش بس همچنان بی وقفه ادامه دارد. ( ۱۹ ژانویه ۲۰۲۵ و ۳۰ دیماه ۱۴۰۳ )


۹ ساعت پیش · به گزارش فارس؛ ضارب آبدارچی دیوان‌عالی کشور بوده که با سلاح کلت به سمت قضات شلیک کرده است و پس از ترور اقدام به خودکشی می‌کند


سریال های تخیلی تاریخی


۳۰ مهر ۱۳۹۱ · - البته بیشتر شخصیت‌های این سریال خیالی هستند و در واقع هر کدام نماد و سنبل طبقه اجتماعی آن زمان هستند و بلانش هم سنبل یک زن ‌مدرن فرانسوی است.


عمل تطبیق جنسیت در ایران چند شرط دارد:
  • سن بالای ۱۸ سال
  • صدور مجوز عمل از دادگاه
  • اثبات طولانی‌ بودن تمایلات جنسی
  • نداشتن اضافه وزن برای مردان
  • تایید اختلال دو جنسیتی توسط حداقل دو روانشناس معتمد
  • زندگی به مدت یک سال در کالبد جنس مخالف
  • آگاهی کامل نسبت به نحوه تغییر جنسیت، عوارض و برگشت‌ناپذیری آن


و از شاهرگ به شما نزدیکتریم


وَلَقَدْ خَلَقْنَا الْإِنْسَانَ وَنَعْلَمُ مَا تُوَسْوِسُ بِهِ نَفْسُهُ وَنَحْنُ أَقْرَبُ إِلَیْهِ مِنْ حَبْلِ الْوَرِیدِ


فشار تست در High Pressure piping فصل IX


سلام بر او؛ روزى که زاده شد و روزى که مى‌میرد و روزى که دیگر بار زنده برانگیخته مى‌شود. ( حضرت عیسی )


for the signs of appearance May your eyes be on Yemen.


دیماه ۱۴۰۳
علی قنبری در گفت‌وگو با خبرگزاری خبرآنلاین درباره پیش‌بینی نرخ تورم و ارز تا پایان سال گفت: «اگر مسئولان چاره‌جویی لازم را نکنند زمینه افزایش نرخ تورم فراهم شده است. اگر اوضاع به همین منوال ادامه یابد تا پایان سال تورم کشور به بیش از ۴۰ درصد هم می‌تواند برسد. در حوزه نرخ دلار اوضاع حتی بدتر است و انتظار می‌رود در صورت ادامه وضع موجود نرخ هر دلار تا پایان سال به ۱۰۰ هزار تومان هم برسد.»


11 بهمن 1403 · محمد فضل هاشمی استاد فلسفه و الهیات در دانشگاه اپسالا می‌گوید قتل سلوان مومیکا در واقع به نحوی اعدام وی بود که بصورت زنده در رسانه‌های


Calculate ASME B31.3 process piping hydrotest and pneumatic leak test pressure and hoop stress check. The test pressure should be 1.5 times the design pressure for hydrotest, or 1.1 times the design pressure for pneumatic test. An allowance should be made for the pipe design temperature.


در سیستم فشاربالا ( فلنج حداقل 2500 پوند ) حداقل فشار تست ۱.۲۵ برابر فشار طراحی است 


K345.4.2 Test Pressure for Components and Welds. Except as provided in para.K345.4.3 , the hydrostatic test pressure at every point in a metallic piping system shall be as follows:

(a) not less than1.25 times the design pressure.

در صورت بیشتر بودن دمای طراحی نسبت به دمای تست حداقل فشار تست در محل اجرا بایستی طبق فرمول 38 محاسبه شود

(b) when the design temperature is greater than the test temperature,the minimum test pressure , at the point under consideration , shall be calculated by eq.(38)

(38)  Ptest=1.25Pdesign × S(test)/S


Stest=allowable stress at test temperature for the prevalent pipe material ; see TableK-1


در مواردیکه Pipe استفاده نشده از جدول K-1 برای گرفتن تنش های مجاز هر جزء غیر از support و bolt می توان استفاده کرد .


c) in those cases where the piping system may not include pipe itself , any other component in the piping system  ,other than pipe-supporting elements and bolting , may be used to determine the ST/S  ratio based on the applicable allowable stresses obtained from TableK-1.
In those cases where the piping system may be made up of equivalent lengths of more than one material , the ST/S ratio shall be based on the minimum calculated ratio of the included materials.


 تهران تجمع اعتراضی گسترده کسبه بازار باغ سپهسالار تهران در اعتراض به گرانی و تورم مغازه‌ها را بسته و تجمع کرده‌اند یکشنبه 9 دی.۱۴۰۳


مغازه‌داران بازار کفاشان تهران در اعتراض به گرانی و تورم دست به تجمع و اعتصاب زدند. اعتراض و اعتصاب گسترده کسبه بازار سپهسالار تهران


جواد امانی رئیس انجمن اسلامی بازار ضمن تکذیب خبرها و ویدئوهای منتشرشده مبنی بر اعتصاب امروز ( ۹ دی ۱۴۰۳ ) بازاریان تهران، اظهار کرد: وقتی من پرس‌وجو کردم، متوجه شدم شاید نهایتا ۱۰، ۱۵ نفر آن هم حدود ۲۰ دقیقه شعارهایی می‌دادند که در این مدت مغازه‌ها هم باز بود و اتفاق خاصی نیفتاد. البته من از محتوای دقیق شعارها اطلاعی ندارم. 

وی در پاسخ به اینکه گفته می‌شود این شعارها در جهت ترغیب بازاریان به بستن مغازه‌ها بوده است، بیان کرد: نمی‌دانم شاید هم همین بوده، اما در هر صورت منجر به اتفاقی نشد. این اتفاق در کوچه «حمام‌چال» در نزدیکی بازار عباس‌آباد رخ داد و اصلا در بخش‌های اصلی بازار نبود. در حالت کلی واقعا اتفاق خاصی نیفتاده است و وضعیت امروز بازار تهران مانند هر روز بود.


می‌خواهمت اگرچه دلم با تو صاف نیست / خانم مژگان عباسلو ( پزشک )

می‌خواهمت اگرچه دلم با تو صاف نیست
بین غریبه‌هاست که هیچ اختلاف نیست

برگرد پیش از آن‌که از این دیرتر شود
این درّه است بین من و تو، شکاف نیست

گنجشک کوچکی که تو سیمرغ خواستی
در مشت توست، آن‌ طرف کوه قاف نیست

تا چشم تو خلاف لبت حرف می‌زند
حظی‌ست در سکوت که در اعتراف نیست

برگرد مثل بارش باران به خانه‌ام
«باران که در لطافت طبعش خلاف نیست»


۱۶ مهر ۱۴۰۳ · قیام یَمانی یا قیام قَحْطانی از نشانه‌های ظهور، به قیام مردی از نسل امام حسین(ع)، از اهالی یمن اشاره دارد که پیش از ظهور امام مهدی(عج) رخ می‌دهد


  • در روایتی از فردی به نام منصور نام برده شده که یاری‌دهنده حضرت مهدی است و ۷۰ هزار نفر حامی دارد.بر پایه روایتی هنگامی که یمانی قیام کند فروختن اسلحه حرام است.
  • درگیری با سفیانی؛ برخی روایات از درگیری میان یمانی و سفیانی خبر می‌دهند؛ برای مثال کسی که چشم سفیانی را درمی‌آورد از صنعا خروج می‌کند،یا اولین کسی که با سفیانی می‌جنگد قحطانی است.روایات درباره نتیجه جنگ یمانی با سفیانی اختلاف دارند؛ برخی از پیروزی و برخی دیگر از شکست یمانی خبر می‌دهند.


سقوط الجولانی : 

 نارضایتی مردم از حکومت اموی، قیام‌های مردمی، نزاع‌های قبیله‌ای، درگیری‌های داخلی و در نتیجه ضعف داخلی، از عوامل اصلی سقوط بنی امیه می‌باشند.


۲۴ ساعت پیش · اسرائیل برای تجزیه سوریه فقط با ایران طرف نیست بلکه کشورهای عربی هم با تجزیه سوریه موافق نیستند و از طرفی مردم خود سوریه هم این‌رو نمی‌خواهند


۲۱ دیماه ۱۴۰۳ به گزارش مشرق، ظریف، معاون رئیس جمهور در توئیتر نوشت: تصاویر تلخ از کالیفرنیا یادآور خانه‌ها، مدارس و بیمارستان‌های ویران شده در غزه است


Severe cyclic condition


Severe cyclic is not a fluid service


305.2.3 Pipe for Severe Cyclic Conditions

(a) Except as limited in (b) through (d) , only the following pipe may be used under severe cyclic conditions:

(1) pipe listed in Table A-1A , where Ec ≥0.90 or

(2) pipe listed in TableA-1B , where Ej ≥0.90

(b) For API5L pipe , only the following materials may be used:


Grade A or B , seamless

Grade A or B , SAW,str.seam, Ej ≥0.95 

Grade X42 , seamless 

Grade X46 , seamless 

Grade X52 , seamless 

Grade X56 , seamless 

Grade X60  ,seamless

(c) For copper pipe  ,only ASTM B42 may be used.

(d) For copper alloy pipe , only ASTM B466 may be used.

(e) For aluminum alloy pipe , only ASTM B210 and B241, both in tempers O and H112 ,may be used.


  • Proprietary “Type C” lap-joint stub-end welding fittings shall not be used under severe cyclic conditions. A flared lap is not permitted under severe cyclic conditions
  • A miter bend to be used under severe cyclic conditions shall be made in accordance with para. 304.2.3 and welded in accordance with para. 311.1, and shall have an angle α (see Figure 304.2.3) ≤ 22.5 deg.
  • Socket welds larger than DN 50 (NPS 2) shall not be used under severe cyclic conditions.
  • Expanded joints shall not be used under severe cyclic conditions.


درصد رادیوگرافی طبق Asm3 B31.3


۱۳ بهمن ۱۴۰۳ ... ظریف برکنار و محاکمه شود. اما در تجمع مشهد، مشخص شد ظریف در یک دادگاه صحرایی محاکمه و به اعدام، حبس و محرومیت از حقوق اجتماعی محکوم شده است.


سازمان رادیو تلویزیون دولتی ترکیه (تی آر تی ) در وب سایت خود درباره راه اندازی شبکه تلویزیونی به زبان فارسی نوشته است که هدف "ارائه محتوای خبری دقیق، جامع و بی‌طرفانه برای بیش از ۱۳۰ میلیون فارسی‌زبان در سراسر جهان" است.  تی آر تی اضافه کرد:  "تی‌آرتی فارسی، به‌عنوان دوازدهمین زبان و نهمین پلتفرم فعالیت‌های بین‌المللی این شبکه است.


ابوالحسن فیروزآبادی، همچنین از منشأ پیام‌رسان‌های داخلی گفت و تاکید کرد همه‌ی آنها حکومتی هستند. او می‌گوید ایتا مربوط به قم و حوزه‌ی علمیه است.


Owner. The owner of a piping installation shall have overall responsibility for compliance with this Code, and for establishing the requirements for design, construction,examination,inspection,and testing that will govern the entire fluid handling or process installation of which the piping is apart.The owner is also responsible for designating pipingin Category D,Category M,High Pressure,and High Purity Fluid Services,and for determining if a specific Quality System is to be employed. [See paras.300(d)(4) through (7) and AppendixQ.] Where applicable,the owner shall considerr equirements imposed by the authority having jurisdiction regarding the piping installation.The owner may designate a repre- sentative to carry out selected responsibilities required by this Code,but the owner retains ultimate responsibility for the actions of the representative.


در این کد حداقل الزامات بیان شده و تعیین درصد NDT به طراحی مهندسی بستگی دارد و توسط Field Engineering مشخص میگردد ( به LineList پروژه مراجعه شود )  ولی قطعاً کمتر از الزامات B31.3 برای پایپینگ کارخانه ها نیست و بستگی به سرویس دارد... برای برنچ و ساکت هایی که قابلیت RT ندارد هم نوع تست مشخص شده ( PT OR MT )


for normal fluid services, RT is 5%.
For severe cyclic conditions, it is 100%
For elevated temperature service there is a requirement for the NDE during the fabrication of the pipes in the mill. 100% RT on longitudinal or spiral welds if base metal is Pno 4 or 5


305.2.4 Elevated Temperature Fluid Service. In Elevated Temperature Fluid Service,all longitudinal or spiral(helicalseam) welds in P-No.4 or P-No.5materials shall be examined by100% radiography or 100% ultrasonic examination.Acceptance criteria are as statedin para.341.3.2 and in Table 341.3.2 ,for Normal Fluid Service,unless otherwise specified.


Table 341.3.2 : 
Acceptance Criteria for Welds — Visual and Radiographic Examination


341.4.1 Examination — Normal Fluid Service.

b)Other examination

1) Notless than 5% of circumferential butt and miter groove welds shall be examined fully by random radiography in accordance with para.344.5 or by random ultrasonic examination in accordance with para 344.6 . When a circumferential weld with an intersecting longitudinal weld(s) is examined, at least the adjacent 38mm(11∕2 in.) of each intersecting weld shall be examined


341.4.4 ( Elevated Temp Fluid )

(b) Additional Examination. The examinationrequire- mentsof para.341.4.1(b) applywiththefollowingexcep- tions:(1) 1) Fabrication for longitudinal and spiral(helical seam) welds inP-No.4 and P-No.5 materials,except those in components made in accordance with a listed specification,shall be examined by

100%radiography in accordance with para.344.5,orby100% ultrasonic examination in accordance with para.344.6


2) Socket welds and branch connection welds in P- No.4 and P-No.5 materials that are not radiographed or ultrasonically examined shall be examined by magnetic particle orliquid penetrant methods in accordance with para.344.3 or 344.4.


341.4.3 Severe cyclic conditions

b) OtherExamination. All circumferential butt and miter groove welds and all fabricated branch connection welds comparable to those shown in Figure328.5.4E shall be examined by100% radiography in accordancewith para.344.5 ,or ( if specified in the engineeringvdesign) by100% ultrasonic examination in accordance with para.344.6. Socket welds and branch connection welds that are not radiographed shall be examined by magnetic particle or liquid penetrant methods in accordance with para.344.3 or 344.4.


306.1.4 Fittings for Severe Cyclic Conditions

(a) Only the following fittings may be used under severecyclicconditions:

(1) forged.

(2) wrought,seamless orwelded.If welded,requires 100% radiograph of welds in accordance with para.344.5.1 and Table341.3.2.

(3) cast,with factor Ec ≥0.90.7

b) Fittings conforming to MSSSP-43,MSSSP-119,and proprietary “TypeC” lap-joint stub-end welding fittings shall not be used under severe cyclic conditions.


room temperature : temperature between10°C and 38°C (50°Fand100°F).

sealweld : a weld intended primarily to provide joint tightness against leakage in metallic piping.

fillet weld : the leg lengths(the leg length for equal leg welds) of the sides,adjoining the members welded,of the largest triangle that can be inscribed within the weld cross section.For welds between perpendicular members, the definitions in Figure 328.5.2A apply.

NOTE:When the angle between members exceeds105 deg,size is of less significance than effective throat (see also throat of a fillet weld).

(b) groove weld: the joint penetration (depth of bevel plus the root penetration when specified).The size of a groove weld and its effective throat are the same.

(a) theoretical throat: the perpendicular distance from the hypotenuse of the largest right triangle that can be inscribed in the weld cross section to the root of the joint

(b) actual throat: the shortest distance from the root of a fillet weld to its face

(c)effective throat: the minimum distance,minus any reinforcement (convexity),between the weld root and the face of a fillet weld.


طبق تعریف های B31.3 چه سرویس هایی در طبقه بندی D قرار خواهند گرفت ؟

-به بافت بدن آسیب نرساند،غیرسمی و غیراشتعال باشد.

- فشار طراحی  از حدود ۱۰ باز تجاوز ننماید.

- دمای طراحی بین ۲۹- تا ۱۸۶ درجه سانتیگراد  باشد.


Category D FluidService: a fluid service in which all of the following apply:

(1) the fluid handled is nonflammable,nontoxic,and not damaging to human tissues as definedin para.300.2

(2) the design gage pressure does not exceed 1035 kPa (150psi)

(3) the design temperature is not greater than 186°C (366°F)

(4) the fluid temperature caused by any thing other than atmospheric conditions is not less than−29°C (−20°F)


در مورد Category M بعد از بررسی طراحی پایپینگ ، تجربه ، وضعیت های سرویس و موقعیت ، کارفرما الزامات برای سرویس های نرمالی که استحکام نشتی لازم برای محافظت از پرسنل ندارند را مشخص خواهد کرد .. مثلا سرویس آمین که معمولاً کارفرما به خاطر حساسیت رادیوگرافی جوشکار را ۲۰ درصد انتخاب می کند. ( سرویس هایی که در دسته سرویس نرمال قرار نگیرند )


(b) Category M Fluid Service: a fluid service in which both of the following apply:

(1) the fluid is so highly toxic that a single exposure to a very small quantity of the fluid, caused by leakage,can produce serious irreversible harm to persons on breathing or bodily contact, even when prompt restorative measures are taken

(2) after consideration of piping design , experience, service conditions  ,and location , the owner determines that the requirements for Normal Fluid Service do not sufficiently provide the leak tightness required to protect personnel from exposure


از طریق شماره تلفنهای 00903124633399 و 00903124634422 و همینطور آدرس الکترونیکی (farsi@trt.net.tr) و آدرس پستی: PK333-06443 - Yenişehir - Anykara Turkey میتونید


۳ ساعت پیش · اینم تبریک از طرف ارتش اسرائیل برای شب یلدا #یلدا #شب_یلدا


۷ ساعت پیش · اسرائیل در جستجوی بقایای جاسوسی که ۶۰ سال پیش در سوریه اعدام شد؛ الی کوهن. پس از مدت‌ها فعالیت جاسوسی موفقیت‌آمیز، هویت الی کوهن به تدریج کشف شد


independentpersian ✓

Twitter › indypersian

علی خامنه‌ای، رهبر جمهوری اسلامی، روز یکشنبه دوم دی ماه ۱۴۰۳ در دیدار با جمعی از مداحان به موضوع حمایت احتمالی آمریکا از اعتراضات در ایران واکنش نشان داد. او گفت: «یک عنصر از مسئولین آمریکایی می‌گوید هر کس که در ایران اغتشاش کند، ما کمکش کنیم. احمق‌ها بوی کباب شنیده‌اند.» جمهوری…

Twitter • ۳ ساعت پیش


در سال‌های اخیر کهن‌سالی و پیامدهایش به او توان و اجازهٔ فعالیت نمی‌داد، اما شاید آخرین پیامی که از او در یاد مردم بماند، همانی باشد که دوران اعتراضات «زن زندگی آزادی» با خط خودش نوشت:

«من خواستار حذف تصویرم از پلاکارد تبلیغی در میدان هستم، به‌خصوص در زمانی که بغض در گلو داریم و سوگوار فرزندان این آب‌وخاک هستیم.»

پیامش واکنش به دیوارنگاره‌ای بود که سازمان اوج  تحت عنوان «زنان سرزمین من، ایران» در میدان ولیعصر تهران نصب کرد و تصویر ژاله علو هم یکی از آن‌ها بود.


ثبت ۳ پروژه اول برای همه کاربران رایگان است. از پروژه ۴ ام به شرطی که یک سوم پروژه‌های قبلی موفق باشد ثبت پروژه همچنان رایگان است در غیر اینصورت ۱۰,۰۰۰ تومان


۵ دیماه ۱۴۰۳

۵۲ دقیقه پیش · هزاران نفر در شهر‌های لاذقیه، طرطوس، حمص و حماه در اعتراض به آتش زدن یک زیارتگاه علویان (مزار شیخ ابی عبدالله الحسین بن حمدان الخصیبی) در


۲۰ دی ۱۴۰۳  اسرائیل برای تجزیه سوریه فقط با ایران طرف نیست بلکه کشورهای عربی هم با تجزیه سوریه موافق نیستند و از طرفی مردم خود سوریه هم این‌رو نمی‌خواهند


۲۱ دیماه ۱۴۰۳ به گزارش مشرق، ظریف، معاون رئیس جمهور در توئیتر نوشت: تصاویر تلخ از کالیفرنیا یادآور خانه‌ها، مدارس و بیمارستان‌های ویران شده در غزه است


نمیدانی نظر بازی گناهست
ز ما تا قبر چهار انگشت ر اه است
تو می گویی قیامت هم شلوغ است؟
تمام حرف ملاها دروغ است؟
تمام مجتهدها حرف مفتند؟
همه بی غیرت و گردن کلفتند؟
برو یک روز بنشین پای منبر
مسایل بشنو از ملای منبر
شب اول که ماتحتت درآید
به بالینت نکیر و منکر آید
چنان کوبد به مغزت توی مرقد
که ....  به سنگ روی مرقد!


TESTING


موارد مصرف کپسول تامیفلو (تامی فلو) 45 میلی گرم. ضد ویروس(مهارکننده نورآمینیداز ویروس آنفلوآنزا). الف- درمان عفونت حاد انفلوانزای نوع Aو B بدون عارضه


F345 TESTING

F345.2.3 Special Provisions for Testing.

When piping subassemblies are tested  separately,consideration should be given to performing  an additional leaktest of the assembled piping system  prior to initial operation.The test fluid should be  nonhazardous to the process and the  people  performing the examination.Examination for  leaks  should be at all joints that have not been  previously  examined for leaks,or that have been  reassembled  after being examined for  leaks.Examples include  flanges where isolation blanks  were removed  after the leak  test  and joints where in strumentation or  other components were removed for the leaktest.


Y Ducting Connector ventilation


اسلتامیویر

دارو
اُسِلتامیویر با نام تجاری تامیفلو یک داروی آنتی‌ویروس است که فعالیت ویروس آنفلوآنزا را در بدن مسدود می‌کند. این دارو برای درمان آنفلوآنزا در افرادی که به مدت ۲ روز علائم آنفلوآنزا داشته‌اند، استفاده می‌شود. ویکی‌پدیا
جرم مولی: ۳۱۲٫۴ گرم بر مول
تلفظ: ‎/ɒsəlˈtæmɪvɪər/‎
دفع: ادرار (>۹۰% به عنوان اسلتامیویر کربوکسیلات),مدفوع
رده‌بندی داروهای بارداری: AU: B1:


۲ روز پیش · من، پرستو؛ دختری که می‌خواهم برای مردمی که دوستشان دارم بخوانم. این حقی است که نمی‌توانستم از آن چشم بپوشم؛ خواندن برای خاکی که عاشقانه


شابلون برای یک طرف تبدیل مخروطی است که طرف دیگر هم همین است


N=8 : 90/7=12.857


۲۶ آذر ۱۴۰۳  اولین بیانیه بشار اسد بعد از سقوط: تا عصر روز قبل‌ از سقوط دولت در دمشق بودم · سوریه پس از سقوط بشار اسد: برنامه برای انحلال گروه‌های مسلح و لغو


نماینده چین در نشست شورای امنیت پیرامون تحولات دمشق گفت: نگران حملات هوایی اسرائیل به سوریه و گسترش شهرک‌ها در جولان (اشغالی) هستیم. ۱۴۰۳-۰۹-۲۷ ۲۲:۰۷ ...


شما برنده شده اید!

شهروند گرامی؛ تماس های تلفنی و اعلام برنده شدن در قرعه کشی، شگرد کلاهبرداران برای خالی کردن حساب شماست. قرائت کد ارسالی برای افراد دیگر برابر با هک حساب های بانکی تان است. اکیدا از قرائت کدهای دریافتی برای دیگران خودداری نمایید.


موارد مصرف کپسول تامیفلو (تامی فلو) 45 میلی گرم. ضد ویروس(مهارکننده نورآمینیداز ویروس آنفلوآنزا). الف- درمان عفونت حاد انفلوانزای نوع Aو B بدون عارضه


اوسلتامیویر (نام تجاری: تامی فلو) یک داروی ضد ویروس است که از تکثیر ویروس آنفلوانزا در بدن جلوگیری کرده و مانع بروز بیماری و یا کاهش علائم آن شوند. برخی از انواع اوسلتامیویر حاوی موادی هستند که برای افراد حساس به پنی سیلین خطرناک است.


۲۲ دسامبر ۲۰۲۴


همدلی با زنان و مادران جبهه مقاومت

در سالروز ولادت حضرت زهرا(س) و روز مادر و با تقدیم ثواب این جهاد مالی به ایشان، در شروع فصل سرما، در پویش کمک به کودکان و زنان مظلوم فلسطین و لبنان با مردم ایران همراه می‌شویم.

با شماره‌گیری #14* و یا پرداخت از طریق irane-hamdel.khamenei.ir


ایران همدل


independentpersian ✓

Twitter › indypersian

علی خامنه‌ای، رهبر جمهوری اسلامی، روز یکشنبه دوم دی ماه ۱۴۰۳ در دیدار با جمعی از مداحان به موضوع حمایت احتمالی آمریکا از اعتراضات در ایران واکنش نشان داد. او گفت: «یک عنصر از مسئولین آمریکایی می‌گوید هر کس که در ایران اغتشاش کند، ما کمکش می کنیم. احمق‌ها بوی کباب شنیده‌اند.» جمهوری…

Twitter • ۳ ساعت پیش


Lateral Pipe Branch 12 × 4 thk 5.49


سرانجام بشار اسد در ۱۸ آذر ۱۴۰۳ سرنگون گردید


زندان صیدنایا به دلیل شکنجه، تجاوز جنسی و اعدام‌های دسته‌جمعی به عنوان بدنام‌ترین زندان شبکه زندان‌های رژیم اسد شناخته می‌شد. این زندان به نمادی از سرکوب


توضیح دانشگاه خواجه نصیر در خصوص علت درگذشت یک دانشجو


۲۶ آبان ۱۴۰۳ ایلنا :  وزیر کشاورزی فروش نان ۱۰۰ هزار تومانی را تایید کرد و گفت: یکی از نگرانی‌های ما این است که یارانه زیادی به نان داده می‌شود. ( نرخ روز بی پایه ی نان بربری ۶۰۰۰ نان لواش ۷۵۰ نان سنگک ۱۰ تا ۲۰ هزار تومان )


تقی‌زاده ( مشروطه )  بسیار جذب فرهنگ اروپایی شده بود و آن را الگوی مناسبی برای پیشرفت ایرانیان می‌دید و این جمله که: ایران باید ظاهراً و باطناً، جسماً و روحاً فرنگی‌مآب شود و بس، را در مقاله‌ای به‌چاپ رساند.


در زیر اعداد انتقالی به سنترهای لوله ۴ اینچ برای ۱۲ ، ۱۶ و ۳۲ سنتر داده شده ، فایل XDF یکی از آنها نیز لینک داده شده است می توانید برای صحت آنرا تست فرمائید.


dxf format


انشعاب ۹۰ درجه ۴ اینچ با ضخامت ۵.۴۹ میل  از هدر ۱۲ اینچ با داشتن ۵۰ میل آفست سطحی ( خارج از مرکز هدر در سطح ) .  این انشعاب در مرکز قرار نمیگیرد بلکه ۵ سانت به بیرون shift دارد.


sketchtee90offset50mm12x4t5.49


sketchtee90offset28mm10x6t6.02


sketchtee90offset86.5mm16x2t3.91


sketchtee45offset50mm324x104h199n12


قتل متخصص قلب در یاسیج ( ۲۲ آبان ۱۴۰۳ )


کد خبر: ۷۹۷۷۳۳
 

جزئیات قتل مرموز دکتر مسعود داودی در یاسوج

جزئیات قتل مرموز دکتر مسعود داودی در یاسوج
دکتر مسعود داوودی، متخصص مشهور قلب در یاسوج شب گذشته ۲۱ آبان ماه در مسیر منزل خود توسط فردی ناشناس با استفاده از سلاح گرم به قتل رسید اما این حادثه حواشی‌ای داشت که سبب جریحه دار شدن افکار عمومی و مردم شد.
تاریخ انتشار: ۱۰:۱۴ - ۲۲ آبان ۱۴۰۳
 
 پ

مسعود داودی پزشک متخصص قلب و عروق توسط یک فرد شرور در جلوی منزل خود به قتل رسیده است.

به گزارش صداوسیما، در پی قتل دکتر مسعود داوودی، متخصص قلب و عروق دانشگاه علوم پزشکی یاسوج، مرکز روابط عمومی و اطلاع رسانی وزارت بهداشت ضمن تسلیت به خانواده این پزشک متخصص، اعلام کرد که با دستور وزیر بهداشت و همکاری دستگاه قضایی، شناسایی عامل قتل این پزشک متخصص در دستور کار قرار گرفته است.

معاون درمان دانشگاه علوم پزشکی یاسوج در نشست بررسی جزئیات قتل پزشک متخصص قلب در یاسوج گفت: برادر قاتل در سال ۱۴۰۱ به دلیل ابتلا به سکته قلبی در یکی از بیمارستان‌های شهر یاسوج بستری شد که متاسفانه فوت کرد.

تب

مدیر گروه طب اورژانس بیمارستان‌های استان هم با بیان اینکه بیمار به بیمارستان منتقل شد، گفت: پس از ده دقیقه دستور اولیه برای بیمار صادر و پس از انجام نوار قلب و دیگر آزمایش‌ها مشخص شد بیمار دچار سکته شدید است.

طهماسبی با بیان اینکه همه دارو‌های قلبی در مراحل اولیه تزریق شد، افزود: پزشکان طب اورژانس بیمارستان برای ادامه روند درمان این بیمار با پزشک متخصص مشورت کردند.

طهماسبی ادامه داد: پزشک متخصص شیفت دستوری برای تزریق یک نوع آمپول صادر کرد که متاسفانه پرستاران وقت به دلیل تعویض شیفت ادامه درمان را به شیفت بعدی واگذار کردند.

وی افزود: پزشک بعدی برای تزریق این دارو دچار تردید و این شک به همراهان بیمار نیز منتقل و موجب شد که تزریق ۲۰ دقیقه به تعویق بیافتد و منجر به مرگ بیمار شود.


سقوط دانشجو از ساختمان خوابگاه


یک نو دانشجوی دانشگاه خواجه نصیرالدین طوسی به دلیل سقوط از ساختمان یکی از خوابگاه‌های این دانشگاه درگذشت.

به گزارش ایسنا؛ شب گذشته امیرمهدی چگینی، یکی از دانشجویان دانشگاه خواجه نصیرالدین طوسی به دلیل سقوط از طبقه چهارم یکی از ساختمان خوابگاه های این دانشگاه درگذشت.

این دانشجو ورودی ۱۴۰۳ رشته شیمی کاربردی دانشگاه صنعتی خواجه نصیرالدین طوسی بود که از طبقه چهارم خوابگاه «دانش ۱» این دانشگاه به پایین سقوط کرد.

برخی دانشجویان عنوان کردند که این دانشجو به علت نبود آمبولانس در دانشگاه خواجه نصیرالدین طوسی با تاخیر حدود ۲۰ دقیقه ای به یکی از بیمارستان های تهران منتقل شد؛ اما به دلیل خونریزی شدید در این مرکز درگذشت.

متاسفانه برخی دانشجویان هنگام پایین آمدن بجای استفاده از پلکان اقدام به سر خوردن بر روی نرده پلکان می نمایند که با کمال تاسف در مورد ایشان این امر منجر به سقوط به طبقه همکف خوابگاه شده است.


نتیجه گیری : باید حفاظ نصب شود!!!


رقصیدن و احیاناً کشف حجاب در انظارعمومی جرم است !!!

پدر افغانستانی : به این موضوع فکر کردم که اگر یک گوشی ساده داشت و اجازه ورود گوشی را به مدرسه می‌دادند، من می‌توانستم با دختر تماس بگیرم. اجازه نمیدادم چنین اتفاقی بیافتد، حتما راهنمایی‌اش می‌کردم. روز قبل دخترم اردو رفته بود. او در اردو شلوار جین پوشیده بود و توی مسیر رفت هم رقص و شادی می‌کند. گویا مدیر عصبانی می‌شود. فردای آن روز با لباس فرم به مدرسه می‌رود و مدیر داخل کلاس راهش نداد. می‌خواست تنبیه‌اش کند. به من گفتند شلوار جین پایش بود و در اردو میرقصید.»

آیا در مدارس غیر دولتی ( شهریه  بگیر ) چنین اتفاقی می اُفتد؟!!!


پنجشنبه ۹ آذر ۱۴۰۳ در بیانیه‌ای اعلام کرد: سردار سرتیپ دوم پاسدار کیومرث (هاشم) پورهاشمی( معروف به حاج هاشم ) از مدافعان حرم و مستشاران نظامی ارشد سپاه در سوریه در حملات شب گذشته تروریست‌های تکفیری صهیونیستی به حومه حلب به شهادت رسید.


Sabotage


۱۰ آذر ۱۴۰۳


حلب سقوط کرد

بسیاری از تاسیسات مهم نظامی سوریه نیز در حلب قرار دارد. از جمله پایگاه هلی‌بُرد تَفِتناز متعلق به نیروی هوایی سوریه ، پایگاه هوایی الجَراح و پایگاه هوایی نیرب در حوالی شهر حلب واقع شده‌اند.

به گزارش هم میهن آنلاین ، شبه نظامیان تکفیری مخالف حکومت سوریه، وارد حلب شدند.


بر اساس گزارش های رسیده از شهر حلب ، از ساعاتی پیش گروه های تروریستی بدون مقاومت خاصی از طرف ارتش سوریه به شهر استراتژیک حلب رسیده اند و در حال پیشروی به سمت مرکز این شهر هستند.
اگر اتفاق خاصی رخ ندهد، انتظار می رود حلب تا ساعاتی دیگر سقوط کند.


خبر جدید: حلب سقوط کرد

دقایقی قبل، تصاویری از مرکز شهر  حلب منتشر شد  که نشان می دهد معارضان مسلح به مرکز این شهر رسیده اند و در یکی از میدان های منطقه صلاح الدین، جشن پیروزی گرفته اند با این وصف می توان گفت که حلب سقوط کرده و به دست تکفیری ها افتاده است


آزادی تروریست های زندانی


معارضین مسلح بعد از اشغال حلب، به زندان این شهر رفته و تروریست هایی که در بند بودند را آزاد کردند.


وقتی مردم در شبکه های اجتماعی و رسانه های خارجی با چشمان خود می بینند که تروریست ها در جای جای حلب حضور دارند و به جای جنگ، در حال جشن و خوردن شاورما هستند و در همان زمان از صدا و سیما می شنوند که اوضاع در حلب عادی است و تروریست ها بیرون شهر زیر آتش ارتش متوقف شده اند، آیا می توانند به رسانه ای که قرار بود ملی باشد، اعتماد داشته باشند؟!


و این نیز میگذرد باطل ماندنی نیست .


انتشار ویدئویی از یک شهروند با پرچم اسرائیل در میدان آزادی تهران؛⁣ نسخه اصلی این ویدئو با موسیقی متن منتشر شده است.


۲ ساعت پیش · حمص محل پالایشگاه نفتی اصلی سوریه بوده و تصرف آن راه ارتباطی پایتخت به ساحل مدیترانه را قطع خواهد کرد؛ جایی که پایگاه دریایی مهم روسیه در طرطوس


۱۷ آذر ۱۴۰۳ فرار بشار اسد و سقوط دمشق ، نخست وزیر مسئول انتقال دولت به مخالفان و تکفیری ها شد.


۳ ساعت پیش · بغداد الیوم همچنین گفته: «آنچه که تاکنون برای ما تأیید شده، این است که بشار اسد به‌دلیل هدف‌قرارگرفتن هواپیمایش توسط اسرائیل، کشته شده است».


۱۶ ساعت پیش · حسینی، خبرنگار صداوسیما در دمشق گفت: بعضی از فرماندهان بلندپایه بشار اسد اطلاعات دقیقی از اماکن حیاتی ارتش سوریه به رژیم صهیونیستی دادند!


دانه‌ی انجیر معابد فیلم درام دلهره‌آور سیاسی به نویسندگی و کارگردانی محمد رسول‌اف محصول سال ۲۰۲۴ است. داستان فیلم دربارهٔ ایمان، یک قاضی تحقیق در دادگاه انقلاب تهران است که با تشدید اعتراضات سیاسی سراسری و ناپدید شدن اسلحه اش به طرز مرموزی با... ویکی‌پدیا
تاریخ اکران: ۱۸ سپتامبر ۲۰۲۴ (فرانسه)
فیلم‌نامه: محمد رسول‌اف


با توجه به نمای بالا ، وتر H حاصل جذرِ جمعِ مجذورِ ارتفاع  و اختلاف های  ( تفریق و جمع ) X ، D1 ، D2 است


D1=500

D2=150

H=1000

X=350

1015.197 :  وتر H


Elbow Side Joint


ویدیویی از یک مدیر در کارخانه‌ای در فضای مجازی منتشر شده که سراغ کارگرانش می‌رود و به آنها بابت نزدن ریش‌شان هشدار می‌دهد و می‌گوید بابت داشتن حتی ته ریش حقوق‌شان را نمی‌دهد. در توضیحات این ویدیو در فضای مجازی عنوان شده این رفتار تحقیرآمیز با کارگران در یکی از کارخانه‌های معروف بستنی و لبنیات نزدیک رباط کریم و بهارستان انجام شده است. برخی علت این برخورد را مسائل بهداشتی و نیافتادن مو در مواد لبنی عنوان کرده‌اند اما برخی دیگران از کاربران یادآوری کرده‌اند حتی در صورت چنین علتی، برخورد تحقیرآمیز و فیلمبرداری از این رفتار قابل توجیه نیست.


آبانماه ۱۴۰۳


به گزارش ایسنا، «حجت‌الاسلام والمسلمین کاظم صدیقی» در حاشیه مراسم چهلم شهید «سید حسن نصرالله»، سردار «عباس نیلفروشان» و دیگر شهدای مقاومت در مدرسه عالی شهید مطهری در جمع خبرنگاران در ارتباط با پاسخ ایران به تجاوز نظامی رژیم صهیونیستی گفت:  مقام معظم رهبری فرمودند که باید قدرت ملی، نظامی و قدرت اراده جوانان‌مان را به صهیونیست‌ها بفهمانیم.

وی با بیان این که «مقام معظم رهبری حساب شده صحبت می‌کنند»، گفت: مطمئنا و یقینا عملیات وعده صادق ۳ انجام می‌شود و و برای رژیم صهیونیستی پشیمانی از انجام جنایت‌هایش به همراه خواهد داشت.


۶ ساعت پیش · ایران می‌گوید به تلافی حمله اسرائیل، عملیات وعده صادق 3 را علیه اسرائیل «کوبنده‌تر و پیچیده‌تر» انجام خواهد داد و اسرائیل نیز هشدار داده است با


واشنگتن در پیام خود به تهران تاکید کرده است که این بار قادر نخواهد بود تضمین کند که واکنش اسرائیل به حمله ایران «محدودیت» و «دقت» دفعه قبل را داشته باشد. یک مقام سابق اسرائیلی گفته است که تبادل پیام بین آمریکا و ایران در شرایط حساس کنونی از طریق سفارت سوئیس در تهران که به عنوان حافظ منافع ایالات متحده ایفای نقش می‌کند صورت گرفته است. کاخ‌سفید و هیات نمایندگی ایران در سازمان ملل از اظهارنظر در مورد گزارش منتشرشده در مورد هشدار آمریکا به ایران خودداری کرده‌اند


نیمه برهنه شدن دختر علوم و تحقیقات در اواخر آبان ۱۴۰۳


بررسی صورت گرفته نشان می‌دهد خانم آ.د ( آهو دریایی ) دارای بیماری اسکیزوفرنی است، وی ادعا می‌کند که کنترل مغزش دست دیگران است و آنان با ماهواره او را مدیریت می‌کنند.
این خانم به محض ورود به دانشگاه مبادرت به فیلمبرداری از همه لحظات حضورش می‌نماید. وقتی علت فیلمبرداری با موبایل را از او می‌پرسند ، پاسخ می‌شنود که هم‌اکنون در دانشگاه پدر و مادرش حبس شده‌اند.بلافاصله این خانم لباس‌های خود را از تن در می‌آورد و در یک مرحله دیگر نیز کاملا برهنه می‌شود ( کاملاً اشتباهه فقط شورت و کورست به تن دارد ). یاد شده حدود سه ماه است به دلیل اختلافات خانوادگی متارکه می‌نماید وی به دلیل اختلالات روانی و با هدف طی کردن مراحل درمانی در بیمارستان بستری است.


۲۰ آبان ۱۴۰۳


به گزارش فارس، روز گذشته انتشار یک فیلم از یک واحد تولید محصولات لبنی و نحوه برخورد نامتعارف با کارگران مجموعه در فضای مجازی حاشیه‌ساز شد.

سعید دوستی‌نژاد دادستان شهرستان اسلام‌شهر عصر امروز در گفتگو با خبرنگار فارس در اسلامشهر دراین‌خصوص گفت: در پی انتشار ویدئوی از رفتار غیرمتعارف در یک واحد صنعتی تولید محصولات لبنی در اسلام‌شهر، بررسی موضوع در دستور کار قرار گرفت.


هر کاری که در محدوده‌های تاریخی و میراثی انجام شود باید به نظر میراث فرهنگی برسد. اصلا امکان ندارد بدون نظر میراث فرهنگی در یک نقطه میراثی، مدیریت شهری کاری انجام دهد.


ویدئویی در فضای مجازی منتشر شده که فردی در یکی از سالن‌های تولید شرکت میهن با عتاب و خطاب به کارگران از وضع ظاهری محاسن آنان انتقاد و آنان را تهدید می‌کند که حقوق آخر ماه شما منوط به اصلاح وضع ظاهری و محاسن تان خواهد بود. 

روابط عمومی شرکت لبنیاتی میهن با رد این ویدئوی جنجالی اعلام کرد: این ویدئو غیرواقعی است و به صورت صداگذاری شده در فضای مجازی منتشر شده است.


زاویه بین سوراخ های فلنج


360 ÷ Number Of Holes


چهلم  ( ۱۰ آبانماه ۱۴۰۳ )

مجاهدان عرصه اقتصاد کشور روحشان شاد و یادشان گرامی

فوت ( ۵۳ نفر ) : بعلت رعایت نکردن حداقل ها !!! gas detector

۳ ساعت پیش · از بین ۱۶ کارگر مصدوم معدن که به یزد و طبس اعزام شدند، دو نفر همان روز‌های اول و یک‌نفر شنبه همین هفته جانش را از دست داد و آمار فوتی‌های معدن


فرزانه صادق در گفتگوی زنده شبکه خبر ساعت ۱۴:۱۲ دقیقه تازه می پرسیدند مجری خانمه یا آقا ( گفتگو چه ربطی به جنسیت داره دکتر؟!!!) .. اینه وضعیت مملکت !!!


یوم جانگ (هانجا: 閻長, هانگول: 염장) ( گُنگ بُک برده ) یک ژنرال ارتش شیلا بود که بخاطر کشتن جانگ بوگو معروف است. او در نهایت تحت فرمان جانگ بوگو درآمد اما بخاطر دزدی دریایی و تجارت برده توسط جانگ بوگو تنبیه شد و روابط آنها به شدت تیره گشت و داغ بردگی بر پیشانی یوم جانگ زده شد.

یوم جانگ به وسیله جانگ بوگو به جزیره‌ای تبعید شد و دو سال در آنجا به سختی زندگی می‌کرد در نهایت او به طرف کیم یانگ (김양, 金陽, ۸۰۸–۸۵۷) گرایش یافت. کیم یانگ که از به قدرت رسیدن جانگ بوگو ترس داشت یوم جانگ را به کشتن جانگ بوگو ترغیب کرد. اما یوم جانگ علی رغم میل باطنی با جانگ بوگو متحد شد و برای جنگ با کیم‌ یانگ امپراتور شیلا وارد عمل شد و در سال ۶۸۰ میلادی امپراتوری شیلا به کیم‌ ووجینگ داده شد که در نهایت یوم جانگ به رئیس گارد امپراتوری منصوب شد و در سال ۶۸۳ میلادی علی رغم میل باطنی و به دستور کیم یانگ فرمانده جانگ بوگو را کشت.


آبان ۱۴۰۳ دانشگاه آزاد


دختر علوم تحقیقات با نام احتمالی آهو دریایی[۲] دانشجوی دختر دانشگاه آزاد اسلامی واحد علوم و تحقیقات تهران است. موضوع دخالت مأموران حراست دانشگاه در نحوه‌ی پوشش فردیِ وی و اعتراضِ وی به این موضوع، موجب واکنش مردم به این رخداد و موضوع حجاب اجباری در سطح جامعه شد. در تاریخ ۱۲ آبان ۱۴۰۳ در دانشگاه آزاد اسلامی واحد علوم و تحقیقات تهران مأموران حراست و بسیج دانشگاه با زور قصد داشتند این دختر دانشجو را به بهانه حجاب و نداشتن مقنعه به داخل اتاقک حراست ببرند اما با مقاومت و اعتراض او، لباسش (هودی مانند) از تنش کنده شد و زیر هودی چیزی جز لباس زیر بر تن او نبود؛ به همین علت مأموران حراست شوکه شده و رهایش کردند[۳]. پس از این ماجرا و نیمه برهنه شدنِ بالاتنه‌اش در طی درگیری، دختر از فرط عصبانیت شلوارش را هم درآورد و به سمت مأموران پرتاب کرد و نیمه برهنه شد و همین موضوع باعث دستگیری خشونت‌آمیز وی شد.[۴][۵][۶][۷][۸][۹] در جریان دستگیری، این دانشجو مورد ضرب‌وشتم و خون‌ریزی قرار گرفت و به مکانی نامعلوم منتقل شد.[۸][۱۰] مسئولان دانشگاه با تکذیب برخورد فیزیکی با این دانشجو، مدعی اختلال روانی وی شدند.[۱۱]


مشکل شریعتمداریِ کیهان حضور اسرائیل در باکوست 

کیهان نوشت: قرار است بیست و نهمین اجلاس تغییرات اقلیمی سازمان ملل با عنوان «‌کاپ ۲۹» از ۲۱ آبان تا ۲ آذر ماه در باکو، پایتخت جمهوری آذربایجان برپا شود.

برخی از خبرها حکایت از آن دارند که قرار است آقای دکتر پزشکیان، رئیس‌جمهور محترم کشورمان در رأس هیئتی در این اجلاس شرکت کنند! اگر این خبر که غربگرایان داخلی به شدت روی آن اصرار می‌ورزند، صحت داشته باشد، جناب پزشکیان به دام و تله خطرناکی پای نهاده و خسارت‌های سنگینی را به جمهوری اسلامی ایران و شخصیت خود تحمیل خواهند کرد!

«‌اسحاق هرتزوک‌» رئیس‌جمهور رژیم جعلی و جنایتکار اسرائیل هم به این اجلاس دعوت شده و در آن شرکت خواهد کرد!


۷ روز پیش · هرتزوگ در این سفر دو روزه قصد دارد با همتای آذری خود، الهام علی‌اف، دیدار و در یک رویداد ویژه به مناسبت هفتاد و پنجمین سالگرد استقلال رژیم


حسین امیرعبداللهیان، وزیر امور خارجه ایران، سال گذشته، رژیم صهیونیستی را متهم کرد که «حضور خود را در چندین منطقه آذربایجان تثبیت کرده است»، باکو این اتهام را رد می‌کند.


ایران بلافاصله پس از آن، یک رزمایش نظامی در امتداد مرزش با جمهوری آذربایجان برگزار کرد. علی‌اف نیز با عکسی از خود در کنار پهپادهای کامیکازه رژیم صهیونیستی «هاروپ» که در کشورش تولید می شد، پاسخ داد.


پهپاد هاروپ از fa.wikipedia.org
هاروپ (انگلیسی: IAI Harop) یک پهپاد انتحاری ساخت شرکت صنایع هوافضای اسرائیل موسوم به آی‌ای‌آی است، که در زمره مهمات پرواز کننده قرار دارد


۶ ساعت پیش · ایران می‌گوید به تلافی حمله اسرائیل، عملیات وعده صادق 3 را علیه اسرائیل «کوبنده‌تر و پیچیده‌تر» انجام خواهد داد و اسرائیل نیز هشدار داده است با ....


واشنگتن در پیام خود به تهران تاکید کرده است که این بار قادر نخواهد بود تضمین کند که واکنش اسرائیل به حمله ایران «محدودیت» و «دقت» دفعه قبل را داشته باشد. یک مقام سابق اسرائیلی گفته است که تبادل پیام بین آمریکا و ایران در شرایط حساس کنونی از طریق سفارت سوئیس در تهران که به عنوان حافظ منافع ایالات متحده ایفای نقش می‌کند صورت گرفته است. کاخ‌سفید و هیات نمایندگی ایران در سازمان ملل از اظهارنظر در مورد گزارش منتشرشده در مورد هشدار آمریکا به ایران خودداری کرده‌اند.